CDU Coupler Assemblies: Drawing to 20k/Month in 30 Days (2026)
You have a CDU drawing on your desk, a deadline from the integration team, and a supplier who said yes to everything. Then the first leak test fails. The seat looks fine to the eye, but the sealing face is a fraction of a degree off, the bore carries a burr you cannot see, and the batch report tells you nothing about which bar of steel the part came from. In liquid cooling, that is not a cosmetic defect. It is a leak inside a rack nobody wants to open for the next six months.
This guide follows what actually happens between a CDU coupler drawing and a repeatable production rate. We use one anonymous customer program as the thread: a CDU coupler assembly that ramped toward 20,000 units a month inside a 30-day window. We will walk the machining route, the numbers we held, the checks that mattered, and the places where a cheaper quote usually hides a cost you will pay later.
We are LusterControl, the brand of Dongguan Licun Technology Co., Ltd., a source factory in Dongguan with 60 CNC machines, a 4,000 m² plant, and fifteen years of stainless-steel mirror turning behind us. Everything below is written from the shop floor rather than a brochure. Your geometry will differ. The decision framework will not.
Table of Contents
- 1. What CDU Coupler Assemblies Actually Do Inside an AI Cooling Loop
- 2. Why Liquid-Cooling Coupler Machining Is Harder Than It Looks
- 3. The 30-Day Ramp: One CDU Coupler Assembly Program, Step by Step
- 4. Turn-Mill Composite: One Setup, Two Surfaces, One Datum
- 5. CNC Precision Machining: Hitting ±0.005 mm on Seal Interfaces
- 6. Tight Tolerance CNC vs Standard Turning: A Hard-Number Comparison
- 7. Choosing CDU Coupler Assemblies Partners: Five Checks Before Your PO
- 8. Common Mistakes in Liquid-Cooling Coupler Machining (And How We Avoid Them)
- 9. From 20,000/Month to Traceable Batches: CNC Precision Machining Controls
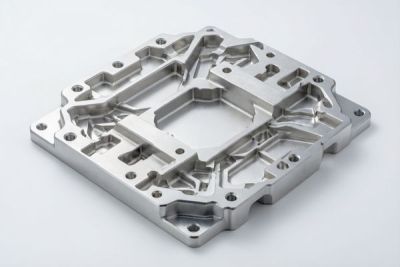
Liquid Cooling (AI Compute) CNC precision component
What CDU Coupler Assemblies Actually Do Inside an AI Cooling Loop
Before you argue about tolerances, get the function right.
- CDU
- Coolant Distribution Unit. The skid that pumps, filters, and distributes water-glycol or dielectric fluid to the cold plates on AI compute trays.
- CDU coupler assembly
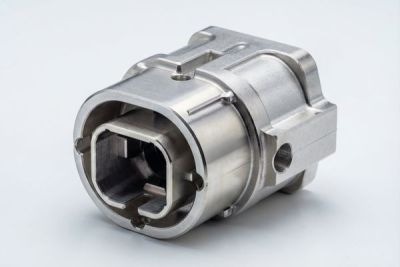
- The interface that connects the CDU manifold to the rack loop: body, seal seat, thread or quick-connect feature, and the mating surface that decides whether the joint holds pressure.
- Seal seat
- The machined face or cone an O-ring, gasket, or metal seal compresses against. On a coupler, this is the surface that sets leak performance, not the outside diameter.
A CDU coupler is a small part with an unforgiving job. It sits at the boundary between a pumped manifold and a rack that runs for thousands of hours. It sees pressure cycling, thermal movement, assembly torque, and occasionally a technician connecting it in a tight space at an awkward angle. If it weeps, you do not just lose fluid. You lose confidence in the whole loop, and you spend engineering hours chasing a leak that looks like a cold-plate problem but started at the fitting.
That is why we start every coupler conversation at the interface rather than the blank. In our technical guides on liquid-cooling and fluid-control components, the recurring theme is the same: the functional surface is usually the last thing a general job shop protects and the first thing you should specify.
Three jobs one coupler has to perform at the same time
- Seal. Hold the fluid at working pressure through temperature swings and vibration without relying on sealant or torque luck.
- Align. Guide the mating half into the seat so the O-ring is not cut on the thread entry and the cone is not scored on the way in.
- Survive. Resist corrosion from the coolant chemistry, survive repeated connect-disconnect cycles, and stay dimensionally stable after passivation.
Why the interface, not the body, decides your yield
Buyers often specify the overall length and thread class carefully and leave the seal seat as a general tolerance. That is backwards. The body can be a few tenths off and still assemble. The seal seat cannot. If the face is out of flatness, if the bore has a directional tool mark that wicks fluid, or if the thread and the seat are cut in two different setups, you get a part that passes a visual check and fails a pressure decay test. We have seen programs where scrap was traced not to the raw material but to the last 0.2 mm of material removed from a sealing face.
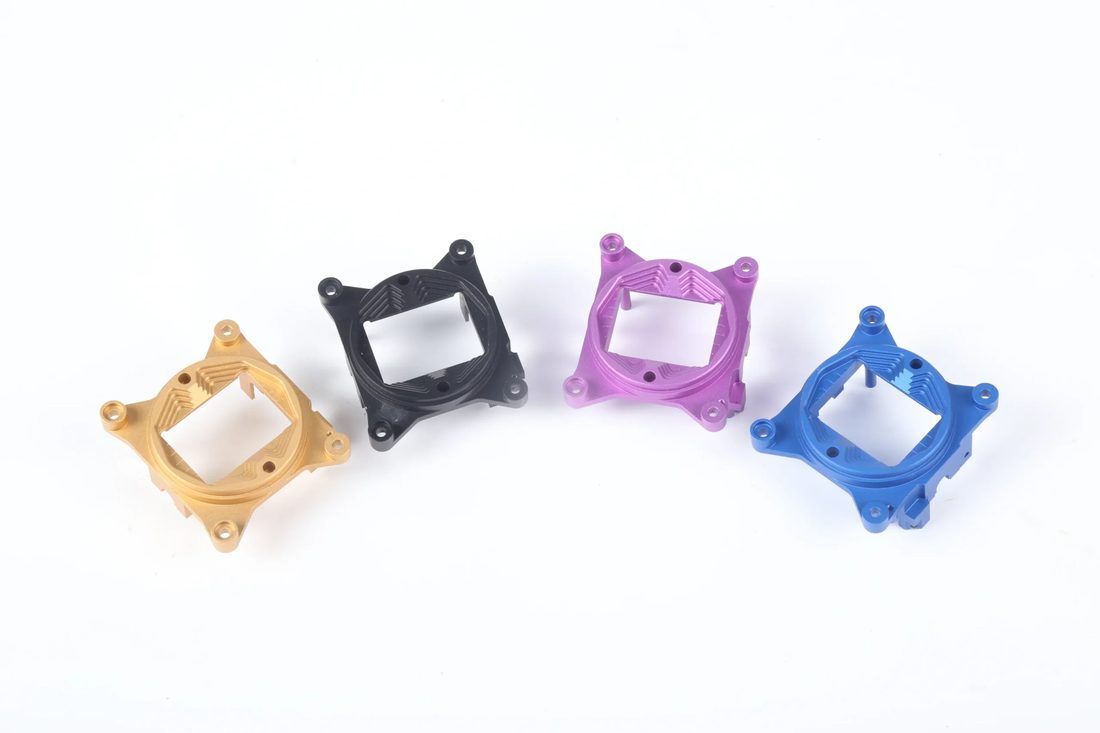
Liquid Cooling (AI Compute) CNC precision component
Why Liquid-Cooling Coupler Machining Is Harder Than It Looks
A coupler is small enough to hold in one hand and precise enough to punish every shortcut.
If you have ever quoted a coupler against a flange or a bracket, you already know the trap. The part looks simple: a turned body, a thread, a bore. The difficulty is not the shape. It is what happens to the shape while you are making it.
Thin walls move when you clamp them
Coupler bodies are often lightened to fit a dense manifold. That leaves a section that deflects under a standard three-jaw chuck. You cut to size, release the part, and the bore goes out of round because the stress you put in with the jaw came back out. The fix is not a softer cutting pass. It is a clamping and sequencing plan that treats the seal seat as a finished surface only after the bulk material has been removed. On the program discussed here, the sealing features were finished in a single clamping after the bulk material was removed.
The burr you cannot see
Cross-drilled ports and internal shoulders produce burrs at the intersection of two holes. A visible burr gets caught in inspection. A hidden one breaks loose during commissioning, travels downstream, and lodges in a micro-channel. For liquid cooling that is a serious failure mode: the coupler is fine, the cold plate is not. We treat cross-hole deburring as a defined operation with its own inspection step, not as a five-second pass with a file at the end of the line.
Surface finish is a sealing spec, not a beauty spec
A sealing face with the wrong texture will leak slowly and inconsistently. Too rough and the O-ring never fully conforms; too polished in the wrong pattern and you lose the lubricant retention the elastomer needs. Our standard mirror finish is Ra ≤ 0.6 µm, and we can take stainless surfaces to 8K mirror at Ra 0.2 µm where the drawing calls for it. On a coupler, the point is not to make the part shiny. It is to make the surface repeatable from the first article to the ten-thousandth.
Where the tolerance actually lives
| Feature | Working target on this class of part | Why it matters to you | How we verify it |
|---|---|---|---|
| Mating diameter | ±0.005 mm capability window | Sets the interference and the seal compression | In-process gauge plus final CMM report |
| Seal seat finish | Ra ≤ 0.6 µm standard; 8K Ra 0.2 µm on request | Controls slow weep and leak repeatability | Surface comparator and profilometer record |
| Port intersection | Defined deburr operation, no loose burr | Prevents debris reaching cold-plate channels | Borescope check on the sample plan |
| Thread to seat relationship | Cut and checked in one setup | Stops the seal face being scored on assembly | Coaxiality checked on the same datum |
| Material identity | Heat lot carried with the batch | Lets you answer a customer audit months later | Incoming batch traceability and certificate |
The 30-Day Ramp: One CDU Coupler Assembly Program, Step by Step
The calendar is the part buyers ask about and suppliers rarely show.
Let us be precise about what a 30-day ramp means, because the phrase gets abused. It does not mean a validated, fully qualified production line in thirty days for every geometry. It means that for this particular anonymous program, drawing review, process planning, sample making, and a controlled ramp toward 20,000 units a month were compressed into a 30-day window with the customer involved at each gate. The geometry was suited to bar-fed turn-mill work. A different part, material, or qualification regime will change the timeline.
Days 1 to 5: Drawing review and DFM
We start by marking the drawing against three questions: which surfaces seal, which surfaces locate, and which surfaces simply need to exist. Then we look for the features that fight each other: a deep bore behind a thin wall, a thread that runs into a seal seat, a finish callout that a turning operation cannot hold without a secondary process. We send back a short DFM note listing what we will hold, what we suggest relaxing, and where we recommend a different datum. This is the cheapest week of the whole program.
Days 6 to 12: Tooling, first articles, and seal validation
Tooling is prepared around the functional surfaces: the seat gets its own finish pass and its own gauge. We run initial articles and report the dimensions that matter, not a decorative inspection sheet. Samples go to the customer for fit and pressure testing. If the first articles come back with a tolerance trend rather than a random scatter, we adjust the process before we make more parts. Trend is information; scatter is a problem.
Days 13 to 30: Process lock and ramp
Once the customer accepts the samples, we lock the process parameters: tooling offsets, clamping approach, inspection frequency, and the batch reporting format. Volume then climbs in controlled steps rather than a single jump. The aim for this program was 20,000 units per month. Across the whole plant we run at roughly 500,000 parts a month, so the coupler program was not stretching our capacity; it was stretching our discipline on documentation and consistency.
- Day 1: drawing and CAD review, functional surfaces flagged.
- Day 3: DFM feedback returned with tolerance and datum recommendations.
- Day 6: tooling and gauging released to the floor.
- Day 9: initial articles machined and dimensionally reported.
- Day 12: customer fit and pressure validation on samples.
- Day 18: first controlled production increment with full batch records.
- Day 30: ramp target of 20,000 units per month reached under the locked process.

Liquid Cooling (AI Compute) CNC precision component
Turn-Mill Composite: One Setup, Two Surfaces, One Datum
The routing choice you make on day one decides how much inspection you need on day thirty.
- Turn-mill composite
- A single machine that performs both turning and milling on the same clamped part. The rotational features and the flats, ports, or cross-holes are produced without moving the workpiece to a second fixture.
Consider what happens when a coupler is turned on one machine and then moved to a mill for the port features. Every transfer introduces a new datum. The inspector now has to prove that the port is positioned relative to the seal seat, which means measuring a relationship that two machines created independently. With turn-mill composite, the relationship is built into one setup. That is not a marketing advantage; it is fewer sources of variation and a shorter inspection report.
Step 1: Bar feed and stress-relieving rough
We start from controlled stainless bar stock, bring the batch identity forward with the job, and rough the bulk profile while leaving material on the functional surfaces. This is where thin-wall distortion is managed. Taking the heavy cuts early means the finishing pass removes very little material and therefore introduces very little new stress.
Step 2: Finish the seal seat, then cut the secondary features
The sealing geometry is finished in the same clamping as the datum it relates to. Ports, flats, and cross-holes follow, with dedicated deburring at each intersection. If the part needs 5-axis access for an angled port, we keep it on the same platform rather than moving it to a separate fixture, because the angular relationship back to the seat is exactly what the customer will measure.
Step 3: Gauge before the part leaves the spindle
In-process gauging catches a drift while there is still time to correct the offset. Waiting until final inspection means you have already made a batch of parts that agree with each other and disagree with the drawing. On the program described here, the mating-feature window was ±0.005 mm, and holding that window over a ramp required checking during the run rather than only at the end.
This is the kind of work our Dongguan plant was built around: 60 CNC machines including turn-mill centres, 5-axis equipment, and Swiss sliding-head lathes, on 4,000 m² of floor after the 2026 expansion. The older 2,000 m² figure you may find elsewhere is no longer current.
| Route | Setups | Datum relationship | Inspection burden | Fit for a 20k/month ramp |
|---|---|---|---|---|
| Turn-mill composite, one clamping | 1 | Built in by the machine | Low: features already related | Strong |
| Turn, then mill on a second fixture | 2 or more | Re-established at transfer | Higher: relationship must be proven | Workable with tight fixturing |
| Manual deburr between operations | Adds handling | No dimensional change, but damage risk | Subjective | Hard to standardise at volume |
Pros
- Choose turn-mill composite if your seal seat and port features have a positional relationship that must be proven.
- Choose it if you are ramping volume and want fewer inspections and fewer handling steps.
- Choose it if your part combines fine turned diameters with cross-holes or flats.
Cons
- Choose separate operations if the geometry is genuinely simple and the volume is very low.
- Choose a simpler route if your budget cannot support setup engineering and you do not need a proven datum chain.
- Be honest if your supplier cannot show turn-mill capability; a claim on a website is not the same as a machine on the floor.
CNC Precision Machining: Hitting ±0.005 mm on Seal Interfaces
A tolerance is only real if it survives the whole batch, the coolant, and the passivation line.
Specifying ±0.005 mm is easy. Holding it is a process question. On seal interfaces the risk is not that one part misses; it is that the process drifts slowly through a shift and the last hundred parts sit at the edge of the window. That is why we treat tolerance as an in-process control, not a final-inspection filter.
Toolpath and tool life are part of the tolerance
A fresh tool and a tool at the end of its life do not leave the same surface, even when the offset is unchanged. We set tool life against surface finish and dimensional trend rather than a fixed number of parts. When the trend moves, the tool changes. This costs a little more in consumables and saves a great deal in rework.
Heat is the quiet variable
Stainless steel holds heat at the cutting zone. A part measured hot and a part measured at room temperature are not the same part. Roughing generates the heat, finishing removes the last few tenths, and coolant strategy decides whether the two interfere. We sequence the operations so the measured features are produced when the part is stable, and we check at a controlled temperature.
Passivation and ASTM A967
After machining, stainless couplers need a cleaning and passivation step that restores corrosion resistance without attacking the finish. ASTM A967 is the standard reference for chemical passivation treatments on stainless steel; we use it as the framework for the treatment and the acceptance discussion with the customer. Where a buyer needs documented material identity, we can provide EN 10204 3.1 certificates with the batch. Traceability is not paperwork for its own sake: it is how you answer a question about a fitting that has been in service for a year.
| Finish route | Typical roughness | Where it helps | Where it can hurt |
|---|---|---|---|
| Precision turning | Standard mirror Ra ≤ 0.6 µm | Cost-effective on simple seal seats | Tool marks may remain if the insert is wrong |
| 8K mirror finishing | Ra 0.2 µm | Low-friction, cleanable sealing surfaces | Adds process time; over-specifying wastes money |
| Electropolishing | Smooths micro-peaks after machining | Complex internal surfaces and deburr support | Can alter edges if not controlled |
| ASTM A967 passivation | Finish-dependent, not a roughness process | Restores stainless corrosion resistance | Will not fix a poor machined surface |

Liquid Cooling (AI Compute) CNC precision component
Tight Tolerance CNC vs Standard Turning: A Hard-Number Comparison
Two quotes can look identical on a spreadsheet and behave completely differently in your incoming inspection.
You do not need tight tolerance CNC on every feature of a coupler. You need it on the features that seal, locate, or relate to another part. The skill is knowing which is which, then refusing to pay a precision premium for a cosmetic diameter. Here is the comparison we use when a buyer asks why the quotes differ.
| Factor | Tight tolerance CNC route | General turning route |
|---|---|---|
| Mating-feature window | ±0.005 mm held and gauged in process | Shop-dependent; typically verified only at final inspection |
| Setups for body plus ports | One turn-mill composite clamping | Separate turn and mill fixtures, datum re-established |
| Seal seat finish | Ra ≤ 0.6 µm, 8K Ra 0.2 µm available | Finish as-machined unless separately specified |
| Burr control | Defined operation plus borescope sample check | Usually manual, subjective, inconsistently recorded |
| Batch traceability | Heat lot carried with the batch report | Often limited to a purchase order number |
| Ramp behaviour | Process locked before volume steps up | Offsets adjusted as volume exposes drift |
| Quality framework | ISO 9001 certified; ISO 13485 system established and certification in progress; IATF 16949 application in progress | Varies by supplier; ask for the certificate and scope |
Six factors, one at a time
- 1. Tolerance stack. Add up the tolerances along the sealing path. If three features each eat half the window, the assembly has no window left.
- 2. Datum chain. Count the number of times the part is re-clamped between the datum and the seal face. Every re-clamp is a relationship you must inspect.
- 3. Surface texture. Decide which face seals and specify that face. A blanket mirror-finish note is expensive and vague.
- 4. Cleanliness. Ask how burrs are removed and how the supplier proves it on a sample basis.
- 5. Evidence. Ask for a real dimensional report on the functional features, not a generic certificate of conformity.
- 6. Capacity proof. Ask what the supplier actually runs per month, and what share of that your program would consume.
Decision table: which route fits your part
| Your requirement | Recommended route | Why it wins |
|---|---|---|
| Pressure seal on a compact body | Tight tolerance CNC with turn-mill composite | Seat and port relationship built in one setup |
| Prototype, low volume, forgiving geometry | Standard turning with a careful drawing | You avoid paying for process control you do not yet need |
| Ramp to 20,000 units/month | Locked process, in-process gauging, batch records | Consistency matters more than the first article |
| Customer audit or regulated end use | Documented system and traceability | You can answer questions months after delivery |
| Corrosive or deionized coolant | Stainless with controlled finish and passivation | Surface condition drives long-term behaviour |
Do not buy a tolerance. Buy evidence that the tolerance still exists on the thousandth part.
Choosing CDU Coupler Assemblies Partners: Five Checks Before Your PO
The five documents you should ask for before a purchase order, not after a problem.
Supplier selection is less about adjectives and more about what a factory is willing to put in writing. When you are sourcing CDU coupler assemblies, these are the five things we would ask for in your position. We keep them ready because our customers ask for them.
- A DFM response that names your functional surfaces and tells you which tolerances drive cost. If a supplier says yes to every callout without comment, they have not read the drawing.
- Material certificate and heat-lot identification that can be tied to the batch you receive.
- An initial dimensional report on the seal seat, mating diameters, and the relationship between them, measured after the final machining operation.
- A defined burr-control and cleaning process, with the sample inspection method stated.
- A capacity and ramp statement: monthly output, the equipment behind it, and how your volume fits into the plan.
Red flags in a low quote
- The quote is fast and unconditional, with no questions about the seal face or the port geometry.
- The supplier offers a mirror finish on every surface, which usually means they have not thought about which surface matters.
- Traceability is described as available but is not included in the batch documentation.
- The sample is excellent and the production plan is vague. One good part is not a process.
- The factory address is an office, and a visit to the machining floor is politely avoided.
If you want to see how we handle the first item, send your drawing for a free DFM review. You will get a short, specific list of what we would hold and what we would question, which is useful information whether or not you order from us.

Liquid Cooling (AI Compute) CNC precision component
Common Mistakes in Liquid-Cooling Coupler Machining (And How We Avoid Them)
Most coupler failures are process failures that were visible in the drawing stage.
| Mistake | Symptom you will see | What we do instead |
|---|---|---|
| Finishing the seal seat before all heavy cuts | Part passes at inspection, leaks after assembly | Rough first, then finish the seat in a stable condition |
| Re-clamping between thread and seat | Seal face scored during assembly, inconsistent leak results | Turn-mill composite in one clamping with a common datum |
| Treating deburr as a manual afterthought | Debris in cold-plate channels, intermittent blockage | Defined deburr operation with a borescope sample check |
| Specifying mirror finish everywhere | High price, no improvement in sealing | Specify the sealing face; leave non-functional surfaces alone |
| Cannot read a first-article report | Trend accepted as normal variation | Review the functional dimensions before releasing volume |
Mistake 1: polishing instead of controlling geometry
A bright surface photographs well. It does not guarantee a flat one. When a buyer asks for the highest gloss available, we ask what the gloss is meant to achieve. If the answer is sealing, we talk about flatness, lay direction, and edge condition. If the answer is appearance, we tell them they are paying for something the fluid will never notice.
Mistake 2: confusing a sample with a process
A supplier can make one beautiful coupler on a quiet afternoon. The question is what the five-hundredth looks like at the end of a shift. Ask for the control plan: how offsets are checked, when tools are changed, and what happens when a dimension starts to walk. If there is no answer, the sample was luck.
Mistake 3: ignoring the fluid chemistry
Water-glycol and dielectric fluids do not treat every stainless surface the same way. Chloride content, temperature, and stagnation all matter. We ask buyers what is actually in the loop before finalising finish and passivation. It is a short conversation that prevents a long corrosion investigation.
From 20,000/Month to Traceable Batches: CNC Precision Machining Controls
Volume changes the problem. The first part is a craft question; the ten-thousandth is a system question.
Batch traceability that survives an audit
Incoming batch traceability means the bar stock identity follows the job through machining, finishing, and packing. If a customer calls eighteen months later about a fitting, we can tell them which material lot it came from and which process conditions applied. For AI compute infrastructure, where a rack may run for years before anyone opens it, that record is part of the product.
Capacity without hand-waving
When we say a program can ramp, we mean it against a known base: 60 CNC machines, a 4,000 m² plant expanded in 2026, and roughly 500,000 parts produced per month across the business. The coupler program's 20,000 units a month is a meaningful order but not a stretch on capacity. The constraint is discipline: keeping the process locked and the records complete as volume steps up.
The quality framework behind the numbers
Our ISO 9001 certification provides the documented framework for process control and continual improvement. The ISO 13485 system, established with certification in progress, pushes the same discipline further in the direction of medical-grade traceability. IATF 16949 remains at the application stage. We also support small-batch custom work alongside mass production, which means a prototype order receives the same engineering attention as a production release.
Pros
- Work with a source factory if you want to see the machines, ask the operator, and change a process quickly.
- Work with us if you need prototype quantities and a 20,000-unit ramp under one quality framework.
- Work with a partner who will tell you when your tolerance is unnecessary, because that is where money is saved.
Cons
- Do not expect a source factory to act as a system integrator; we machine the interface, you own the loop design.
- Do not expect the fastest answer if your drawing is ambiguous. We will ask questions before cutting.
- Do not choose us on price alone if your programme needs a certification we have not yet obtained. Ask for the current status.
Since 2015, Dongguan Licun Technology has supplied precision parts to customers including De'Longhi, Donlim, and Breville, supported a UAV customer whose first order reached RMB 1.2 million, and built an annual output value above RMB 20 million. Those are capability markers, not the story of this coupler program, which remains confidential. If you want to understand how LusterControl approaches a liquid-cooling interface, start with the drawing.

Liquid Cooling (AI Compute) CNC precision component

Liquid Cooling (AI Compute) CNC precision component

Liquid Cooling (AI Compute) CNC precision component

Liquid Cooling (AI Compute) CNC precision component
FAQ: CDU coupler assemblies & Liquid Cooling (AI Compute) Buyer Questions
A: Specify the functional surface, not the whole part. For a stainless coupler we commonly work to a ±0.005 mm capability window on mating diameters and hold the seal face to a defined flatness and roughness. Ask your supplier to report those features after the final machining operation. A blanket tight tolerance on non-functional diameters only raises cost.
A: Yes, we can take stainless to 8K mirror at Ra 0.2 µm. Our standard mirror finish is Ra ≤ 0.6 µm. Whether the finer finish helps depends on your seal type and fluid; on some elastomer seals, surface texture and edge condition matter more than gloss. We will tell you if the finer finish is justified for your geometry.
A: For one anonymous program with bar-fed turn-mill geometry, we moved from drawing review to a controlled ramp toward 20,000 units per month within a 30-day window, with customer validation at each gate. That is not a universal promise. Material, geometry, qualification requirements, and test criteria all change the schedule.
A: Yes. Confidentiality is our normal operating procedure. We run NDA and controlled drawing access for customer programs including De'Longhi, Donlim, and Breville, and we apply the same discipline to anonymous liquid-cooling projects. We discuss process and capability, never a customer's identity or design details.
A: We use ASTM A967 as the reference framework for chemical passivation of stainless steel, and we can provide EN 10204 3.1 material certificates with the batch when required. Incoming material lots are carried through machining, finishing, and packing so the batch can be reconstructed later. Our quality system is ISO 9001 certified; the ISO 13485 system is established with certification in progress, and IATF 16949 is at the application stage.
A: Yes. We handle small-batch custom work and volume production under the same engineering process. That means a prototype gets a real DFM review and a dimensional report, and a production ramp gets a locked process with in-process gauging and batch records. You do not have to change supplier between sample and series.
Send us your CDU coupler drawing for a free DFM review. We will tell you which tolerances drive cost, which ones you can relax, and whether your ramp target is realistic before you commit a purchase order.
Request a Free CNC Quote