CNC Needle Valve Bodies: Machining & Tolerances for Tooling and Fixtures (2026 Guide)
If you have ever watched a test bench drift off its setpoint, or an analytical instrument report a flow that was not really there, the cause is often smaller than the problem suggests. Behind the drift sits a needle valve body: the machined housing that guides a tapered stem into a seat and meters flow a drop at a time. In calibration rigs, chromatography skids, leak-test fixtures, and coolant dosing loops, that little body decides whether your flow stays repeatable to the last percent or quietly wanders. If you are specifying parts for instrumentation, fixtures, or precision fluid control, the body is not a commodity. It is the component that holds the tolerance budget the whole system depends on.
This guide is written the way an engineer would explain it to a colleague. We cover how CNC precision machining turns a bar of stainless into a needle valve body you can trust at plus or minus 0.005 mm, why surface finish down to Ra 0.2 micrometre mirror matters on a sealing seat, how to choose between a machined body and other flow-control options, and the checklist we use to qualify a supplier of tooling and fixtures CNC parts. We keep it practical and honest, with real numbers rather than adjectives.
We are Dongguan Licun Technology Co., Ltd. (brand LusterControl), a Dongguan source factory that has machined stainless steel since 2015. So we speak from the shop floor, not a catalog. By the end you should be able to write a needle valve body specification that a good shop can actually hold, and to spot the red flags before you ever place an order.
Table of Contents
- 1. Why Needle Valve Bodies Are Critical to Precision Flow Control
- 2. How CNC Precision Machining Shapes a Reliable Needle Valve Body
- 3. Tight Tolerance CNC: The Accuracies a Needle Valve Seat Actually Needs
- 4. Stainless Steel Mirror Finishing for Needle Valve Seats and Stems
- 5. Custom CNC Parts: Designing Needle Valve Bodies for Your Assembly
- 6. Tooling and Fixtures CNC Parts: Holding and Inspecting Needle Valve Bodies
- 7. Needle Valve Bodies vs Other Flow-Control Methods: A Comparison
- 8. A Buyer's Checklist for Sourcing Needle Valve Bodies
- 9. Common Mistakes Engineers Make When Specifying Needle Valve Bodies
Tooling&Fixtures CNC precision component
Why Needle Valve Bodies Are Critical to Precision Flow Control
A needle valve body is where your flow accuracy is either locked in or quietly lost.
A needle valve body does one job that sounds simple and is anything but: it holds a precisely bored orifice and a guided tapered stem so that rotating the stem a fraction of a turn moves flow from fully closed to a metered trickle with fine resolution. In a calibration rig that resolution is your measurement. In a coolant or reagent dosing loop it is your dose. In a leak-test fixture it is the controlled bleed you trust. When the seat is concentric to the bore and the orifice is true, the valve repeats for tens of thousands of cycles. When it is not, you get creep, drip, and a setpoint that lies.
Where you actually find them
- Calibration and test benches, where a needle valve sets the reference flow the rest of the rig is judged against.
- Analytical and chromatography skids, where reagent or carrier flow must stay repeatable across a long run.
- Leak-test and pressure fixtures, where a controlled micro-bleed verifies a seal without flooding the part.
- Coolant, lubricant, and additive dosing loops, where the body meters a small, steady stream into a process.
- Vacuum and specialty gas lines, where a fine, repeatable throttling point beats a fast on or off valve.
The takeaway is simple. The body looks like a small machined block with a couple of holes, and that is exactly why it is easy to under-specify. Treat it like the precision component it is and your whole flow loop behaves. Treat it like a fitting and you will spend the savings on troubleshooting and re-validation.
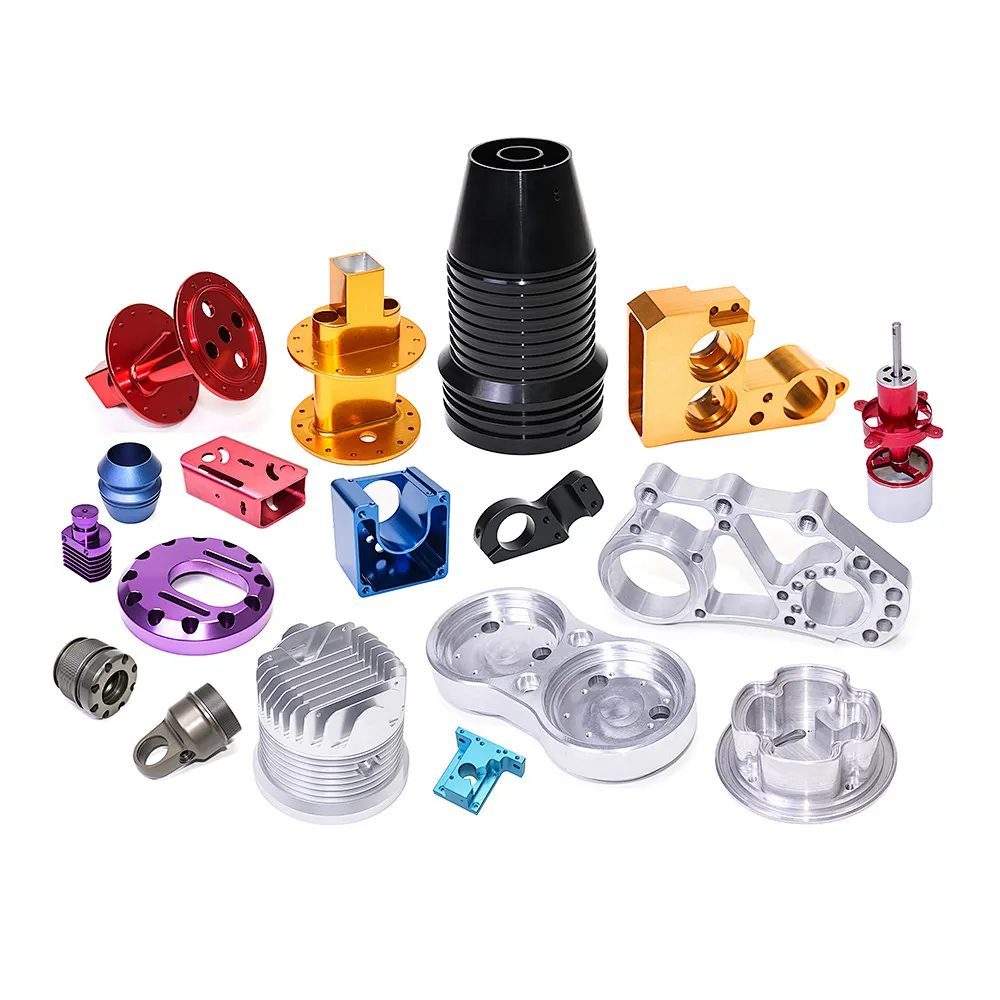
Tooling&Fixtures CNC precision component
How CNC Precision Machining Shapes a Reliable Needle Valve Body
The process you choose decides whether the seat stays true to the bore in the real world.
A reliable needle valve body is not the product of one magic machine. It is the product of choosing the right sequence so that every critical feature is referenced to the same datum. For a body, the orifice, the bore that guides the needle, the port threads, and the sealing face all have to agree with each other, and the only way to guarantee that is to keep the part clamped to one datum through as many operations as possible.
From bar stock to finished body
- Select the grade. For general instrument service we often use free-machining 303; for wetted or corrosive service we move to 304 or 316L.
- Turn the bore and outer profile on a Swiss-type or CNC lathe so the bore is true to the OD before any port exists.
- Mill or drill the cross port and seat on a 4 or 5 axis center, referencing the already-turned bore as the datum.
- Use turn-mill compound machining to add hex bodies, wrench flats, or integrated bosses in the same clamp, protecting the stack-up of tolerances.
- Deburr and passivate to ASTM A967 so the part is clean and corrosion-resistant, not just shiny.
- Inspect with CMM for geometry and a profilometer for finish, because we do not guess the numbers that matter.
Why we combine operations
- Turn-mill compound
- A machine that turns and mills in one setup, so a part keeps one datum and tolerances do not accumulate from moving between machines.
- Swiss-type turning
- A sliding-headstock lathe ideal for long, slender, tightly toleranced bores and small bodies.
- Datum
- The reference surface or axis from which every other dimension is measured; protecting it protects your tolerance.
- ASTM A967
- The standard that defines how stainless steel is passivated to maximize corrosion resistance.
| Process | Best for | Typical tolerance | Volume |
|---|---|---|---|
| Swiss-type turning | Slender bores, small bodies | ±0.005 mm | Low to high |
| 5-axis milling | Cross ports, integrated bosses | ±0.01 mm | Prototype to mid |
| Turn-mill compound | Body with milled hex or flange | ±0.008 mm | Mid to high |
| Passivate + electropolish | Final finish on 304 or 316L | Ra 0.2 µm | All |
For tooling and fixtures CNC parts especially, combining operations in a single clamp reduces the error stack-up that comes from moving a part between machines. Process choice here is a quality decision, not just a cost one.
Tight Tolerance CNC: The Accuracies a Needle Valve Seat Actually Needs
Tighter is not automatically better. Tolerance has to serve a function.
Every tighter tolerance you put on a drawing costs money in cycle time, tooling wear, inspection, and scrap. The disciplined approach is to tighten only the features that actually control flow and sealing, and to leave the rest at a sane commercial tolerance. A good supplier will tell you which features matter for your needle valve body and which are quietly wasting your budget.
Tolerances that matter by feature
| Feature | Typical tolerance | Why it matters |
|---|---|---|
| Bore diameter | ±0.005 mm | Guides the needle true, no wobble at the seat |
| Orifice diameter | ±0.01 mm | Sets the minimum flow and shutoff resolution |
| Seat concentricity to bore | ±0.01 mm | Keeps the needle centred for repeatable throttling |
| Port thread pitch | ±0.02 mm | Leak-free connection to the fixture or line |
| Flatness of sealing face | ±0.01 mm | Gasket or ferrule seats without weeping |
- Runout (TIR)
- Total indicator reading; how far a feature wobbles as the part rotates.
- Concentricity
- How well the seat orifice shares the centre axis of the bore.
- Shutoff resolution
- The smallest flow change you can make by turning the stem one detent.
Pros
- Predictable fit and flow
- Lower assembly scrap
- Easier validation and repeat orders
Cons
- Tighter features cost more to hold
- Not every feature needs them
- Inspection time grows with each tight callout
When you talk to a supplier about tooling and fixtures CNC parts, ask them to mark up your drawing with the features they would hold tight and the ones they would relax. The answer tells you whether they understand a needle valve body or are just quoting metal.
Tooling&Fixtures CNC precision component
Stainless Steel Mirror Finishing for Needle Valve Seats and Stems
On a sealing seat, finish is a leak-tightness and cleanliness issue, not a cosmetic one.
A needle valve seat in a wetted, analytical, or washdown environment lives in contact with chemicals, moisture, and sometimes pharma or reagent-grade media. A rougher surface gives contamination a place to lodge and gives the seat microscale leakage paths that defeat a fine shutoff. A mirror finish down to Ra 0.2 micrometre, what we call 8K, is smoother, easier to clean, and far more durable. That is why stainless steel mirror finishing belongs in the specification, not the sales brochure.
How we reach a true mirror finish
- Start with the correct grade, typically 304 or 316L for wetted service.
- Machine to a clean baseline so polishing has little material to remove.
- Passivate to ASTM A967 to rebuild the chromium-oxide layer that makes stainless resist corrosion.
- Electropolish to level micro-peaks and drop Ra toward 0.2 micrometre.
- Verify with a profilometer, because a guess is not a measurement.
| Finish grade | Typical Ra | Where it is used |
|---|---|---|
| Standard machined | 0.8 µm | Non-critical body covers |
| Fine turned | 0.4 µm | Dry instrument housings |
| Mirror (8K) | 0.2 µm | Wetted seats, pharma, reagent, gas valves |
For more on how a Dongguan source factory runs this discipline at scale, our Dongguan Licun Technology page lays out the plant, the certifications, and the process controls behind every part.
Custom CNC Parts: Designing Needle Valve Bodies for Your Assembly
Most needle valve problems are decided at the drawing stage, not on the shop floor.
Off-the-shelf valve bodies rarely fit a compact fixture, a tight instrument bay, or a specialist media path. Custom CNC parts let you integrate the body, ports, boss, and mounting flange into one machined piece, which removes joints that could loosen and datums that could shift. The design choices you make in CAD are what keep the part honest in the field.
Design choices that protect your tolerance
- Integrate the boss and mounting flange instead of brazing a separate one, so the bore and ports never decouple.
- Use a true bore sized to your needle rather than an undersized hole finished by reaming blind.
- Add a hex or wrench flat so the body can be torqued without spinning the seat out of round.
- Match the port thread exactly to your fitting standard, not approximately to a look-alike.
- Call out finish only where the part is wetted or cleaned, to control cost.
Custom does not mean expensive when the volume is there. Because we run both small custom batches and half a million parts a month, a needle valve body design can grow from first prototype to full production without re-qualifying the source.
Tooling&Fixtures CNC precision component
Tooling and Fixtures CNC Parts: Holding and Inspecting Needle Valve Bodies
The body is only as good as the fixtures that hold it and the gauges that prove it.
A needle valve body is small, often asymmetric, and unforgiving of movement during the cut. The difference between a repeatable seat and a scrap batch is usually the fixture, not the machine. This is the part of the job that separates a real tooling and fixtures CNC parts supplier from a broker with a logo, because the work happens before and after the spindle runs.
How we fixture the body
- Hardened locating pins reference the turned bore and OD so every subsequent cut shares one datum.
- A hydraulic or dovetail clamp holds the body without distorting the thin sealing face under cut load.
- Dedicated port-drill jigs keep the cross hole square to the bore without a second setup.
- A tensioning fixture lets thin-walled bodies spring back to free state before the final seat cut.
- Palletized fixtures let one program run the whole batch with no re-indication between parts.
Inspection tooling and gauges
- First-article CMM report with full datum references for the bore, orifice, and seat concentricity.
- Thread plug and ring gauges to prove the port connection before the part leaves the cell.
- A profilometer check on the seat to confirm the Ra target is met, not assumed.
- A leak or bubble test on wetted bodies to prove shutoff at the specified pressure.
- Batch traceability tying each lot to its material cert, machine, operator, and CoC.
| Tooling or gauge | What it controls | Why it matters |
|---|---|---|
| Dedicated fixturing | Datum repeatability | Stops tolerance stack-up across the batch |
| CMM first article | Bore, orifice, concentricity | Proves the drawing was actually met |
| Thread gauges | Port connection | Leak-free fit to your fitting standard |
| Profilometer | Seat Ra | Verifies mirror finish instead of guessing |
| Leak test rig | Shutoff | Confirms the valve actually holds pressure |
For a deeper look at related precision components, browse our technical guides on tooling and fixtures CNC parts and tight tolerance CNC machining.
Needle Valve Bodies vs Other Flow-Control Methods: A Comparison
The right device is the one matched to your resolution, media, and space need.
A needle valve is not the only way to meter or stop flow inside an instrument or fixture. Ball valves, globe valves, and metering pumps all exist, and each wins in a different scenario. The mistake is picking by habit instead of by requirement. Below is the honest trade for a precision flow-control context.
| Factor | Needle valve | Ball valve | Globe valve |
|---|---|---|---|
| Flow resolution | Excellent, fine throttling | On or off only | Good, coarser than needle |
| Shutoff tightness | Excellent with mirror seat | Good | Good |
| Space | Compact, body-integrated | Bulky | Bulkiest |
| Media tolerance | Great for gas and reagent | Limited for fine gas | Fine for liquid |
| Cost at volume | Low to medium | Low | Medium |
| Best use | Metering, calibration, bleed | Quick isolation | Larger liquid throttling |
Choose a needle valve body if
- You need fine, repeatable throttling between fully closed and a small flow.
- Space is tight and you want the body integrated into a fixture or instrument.
- Your media is gas, reagent, or clean fluid where tight shutoff matters.
- Your priority is resolution and repeatability, not raw flow capacity.
Choose another option if
- You only need fast on or off isolation, where a ball valve is simpler and cheaper.
- You are moving large liquid volumes, where a globe or pump is stronger.
- Tolerance to seat wear over millions of cycles would break your accuracy budget.
Pros
- Low cost, fine resolution, easy integration
- Compact, repeatable shutoff
Cons
- Not for high flow
- Seat wear matters over very long life
For a deeper look at related flow-control components, browse our technical guides on fluid control and valve CNC parts and tight tolerance CNC machining.
Tooling&Fixtures CNC precision component
A Buyer's Checklist for Sourcing Needle Valve Bodies
Copy this and send it to every shop on your shortlist. The answers will sort them fast.
- Can they show ISO 9001 with real QMS records, and ISO 13485 where medical or pharma fluid service is involved?
- Do they machine 303, 304, and 316L stainless regularly, not as a one-off?
- Can they state a finish target such as Ra 0.2 to 0.4 micrometre and verify it with a profilometer?
- Will they passivate to ASTM A967 and document it, not just claim a bright look?
- Do they provide first-article CMM, thread gauges, and leak test data on every lot?
- Are tolerances quoted against your drawing, with tight callouts only where flow or sealing depends on them?
- Can they support prototype to production without re-qualifying the process?
- Do they answer engineering questions with specifics, not sales talk?
A supplier that clears all eight is rare and worth keeping. One that stumbles on traceability, passivation, or finish verification should not be on a needle valve body program where a single bad lot becomes a recall or a failed calibration.
Common Mistakes Engineers Make When Specifying Needle Valve Bodies
Most failures we see were locked in at the sourcing stage, not on the shop floor.
- Chasing the lowest bid, when the saving evaporates in rework, delays, and validation restarts.
- Leaving finish as 'smooth' on the drawing, then arguing about it after shipment.
- Over-tolerancing every feature, which forces scrap and slows delivery for no functional gain.
- Ignoring seat concentricity, so the valve creeps even though each feature 'measures fine'.
- Skipping first-article inspection to save time, which is the cheapest insurance you have.
- Forgetting traceability, so a single complaint becomes a full stop-ship instead of a targeted fix.
None of these mistakes are technical. They are habits, and the disciplined supplier you choose should make the right habit the easy default. That is the difference between a valve that meters for years and one that becomes a service call.
Tooling&Fixtures CNC precision component
Tooling&Fixtures CNC precision component
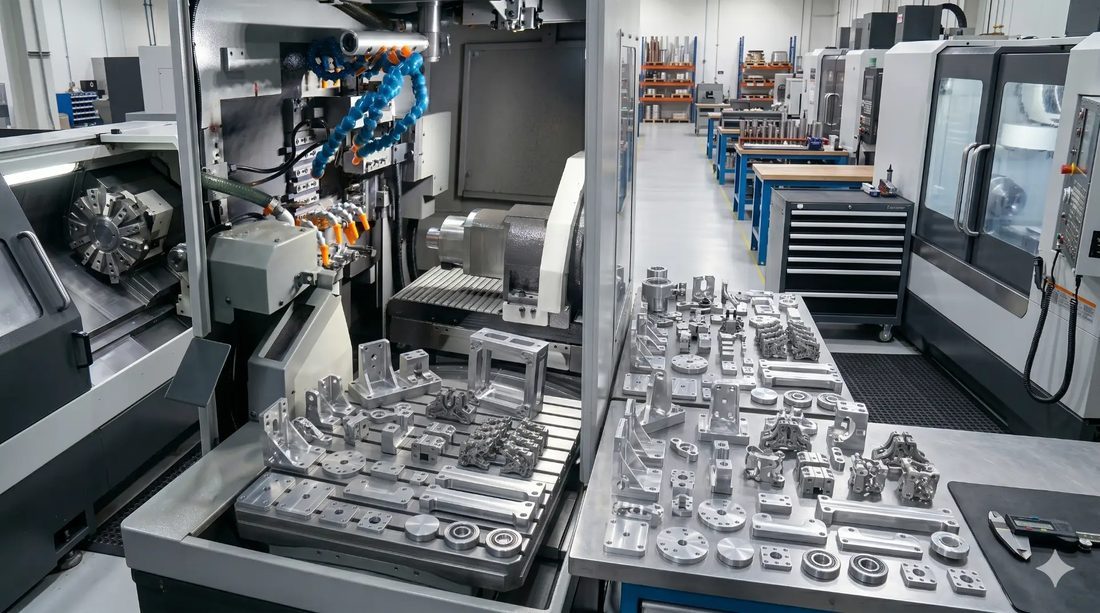
Tooling&Fixtures CNC precision component
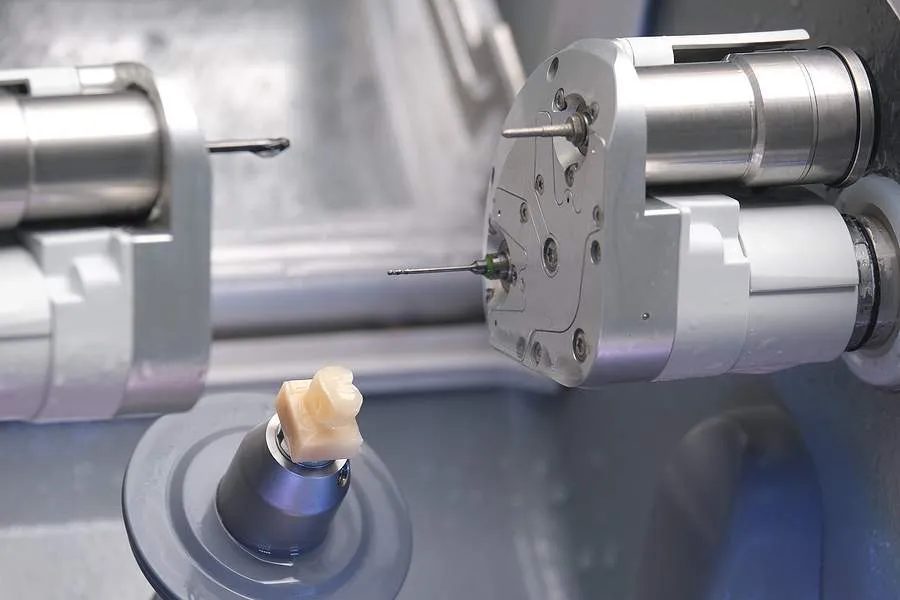
Tooling&Fixtures CNC precision component
FAQ: needle valve bodies & Tooling&Fixtures Buyer Questions
A: We routinely hold plus or minus 0.005 mm on the bore and plus or minus 0.01 mm on the orifice, seat concentricity, and port thread pitch for needle valve bodies, with runout controlled to plus or minus 0.02 mm. Every number is verified by CMM and profilometer rather than estimated.
A: For dry instrument service, free-machining 303 is common. For wetted, reagent, or corrosive service, 304 or 316L is the right choice, with 316L preferred for pharma, marine, or chemical lines because of its higher pitting resistance. The grade should match the media, not the price list.
A: On a sealing seat a rougher surface gives contamination and microscale leakage a place to start and defeats a fine shutoff. A mirror finish down to Ra 0.2 micrometre, our 8K, is smoother, easier to clean, and more durable. Always specify the Ra target and verify it with a profilometer.
A: Yes. We run first-article inspection on new designs, support low-volume custom runs, and scale to monthly volume while keeping the same documented process and batch traceability, so your program grows without re-qualifying the source.
A: Every lot is tied to its material mill certificate, the machine and operator that ran it, in-process inspection records, and a Certificate of Conformance. Any shipped needle valve body can be traced back to its full history, which is what a recall-ready program requires.
A: State the material grade, the port thread standard matched to your fittings, the bore and orifice, the seat finish such as Ra 0.2 micrometre where wetted, the tight tolerances only on features that control flow and sealing, and your volume. Send the drawing and a good shop will return a free DFM review before you cut metal.
Ready to turn your needle valve body drawing into a part you can trust at plus or minus 0.005 mm? Send us your drawing for a free DFM review with tolerance and finish recommendations. No obligation, just a clear engineering answer from LusterControl.
Request a Free CNC Quote