CNC Nozzles for Optical Applications: A Complete 2026 Technical Guide
If your product has an optical surface in it - a lens, a sensor window, a fiber tip, a coating chamber - then the nozzle feeding it fluid, gas, or coating mist is not a commodity fitting. It is the part that decides whether that surface stays clean. A burr, a scored bore, or a five-micron oversize orifice changes spray angle, throws off flow rate, and seeds the very defects your optical inspection is trying to catch. We have watched this happen on lens-washing arms and on spray coating heads, and the root cause was almost always treated as 'just a nozzle.'
In this guide we walk through how to specify and source optical-grade nozzles the way an engineer actually should: what the orifice tolerance budget really buys you, why the internal bore finish matters more than the outside polish, how material and passivation keep particles out of a clean optical path, and which process wins for your volume. We will also give you a buyer's checklist you can hand a supplier today - the same questions we answer with data when a photonics or medical customer quotes with us.
We are Dongguan Licun Technology Co., Ltd. (brand LusterControl), a South-China source factory focused on CNC lathe stainless-steel mirror finishing for 15 years since 2015. Our floor runs 60 CNC machines across a 4,000 sqm plant (expanded in 2026; the old 2,000 sqm site is retired), with monthly output around 500,000 parts, ISO 9001 certified, ISO 13485 completed, and IATF 16949 in application. This is written from the shop floor, not a catalog.
Table of Contents
- 1. Why Nozzles and Their Geometry Decide Your Optical CNC Parts Quality
- 2. How CNC Precision Machining Shapes Optical Nozzle Flow Paths
- 3. Tight Tolerance CNC: Holding +/-0.005 mm on Nozzle Orifices
- 4. Stainless Steel Mirror Finishing for Optical-Grade Nozzles
- 5. Custom CNC Parts: Designing One-Off Optical Nozzles
- 6. CNC Nozzles vs Other Processes: Which Wins for Optical Components?
- 7. A Buyer's Checklist for Sourcing Optical CNC Parts Right
- 8. Real CNC Precision Machining Programs We Have Shipped
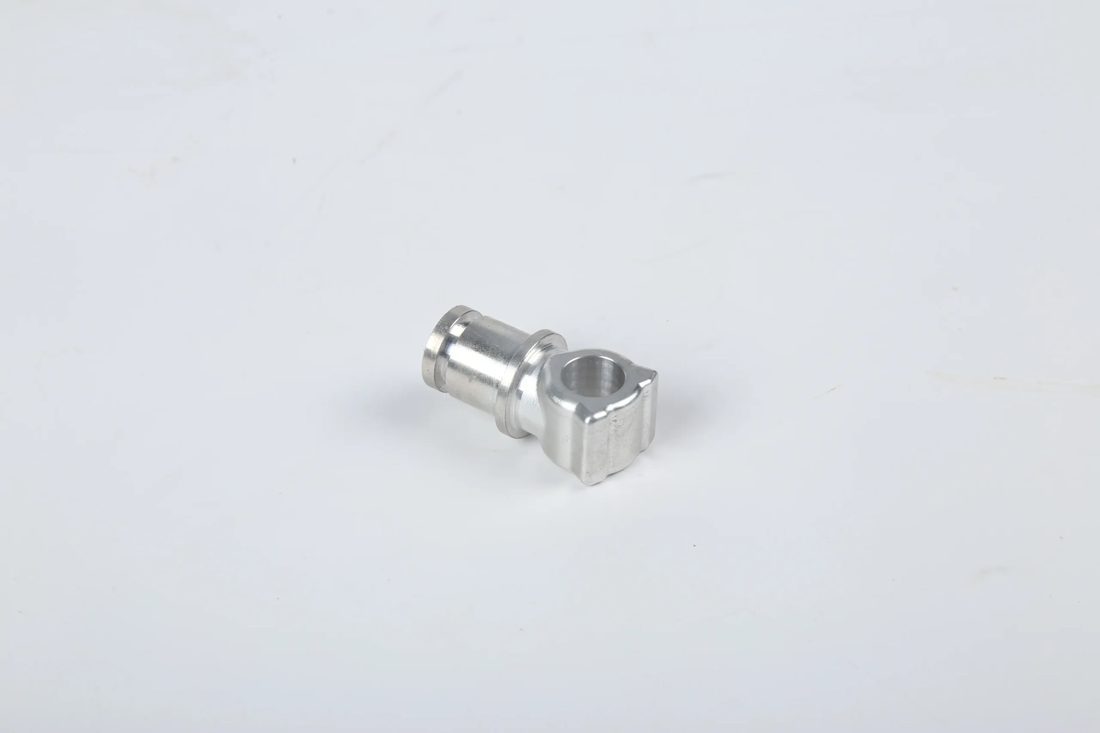
Optical CNC precision component
Why Nozzles and Their Geometry Decide Your Optical CNC Parts Quality
The nozzle is the last thing between your fluid and your optical surface - treat it like one.
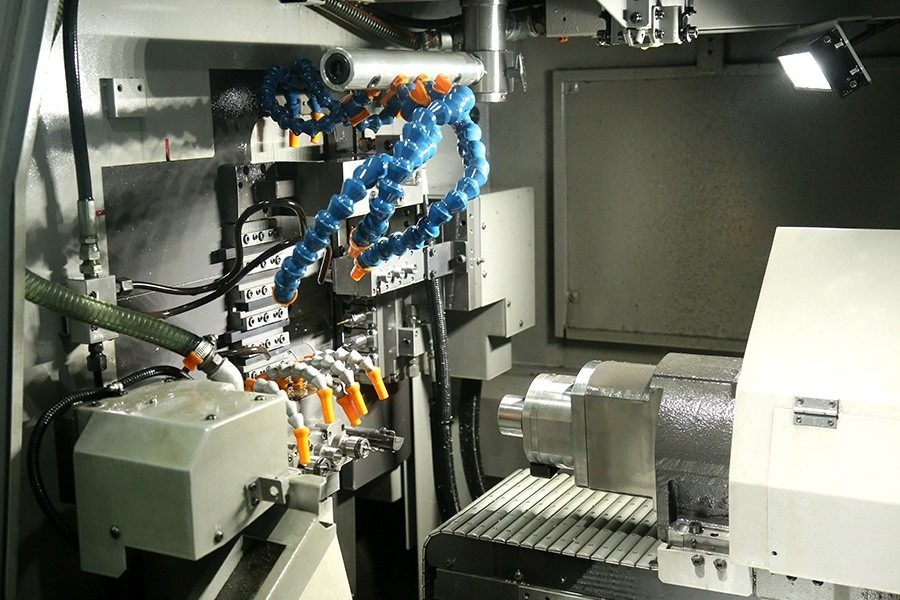
An optical nozzle does one job under pressure: deliver a repeatable stream or spray to a surface you cannot afford to scratch. The geometry that controls that - orifice diameter, inlet taper, internal land length, and the concentricity of the bore to the body datum - is what separates a clean, repeatable process from one that drifts part to part. When you are coating lenses or washing sensor windows, a 5 micron change in orifice size can swing flow by more than 10 percent, and that shows up as coating thickness variation your metrology flags later.
The trap most buyers fall into is specifying the outside of the nozzle and forgetting the inside. The external thread and hex are trivial; the internal flow path is where optical-grade behavior lives. We tell customers to put their tolerance budget on the orifice and the bore, relax everything cosmetic, and define a cleanliness class up front. That single decision removes most of the field failures we see in optical CNC parts programs.
What 'optical-grade' actually demands
- Orifice held to tight tolerance CNC limits, typically +/-0.005 mm
- Bore surface finished to Ra 0.2 um mirror where flow turbulence seeds defects
- Full burr-free edge at the orifice - no wire-drawn lips
- Passivated stainless per ASTM A967 so particles do not shed
- Lot-level traceability from raw bar to finished nozzle
Optical CNC precision component
How CNC Precision Machining Shapes Optical Nozzle Flow Paths
A clean flow path is a machined flow path - not a drilled one.
CNC precision machining lets us cut the entire internal profile - inlet chamfer, converging taper, orifice land, and outlet relief - in one coordinated program rather than stacking separate drilling and reaming steps. That coherence is what keeps the bore concentric to the body datum and the orifice axis where the drawing puts it. For an optical nozzle, axis location is not a nice-to-have; it is what keeps the spray cone centered on the lens.
Step 1 - Rough and establish datum
We first turn or mill the external body and the primary locating diameter, then lock that as the machining datum for every internal operation. Because the part never leaves that datum, the orifice centerline stays true to the body within our +/-0.005 mm positioning accuracy. This is the step that makes the rest of the flow path trustworthy.
Step 2 - Form the internal taper and land
The converging section is cut with a fine finishing pass and, where the spec calls for it, a custom ground tool that matches the designed taper angle. We leave 0.05 to 0.1 mm for the final pass so heat and spring don't print into the bore. On micro-orifices we use Swiss-type sliding-headstock lathes so the spinning tool stays supported right at the cut - that is how we hold small bores round and burr-free.
Step 3 - Mirror finish and verify
For optical use we take the bore to our mirror line, reaching Ra 0.2 um on the flow surfaces, then verify on a first-article CMM and a bore-scan where the orifice is small enough to matter. Batch parts get in-process gauging and lot audits so a tool-wear drift shows up before a bad lot ships. The result is a nozzle whose internal finish does not shed particles into a clean optical path.
Tight Tolerance CNC: Holding +/-0.005 mm on Nozzle Orifices
Tolerance is a budget - spend it on the orifice, not the hex.
The single number that usually matters most on an optical nozzle is the orifice diameter, and that is exactly where tight tolerance CNC earns its keep. We hold the orifice to +/-0.005 mm and the orifice-to-body concentricity to a similar band, because both directly set spray angle and flow consistency. Everything else - wrench flats, collar, external thread - gets commercial tolerances so we are not paying for precision you will never measure in service.
- Orifice
- The final discharge hole of the nozzle; its diameter and edge quality set flow rate and spray cone.
- Concentricity
- How true the orifice axis is to the body locating datum; poor concentricity throws the spray off-center.
- Ra (roughness)
- Arithmetic average surface height in micrometers; lower Ra means a smoother, less particle-shedding bore.
A practical note for buyers: ask for the tolerance in the coated or passivated condition, not the bare machined size. ASTM A967 passivation and any thin film add microns, and we machine the orifice undersize so the finished, treated bore lands at nominal. Designing to the bare condition is the classic mistake that makes a 'correct' nozzle measure oversize after treatment.
| Feature | Where to spend tolerance | Typical callout |
|---|---|---|
| Orifice diameter | Critical | +/-0.005 mm |
| Orifice concentricity | Critical | +/-0.01 mm TIR |
| Bore surface (Ra) | Critical for optics | Ra 0.2-0.4 um |
| External thread/hex | Commercial | 6g / loosen |
| Collar length | Loose | +/-0.1 mm |
Optical CNC precision component
Stainless Steel Mirror Finishing for Optical-Grade Nozzles
Inside polish is what keeps particles out of your optical path.
Stainless steel mirror finishing is not cosmetic here - it is a contamination-control strategy. A rough bore traps process fluid, dries into residue, and sheds micro-particles every cycle; a mirror bore (we reach Ra 0.2 um, an 8K-class finish) lets fluid sheet cleanly and gives particles nowhere to lodge. For lens-washing and coating-mist nozzles that operate in or near an optical surface, that difference is the line between a clean run and a defect cluster.
We combine mechanical mirror polishing with electropolish where the geometry allows it, then passivate per ASTM A967 so the stainless resists fingerprint and handling corrosion. Our standard precision line sits at Ra 0.6 um, and the mirror line at Ra 0.2 um - the same discipline we apply to the bores that feed optical surfaces so the sensor sees only the world, not the mill.
Pros
- Ra 0.2 um bores shed far fewer particles
- Electropolish smooths micro-crevices mechanical buffing misses
- Passivation per ASTM A967 stabilizes the surface
- Mirror finish improves flow repeatability
Cons
- Adds cycle time versus a turned-only bore
- Very small or blind bores are harder to polish
- Needs a defined cleanliness class to be worth it
- Costs more than a commercial finish
Custom CNC Parts: Designing One-Off Optical Nozzles
One-off nozzles are where DFM pays for itself before the first cut.
Most optical nozzles are custom CNC parts, not catalog items, because the spray angle, mount, and fluid chemistry are unique to your head. That is good news: a custom part means we can design the features that actually matter and drop the ones that only add cost. Our floor runs small-batch custom work next to volume, so a single prototype and a 50,000-piece lot use the same process - the only difference is qualification depth.
- Send the drawing plus the real fluid, pressure, and target spray angle
- Agree the orifice tolerance and the coated-condition callout
- Define the bore Ra and a cleanliness class
- Pick material and passivation (ASTM A967) up front
- Qualify at low volume with a CMM first article, then scale
- Drawing shows orifice in coated condition
- Spray angle and flow rate targets are both listed
- Bore Ra and cleanliness class are specified
- Material cert and passivation spec are agreed
- CMM first-article report is in the contract
Optical CNC precision component
CNC Nozzles vs Other Processes: Which Wins for Optical Components?
CNC is not always right - but for optical bores it usually is.
You can make a nozzle three other ways: Swiss screw machining, micro-casting, or 3D printing. Each has a place, but for optical-grade bores the comparison is decided by how well the process controls the internal finish and the orifice tolerance. The table below is the honest version - what each process really gives you when the part has to stay clean.
| Factor | CNC precision machining | Swiss screw | Micro-casting |
|---|---|---|---|
| Orifice tolerance | +/-0.005 mm | +/-0.008 mm | +/-0.02 mm, needs ream |
| Bore finish (Ra) | Ra 0.2 um mirror | Ra 0.4 um typical | Ra 0.8 um as-cast |
| Material freedom | Any machinable steel | Free-cutting grades | Castable alloys only |
| Min orifice | ~0.2 mm practical | ~0.3 mm | Limited, rough |
| Best volume | 1 to 500k/mo | High volume | Very high volume |
| Cleanliness | Excellent, traceable | Good | Needs heavy cleanup |
3D printing we flag separately: it is excellent for a concept nozzle you want to trial in a day, but the as-built internal surface is too rough and too porous for an optical path without post-machining the bore - at which point you are back to CNC for the part that matters. For optical components, machine the flow path.
Pros
- CNC gives the tightest orifice and cleanest bore
- Any stainless grade, full traceability
- One process from prototype to volume
Cons
- Higher piece cost than casting at huge volume
- Very long bores are slower to polish
- Design still needs a real DFM pass
A Buyer's Checklist for Sourcing Optical CNC Parts Right
Hand this to a supplier and you filter out the brokers from the shops.
Sourcing optical CNC parts like nozzles is less about finding a cheap machine and more about finding a shop that understands contamination-controlled intent. The questions below are the ones we are happy to answer with data, and they are exactly what separate a real precision source from a logo with a subcontractor.
- Ask for the cert stack: ISO 9001 minimum, ISO 13485 a strong plus for optics/medical
- Request material certs traceable to the heat lot
- Confirm mirror-bore capability (Ra 0.2 um), not just a turned finish
- Get a CMM first-article report with full datum references
- Agree orifice tolerance in the coated/passivated condition
- Verify batch traceability and a real rework path
- Ask how they control particles - cleanliness class, not just Ra
The cheapest optical nozzle is the one that passes qualification the first time - because the second time costs you a launch date and a customer's trust.
Optical CNC precision component
Real CNC Precision Machining Programs We Have Shipped
Numbers from the floor beat adjectives from a brochure.
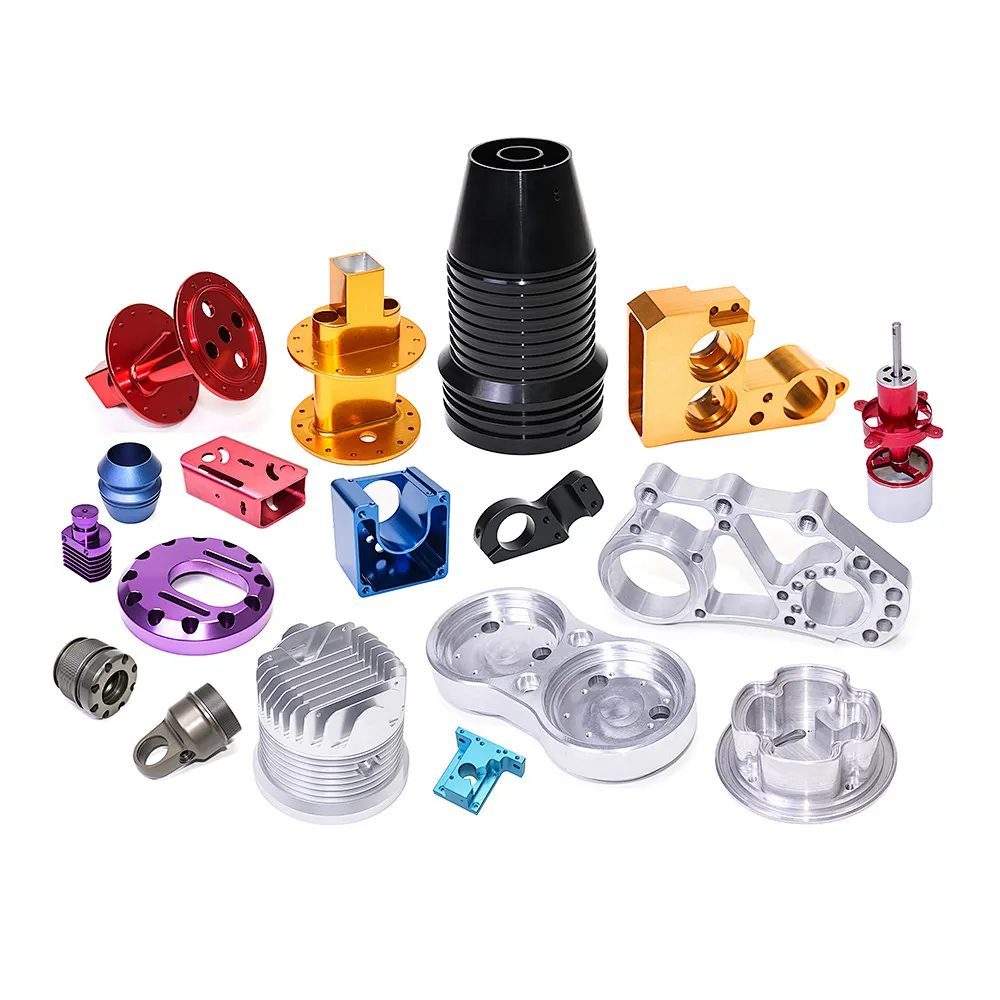
We have shipped precision CNC work to appliance and optics brands including De'Longhi, Donlim, and Breville, where mirror-finished stainless parts have to look and perform flawlessly on consumer-facing products. One UAV customer's first production order with us reached 1.2 million RMB, and our annual output now runs past 20 million RMB across the floor - proof that tight-tolerance custom work and volume are not opposites here.
For optical and medical-adjacent programs we apply the same discipline: single-datum machining for orifice truth, mirror bores to Ra 0.2 um where the flow matters, ASTM A967 passivation, and lot traceability from raw bar to finished part. Whether it is a one-off coating nozzle or a standing 500k/month run, the process is identical - only the qualification depth changes.
Optical CNC precision component
Optical CNC precision component
Optical CNC precision component
Optical CNC precision component
FAQ: nozzles & Optical Buyer Questions
A: We hold the orifice diameter to +/-0.005 mm and the orifice-to-body concentricity to about +/-0.01 mm TIR, because both set spray angle and flow consistency. The tolerance should be specified in the coated or passivated condition, since ASTM A967 treatment and thin films add microns that we machine away up front.
A: The bore is what touches your fluid and faces your optical surface. A rough bore traps residue and sheds micro-particles every cycle; a mirror bore at Ra 0.2 um lets fluid sheet cleanly and gives particles nowhere to lodge. For lens-washing or coating-mist nozzles that operate near an optical surface, internal finish is a contamination-control spec, not a look.
A: 316L is the default for corrosion resistance and cleanability; 17-4PH steps in when you need hardness or a precipitation-hardened body; 303 machines fastest but sacrifices some corrosion resistance. All should be passivated per ASTM A967. The right call depends on your fluid chemistry and whether the nozzle sees mechanical wear.
A: Only for a concept prototype you want to trial in a day. The as-built internal surface is too rough and porous for an optical path without post-machining the bore - at which point you are back to CNC for the flow path that matters. For production optical components, machine the bore.
A: Yes. We supply material certs traceable to the heat lot, a CMM first-article report with full datum references, in-process gauging for batch parts, and lot-level traceability from raw bar to finished nozzle - the same evidence a photonics or medical quality team needs to qualify the part.
A: Single prototypes are routine, and our floor is built for both one-off custom parts and volume up to 500,000 pieces a month across 60 machines. For a dedicated optical program we typically qualify at low volume with a CMM first article, then scale once the data is locked.
Send us your nozzle drawing for a free DFM review - we will flag the orifice tolerance that should move to tight tolerance CNC, the bore finish your optical path actually needs, and the coated-condition size so passivation never surprises you. Reach out and let's cut the first article.
Request a Free CNC Quote