CNC Rotors 2026: Machining & Tolerances for UAV/Drone Applications
A rotor is the part that actually turns air into thrust - but on a multirotor it is also the part that, if it is out of balance by a few hundredths of a gram, shakes the whole airframe, blurs the camera, and shortens every bearing in the drivetrain. You rarely get a warning before that happens; the first sign is usually a cracked printed arm or a gimbal that will not hold still.
So when you spec a rotor hub, a rotor shaft, or a motor bell, the real question is not 'how cheap can the blank be?' It is 'who can hold the runout, the concentricity, and the balance that keep this thing smooth at 8,000 rpm?' This guide is written the way we, as a precision shop, would qualify our own rotor work - and how you should qualify any supplier you are about to trust with flight-critical parts.
We have been a Dongguan source factory for stainless-steel precision CNC since 2015 - 15 years on the spindle. Today we run 60 CNC machines in a 4,000 m2 plant (expanded from 2,000 m2 in 2026) and ship around 500,000 machined parts a month. The numbers and trade-offs below are the ones we argue about with customers before a single chip is cut, not catalog claims.
Table of Contents
- 1. Why Rotors Demand Tight Tolerance CNC From the First Spin
- 2. How CNC Precision Machining Builds Balanced Rotors for UAV Flight
- 3. Rotor Materials: Where UAV/Drone CNC Parts Meet Weight and Strength
- 4. Custom CNC Parts vs Standard Rotors: When to Machine Your Own
- 5. Stainless Steel Mirror Finishing for Corrosion-Proof Rotor Shafts
- 6. Tight Tolerance CNC on Rotor Runout and Concentricity
- 7. Sourcing Custom CNC Parts: A Rotor Buyer's Checklist
- 8. Common Mistakes When Specifying Rotors for Drone Motors
UAV/Drone CNC precision component
Why Rotors Demand Tight Tolerance CNC From the First Spin
A rotor is a rotating mass. At speed, any asymmetry becomes a force you cannot un-see.
A rotor hub or shaft is a rotating mass, and the physics is unforgiving: the vibration force from an off-center feature scales with the square of rotational speed. A bore that is 0.02 mm off the shaft centerline is invisible on the bench, but at 10,000 rpm on a typical UAV prop it throws a centrifugal load that walks the motor, blurs the optics, and accelerates bearing wear until something fails. Tight tolerance CNC is what makes that load small enough to ignore.
What 'balanced' actually means
- Runout
- The total indicator variation as a surface rotates - how far the actual axis deviates from the ideal axis. On a rotor it is the headline number for smoothness.
- Concentricity
- How well two diameters share the same center axis. A rotor bore and its outer pilot must be concentric or the part is permanently unbalanced.
- Dynamic balance
- The state where the mass distribution produces no net vibrating force at operating speed, including both static and couple unbalance.
You do not need every feature held to micron levels - you need the rotating features held so the residual unbalance stays inside your motor's tolerance. That is a targeting problem, not a 'make everything precise' problem, and a good shop will tell you which features actually earn the tight callout.
| Operating speed | Allowed residual unbalance | What it protects |
|---|---|---|
| 3,000-6,000 rpm (large props) | G2.5-G6.3 grade | Smooth hover, long bearing life |
| 8,000-12,000 rpm (racing/cine) | G1.0-G2.5 grade | Sharp footage, no resonance |
| 15,000+ rpm (micro/drone) | G1.0 or better | Stable flight controller, no drift |
The good news is that disciplined tight tolerance CNC makes balance boring - in the best way. Predictable bore, predictable pilot, predictable result at speed. That is what you are really buying when you pay for the tight callout.
UAV/Drone CNC precision component
How CNC Precision Machining Builds Balanced Rotors for UAV Flight
One setup, one datum, zero re-clamp drift - that is the whole game for a rotor.
A rotor hub is a disc with a central bore, a pilot, bolt bosses, and often features on both faces. Cutting it on a 3-axis machine means flipping it two or three times. Every re-clamp risks a datum shift of 0.01 to 0.03 mm, and that shift lands directly on the rotating axis where you can least afford it. CNC precision machining on a 5-axis or turn-mill center holds the part on one datum and rotates the axes around it, so the bore and the pilot can never disagree.
The single-setup rule we machine rotors by
- Rough and semi-finish the bore, pilot, and face in the first clamp so the datum is established once.
- Finish the critical diameters in the same setup before any re-fixturing.
- Cut the opposite-face features with the rotary table so the axis never releases.
- Verify the first article on a CMM against the full datum chain, not just one dimension.
- Run in-process gauging on batch parts so drift shows up before a bad lot ships.
| Process | Best rotor use | Concentricity we hold | Volume fit |
|---|---|---|---|
| Turn-mill compound | Shafts with milled flats/keyways | ±0.005 mm | Low to high |
| 5-axis milling | Complex hubs, multi-face features | ±0.008 mm | Prototype to mid |
| Swiss-type turning | Long slender rotor shafts | ±0.005 mm | Low to high |
| 3-axis (multi-setup) | Simple spacers only | ±0.02 mm per re-clamp | High only |
Because we run both 3-axis and 5-axis centers side by side on the same floor, we quote each rotor on the cheapest process that still meets the true-position callout. You should expect the same honesty from any shop you shortlist - if they route everything to the most expensive machine, ask why. Explore more UAV structural components we machine and you will see the same principle applied across arms, yokes, and motor mounts.
For rotors, process choice is a quality decision first and a cost decision second. The setup that protects your datum is the setup that protects your flight.
Rotor Materials: Where UAV/Drone CNC Parts Meet Weight and Strength
Pick the material for the rotating job it does, not for the brochure.
Rotor hubs live where stiffness-per-gram matters most, because a gram at the rotor tip changes the inertia tensor the flight controller fights every millisecond. Aerospace-grade aluminum is the default for most hubs; stainless takes the shaft where corrosion and a hard bearing seat matter; titanium steps in only when strength-to-weight or corrosion genuinely drives the design.
Aluminum hubs: 6061 vs 7075
6061-T6 covers most hubs, clamps, and plates - stable, easy to hold, and cheap to anodize. 7075-T6 steps in where yield strength matters, provided you anodize it because its corrosion resistance is lower. We machine the bore undersize by the anticipated anodize thickness so the coated bore lands at nominal - designing to the bare condition is the classic mistake that makes a motor bind.
Stainless and titanium shafts
Rotor shafts see bearing loads, finger oils, and condensation, so 304 or 316L stainless is common, and we passivate per ASTM A967 to rebuild the chromium layer that resists fingerprint corrosion. TC4 titanium is reserved for shafts where weight or corrosion resistance earns the 2-3x cycle-time premium.
| Material | Use it for | Watch out for |
|---|---|---|
| 6061-T6 | Most rotor hubs and spacers | Lower strength vs 7075 |
| 7075-T6 | High-stress hubs, yokes | Corrosion; anodize required |
| 304 / 316L stainless | Rotor shafts, bearing seats | Heavier; needs passivation |
| TC4 titanium | Weight-critical shafts | 2-3x cycle time, heat control |
Pros
- Aluminum hubs are light, cheap, and easy to hold to tolerance
- Stainless shafts resist corrosion without coating
- Titanium buys stiffness-per-gram when it matters
Cons
- 7075 needs anodize or it corrodes
- Stainless is dense - watch the tip mass
- Titanium costs more and runs hot
- Anodize thickness must be tolerated into bores
UAV/Drone CNC precision component
Custom CNC Parts vs Standard Rotors: When to Machine Your Own
A stock prop adapter is fine until your program outgrows it.
Off-the-shelf rotor hubs and prop adapters are cheap and fast - and for a prototype or a low-volume build they are usually the right answer. The moment your drone has a unique mounting pattern, a higher rpm target, a special material, or a tolerance the catalog part cannot hold, custom CNC parts stop being a luxury and become the only way to hit your spec.
Choose custom CNC parts if
- Your mounting pattern or bolt circle is not a standard size.
- Operating speed is above 12,000 rpm and balance grade must be G1.0 or better.
- You need a material the catalog does not offer (316L, TC4, hard-coat anodized 7075).
- The hub carries a sensor, a wiring path, or a feature the stock part lacks.
- You must trace every lot back to its material cert for a certified program.
Choose a standard rotor if
- Volume is low and the catalog part already meets your balance grade.
- Lead time matters more than a few grams or a custom feature.
- You are still validating the airframe and will re-specify later.
| Decision point | Standard rotor | Custom CNC parts |
|---|---|---|
| Lead time | Days | 1-2 weeks for first article |
| Balance control | As-shipped, unverified | CMM-verified, documented |
| Material choice | Limited | Any machinable alloy |
| Traceability | None | Lot-to-melt certs |
| Cost at volume | Low | Lower per unit as volume rises |
The right answer is rarely 'always custom.' It is 'custom where the spec demands it, standard where it does not' - and a supplier who tells you that is one worth keeping.
Stainless Steel Mirror Finishing for Corrosion-Proof Rotor Shafts
On a shaft, the finish is a corrosion shield, not a cosmetic touch.
Stainless steel mirror finishing is often treated as 'looks nice.' On a rotor shaft it is a durability feature. A rougher surface (higher Ra) gives corrosion a starting point and gives bearing grease a place to trap contamination. A mirror finish down to Ra 0.2 um (what we call 8K) is smoother, easier to keep clean, and far more resistant to the condensation and handling a drone sees in the field.
How we reach a true 8K mirror
- Machine the shaft to a clean baseline so polishing removes little material.
- Passivate per ASTM A967 to rebuild the chromium-oxide layer that makes stainless 'stainless'.
- Electropolish to level micro-peaks and drive Ra toward 0.2 um.
- Verify the finish with a profilometer - we do not guess the number.
- Protect the finished shaft from handling oils until assembly.
| Finish grade | Typical Ra | Where it is used on rotors |
|---|---|---|
| Standard turned | 0.8 um | Non-critical spacers |
| Fine turned | 0.4 um | Bearing seats, low-speed hubs |
| Mirror (8K) | 0.2 um | High-speed shafts, food/medical-adjacent builds |
When you specify a rotor shaft, write the Ra target on the drawing. 'Smooth' is not a tolerance; 'Ra 0.2 um max, passivated per ASTM A967' is. If you want us to review your shaft drawing, send it over for a free DFM check and we will flag the features that need the mirror callout versus the ones that do not.
UAV/Drone CNC precision component
Tight Tolerance CNC on Rotor Runout and Concentricity
Tolerance is a budget - spend it where the rotation depends on it.
Smooth rotation is set by how true the bore is to the pilot, and how perpendicular the hub face is to the axis. We concentrate the tolerance budget on those relationships and relax everything else to commercial limits so the part stays affordable. A rotor that is perfect on a feature nobody cares about but loose on the bore is the worst of both worlds.
| Feature | Tolerance we hold | Why it matters at speed |
|---|---|---|
| Bore to shaft (concentricity) | ±0.005 mm | Directly sets residual unbalance |
| Pilot diameter (h7) | ±0.008 mm | Motor registration, no wobble |
| Hub face perpendicularity | 0.01 mm | Square seating, no couple unbalance |
| Bolt-circle true position | ±0.03 mm | Even clamp load, no fretting |
| Thread form / pitch | ISO 2 / 3A | Engagement and torque consistency |
How we verify, not estimate
- CMM first article with full datum references on every new rotor design.
- In-process air or pin gauging on batch parts for the bore and pilot.
- Lot-level CMM audit so process drift shows before a bad lot ships.
- Batch traceability from raw bar to finished rotor for certified programs.
A supplier that quotes 'we are precise' without naming the feature and the number is not holding a tolerance - they are hoping. Ask for the datum chain and the CMM report, and the real shops will hand them over without hesitation.
Sourcing Custom CNC Parts: A Rotor Buyer's Checklist
Copy this and send it to every shop on your shortlist. The answers sort them fast.
Sourcing rotors is less about finding a cheap machine and more about finding a shop that understands flight-critical intent. The questions below are the ones we are happy to answer with data, and the ones that separate a real precision source from a broker with a logo.
- Can they show ISO 9001 (minimum) with real QMS records, and ISO 13485 / IATF 16949 if claimed?
- Do they machine 6061/7075 aluminum and 304/316L stainless regularly, not as a one-off?
- Can they state a runout and concentricity target and verify it with a CMM?
- Will they provide a first-article report, in-process gauging, and lot traceability?
- Do they offer passivation and electropolish in-house or via a controlled partner?
- Are tolerances quoted against your drawing, not a generic 'we are precise'?
- Can they support prototype to production without re-qualifying the process?
- Do they answer engineering questions with specifics, not sales talk?
The cheapest rotor is the one that passes qualification the first time - because the second time costs you a launch date.
UAV/Drone CNC precision component
Common Mistakes When Specifying Rotors for Drone Motors
Most rotor failures were decided at the drawing stage, not on the shop floor.
- Leaving balance as 'smooth' on the drawing, then arguing about it after shipment.
- Tolerancing an anodized bore to the bare condition, so the coated motor will not seat.
- Chasing the lowest blank price and paying for it in rework and bearing returns.
- Skipping first-article inspection to 'save time' - it is the cheapest insurance you have.
- Forgetting traceability, so a single field complaint becomes a full recall.
- Drawing R0 internal corners on pockets; end mills leave a radius, so specify the real one.
None of these mistakes are technical. They are habits, and the disciplined shop you choose should make the right habit the easy default. Pick the partner whose strengths match the stage you are actually in - and ask how they handle the next stage before you need it.
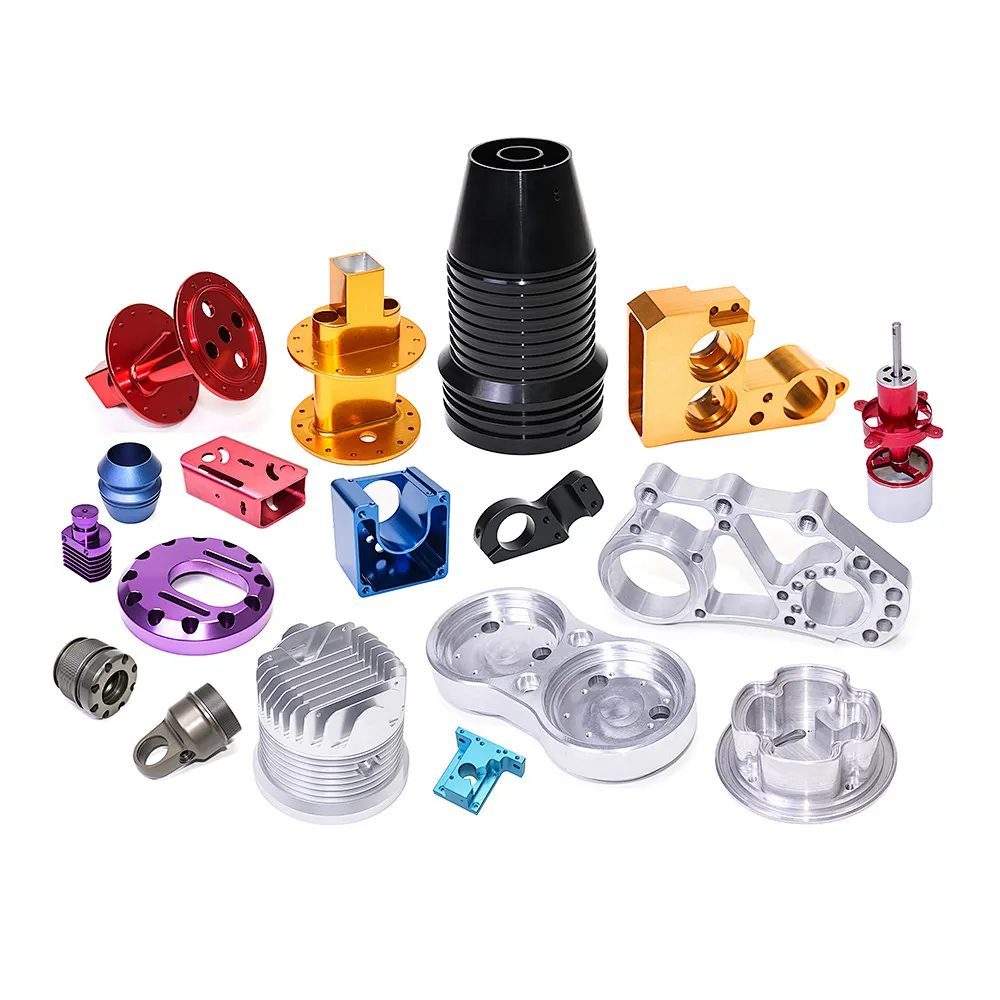
UAV/Drone CNC precision component
UAV/Drone CNC precision component
UAV/Drone CNC precision component
UAV/Drone CNC precision component
FAQ: rotors & UAV/Drone Buyer Questions
A: For most multirotor hubs we hold bore-to-shaft concentricity to ±0.005 mm and the pilot to ±0.008 mm, verified by CMM. At 8,000-12,000 rpm that keeps residual unbalance inside a G1.0-G2.5 grade. Write the number on the drawing rather than 'smooth' so it is a controllable requirement.
A: Yes. We machine 304 and 316L stainless rotor shafts and passivate per ASTM A967, then electropolish to a mirror Ra 0.2 um (8K) when the application calls for it. Passivation rebuilds the chromium layer that resists field corrosion; we verify the finish with a profilometer rather than estimating it.
A: Balance starts with the machining: we hold the bore, pilot, and face on one datum in a single setup so concentricity is built in, not chased. For certified programs we verify the first article on a CMM and run lot-level audits, and we treat balance grade (G1.0 to G6.3) as a function of your operating speed, not a fixed number.
A: Only when stiffness-to-weight or corrosion resistance genuinely drives the design. Titanium's higher modulus lets you use less material for a bending-limited shaft, but cycle time runs 2-3x aluminum. For most hubs, 6061 or 7075 aluminum is the better value; we steer customers to TC4 only when the math supports the premium.
A: Yes. We run first-article inspection on new rotor designs, support low-volume custom batches, and scale to monthly volume of 500,000 parts while keeping the same documented process and lot traceability - so a rotor program grows with us without re-qualifying the source.
A: Expect a material mill certificate tied to the heat lot, a CMM first-article report with full datum references, in-process gauging records, passivation or finish reports, and a Certificate of Conformance. Any flight-critical rotor order should be traceable from raw bar to finished part.
Sending us your rotor hub or shaft drawing gets you a free DFM review - we will flag the features that should move to 5-axis or turn-mill, the tolerances that are costing you money, and the finish call between a standard turn and an 8K mirror. Reach out and let's cut the first article.
Request a Free CNC Quote