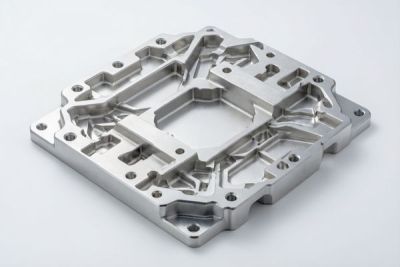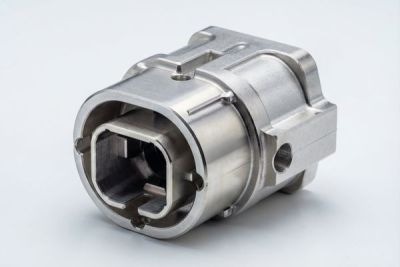
CNC end-effector parts: Machining & Tolerances for Medical Applications
If you are buying end-effector parts for Medical applications, the part that looks fine on a drawing can still fail in the field — at the worst moment. specifying end-effector parts that must hold tight tolerances and survive real operating loads is exactly where most sourcing mistakes happen, and where a disciplined supplier earns its fee.
At LusterControl we have spent 15 years machining stainless and alloy precision parts on 60 CNC machines across a 4,000 m² plant. This guide walks through what a Medical buyer should actually check before releasing a PO — written the way an engineer talks to another engineer, with numbers you can verify.
Table of Contents
- 1. Why End-Effector Parts Matter for Medical Buyers
- 2. How Medical Cnc Parts Is Machined at LusterControl
- 3. Tolerances and Inspection on Cnc Precision Machining
- 4. Material and Surface Finish for Tight Tolerance Cnc
- 5. Key Terms Every Custom Cnc Parts Buyer Should Know
- 6. Comparing Suppliers for Stainless Steel Mirror Finishing
- 7. Buyer's Checklist for End-Effector Parts
- 8. Cost and Lead Time for Medical Cnc Parts
- 9. Quality Process Framework Behind Cnc Precision Machining
- 10. A Real Tight Tolerance Cnc Program We Shipped
- 11. Protecting Your Design When You Source Custom Cnc Parts
- 12. More Stainless Steel Mirror Finishing Reading for Medical Buyers
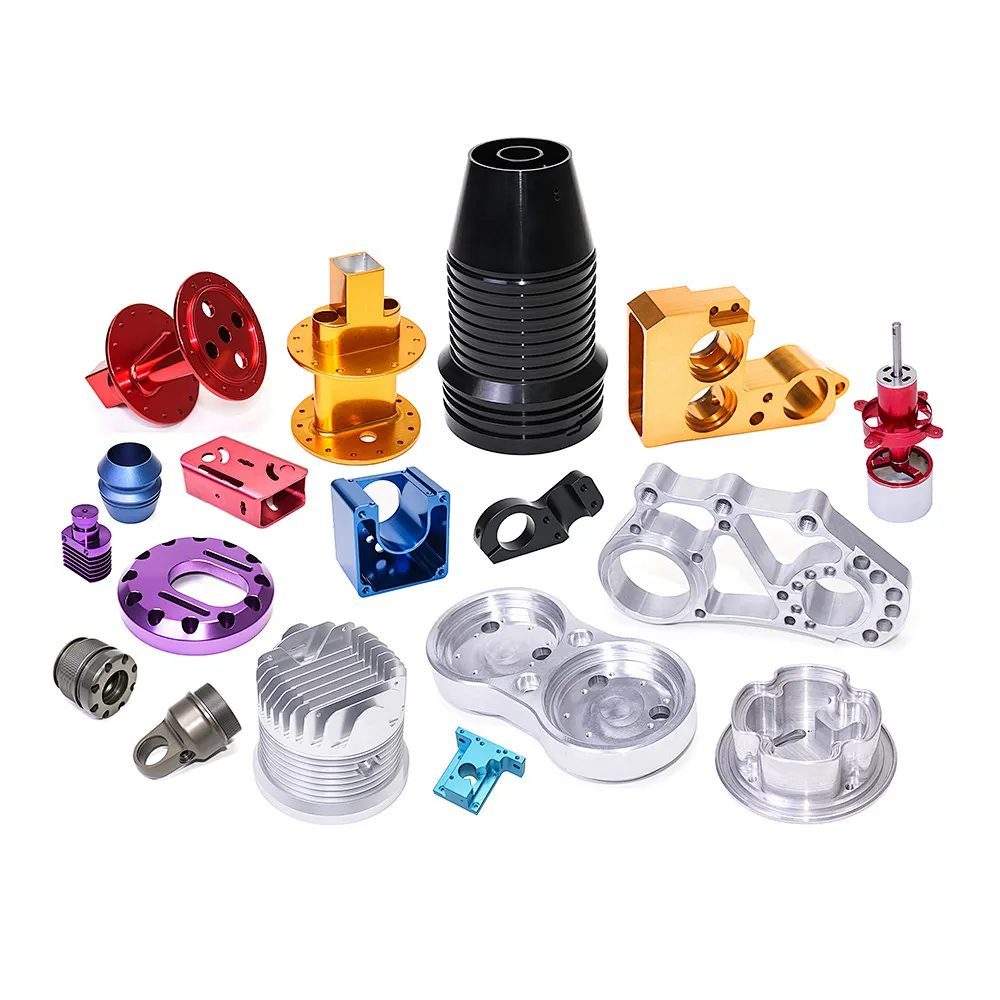
Medical CNC precision component
Why End-Effector Parts Matter for Medical Buyers
A end-effector part is rarely the hero of your assembly, but it is usually the part that determines whether the whole product passes qualification. For Medical programs, end-effector parts sit at the intersection of fit, function and cost.
The buyer's real risk
Miss the tolerance and you get scrap, rework loops and a delayed launch. Pick the wrong process and you pay for capability you do not need — or worse, you under-buy and the part cannot hold up. That is why End-Effector Parts deserve a second look before PO.
Medical CNC precision component
How Medical Cnc Parts Is Machined at LusterControl
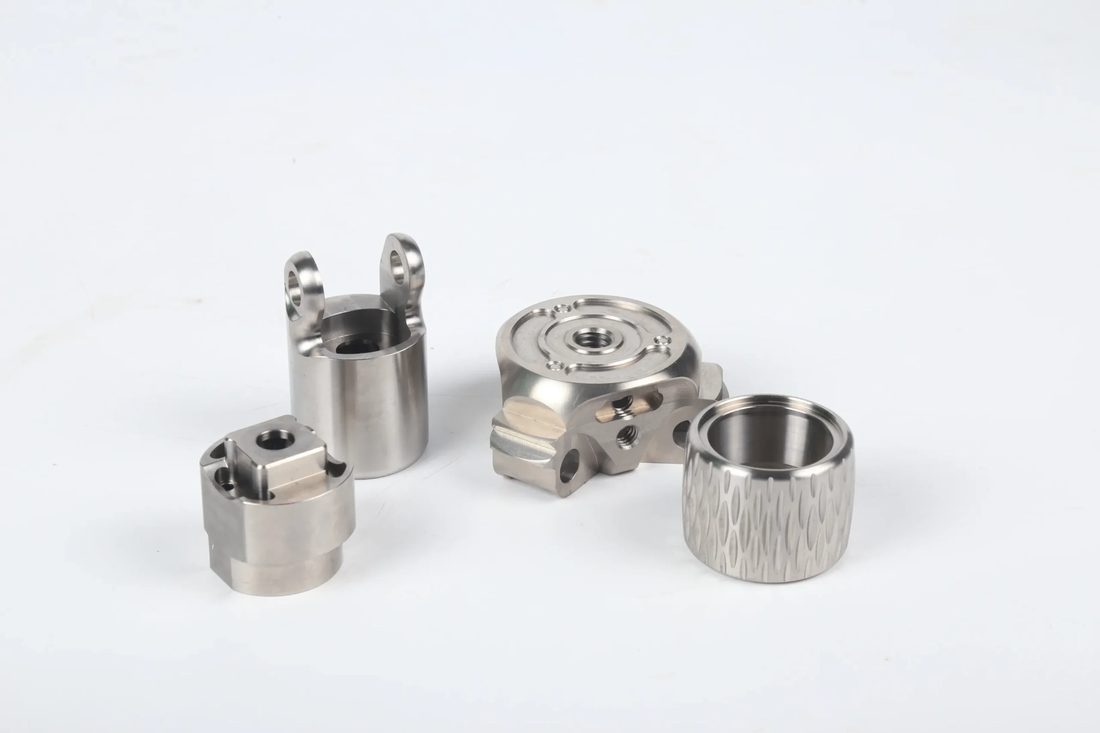
Most end-effector parts are produced on a combination of turning and milling. LusterControl runs 60 CNC machines covering turn-mill composite, 5-axis, mirror/electropolishing, Swiss-type turning, lot traceability — so a part that needs multi-side features is done in fewer setups, which means less stack-up error.
Choosing the right process
- 3-axis milling for simple profiles — cheapest, fast.
- Turn-mill composite for round parts with milled features — one chucking, better concentricity.
- 5-axis when you need deep cavities or tight angular features without re-fixturing.
- Swiss-type turning for long, slender, high-volume shafts where runout matters.
Tolerances and Inspection on Cnc Precision Machining
LusterControl holds ±0.005 mm on stainless mirror-finished parts. But a number on a drawing means nothing without proof, so every high-precision item ships with CMM first-article data and ISO 9001 certified, ISO 13485 completed, IATF 16949 applying controls behind it.
| What you should request | Why it matters |
|---|---|
| First-article CMM report | Measured data, not a promise — your baseline for incoming inspection. |
| Lot traceability | Every batch ties back to material and machine for field failures. |
| 100% final inspection plan | Incoming, in-process and final checks before shipment. |
| Material cert (MTR) | Confirms the alloy is what the print calls for. |
Medical CNC precision component
Material and Surface Finish for Tight Tolerance Cnc
For end-effector parts the alloy decides corrosion resistance, hardness and cleanability. LusterControl machines 304, 316/316L, 303, 440C and 630 (17-4PH) stainless.
- 304 — general corrosion resistance, the default workhorse.
- 316 / 316L — chloride, marine and medical exposure.
- 440C — hardenable, wear-resistant moving parts.
- 630 (17-4PH) — high strength with good corrosion resistance.
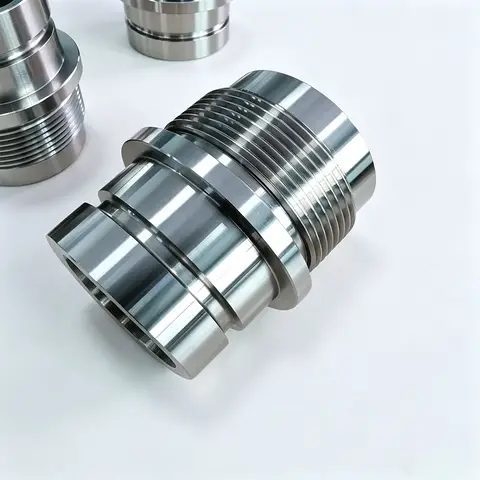
Surface matters too. LusterControl reaches Ra 0.6 μm (standard), up to 8K mirror Ra 0.2 μm — the difference between a seal that holds and one that weeps, or a part that sterilizes clean versus one that traps residue. We do electropolishing in-house, so lead time stays short.
Key Terms Every Custom Cnc Parts Buyer Should Know
Before you compare quotes on end-effector parts, a few terms decide whether the number on the quote means what you think. Here is the plain-English version a Medical buyer needs.
- Ra (roughness average)
- Surface roughness in micrometres. Lower Ra = smoother. LusterControl holds Ra 0.6 μm (standard), up to 8K mirror Ra 0.2 μm on stainless mirror parts - the difference between a seal that holds and one that weeps.
- Tolerance
- The allowed deviation from the drawing dimension. We hold ±0.005 mm on stainless; tighter than needed just adds cost, looser than needed adds scrap risk.
- Electropolishing
- An electrochemical finish that smooths and passivates stainless in-house at LusterControl - smoother, cleaner, more corrosion-resistant, and it keeps lead time short.
- SPC / CPK
- Statistical process control and process-capability index. CPK > 1.33 on critical dims means the process is stable, not lucky - the proof your audit trail needs.
- Lot traceability
- Every batch ties back to material cert and machine. If a part fails in the field, root cause is fast instead of a finger-pointing exercise.
Medical CNC precision component
Comparing Suppliers for Stainless Steel Mirror Finishing
Not all shops that quote end-effector parts are equal. The tables below are the quick lens a Medical buyer should use when the prices look similar but the risk does not.
| Supplier model | Best for | Watch-out |
|---|---|---|
| Trading company | White-label, re-export convenience | You pay a margin and lose traceability to the source. |
| Job shop (no finishing) | Simple one-off parts | You manage plating/polish handoffs and lead time. |
| One-stop source factory (LusterControl) | Turn-mill-finish-assembly in one PO | Confirm certs match your industry upfront. |
Capability vs your actual need
| Capability | What it proves to a buyer | Minimum we recommend |
|---|---|---|
| In-house finishing | Shorter lead time, no handoffs | Electropolish + anodize in-house |
| CMM first-article data | Measured proof, not a promise | On every new print |
| SPC / CPK on critical dims | Stable process, not spot checks | CPK > 1.33 on special chars |
| Lot traceability | Fast root cause on field failures | Full batch record |
| Material cert (MTR) | Alloy matches the print | Per lot |
Choose a one-stop source if — choose a split shop if
Pros
- Pick one-stop (LusterControl) if you want one PO, one quality record and one accountable partner from raw bar to finished, inspected part.
- Pick it if your part needs turning + milling + finish in one flow and you cannot afford handoff drift.
Cons
- Pick a split shop only if a single specialist is clearly cheaper for a simple, low-risk part.
- Accept that you own the handoffs, the freight between shops and the final quality record.
Buyer's Checklist for End-Effector Parts
Before you release a PO for end-effector parts, run this list. It takes five minutes and removes most of the risk on a Medical program.
- Drawing is 2D + 3D and the real annual volume is stated.
- Tolerance is called out (not just 'as per drawing').
- Material grade and finish (Ra) are specified.
- Inspection plan and AQL are agreed up front.
- Material cert + lot traceability are in the contract.
- Free DFM review is done before PO to avoid rework loops.
Medical CNC precision component
Cost and Lead Time for Medical Cnc Parts
Unit price on end-effector parts is material + machine time + finishing + inspection + packaging. LusterControl prices transparently so you can trade off tolerance, finish and volume instead of guessing.
- Send a clean drawing and the real annual volume.
- Confirm material early so we reserve stock.
- Book a free DFM review before PO to relax non-critical tolerances.
- Bundle volume for a sharper unit rate.
Quality Process Framework Behind Cnc Precision Machining
Buyers rarely see the factory floor, so we make the quality system explicit. For end-effector parts LusterControl runs a staged control chain — the discipline that lets us hold ±0.005 mm and ship 500,000 parts/month without a recall.
- DFM review before PO — relax non-critical tolerances, pick the right process.
- Incoming material check — mill test report and positive material ID on every lot.
- First-article CMM — measured data, not a promise, as your incoming baseline.
- In-process patrol — SPC / CPK on critical dimensions so drift is caught early.
- Final FQC / OQC — AQL-based full or sampled inspection before shipment.
- Lot traceability — every batch ties back to material and machine for field failures.
| Checkpoint | What the buyer gains |
|---|---|
| DFM | Fewer rework loops, lower unit price. |
| First-article CMM | A reference you can defend in an audit. |
| SPC / CPK | Stable process, not luck, on critical dims. |
| Lot traceability | Fast root cause if a part fails in the field. |
Medical CNC precision component
A Real Tight Tolerance Cnc Program We Shipped
Numbers build trust more than adjectives. From our Dongguan plant: a UAV structural order won at RMB 1.2 million on tight concentricity; mirror-finished coffee-machine parts supplied to De'Longhi, Donlim and Breville-grade programs at 8K Ra 0.2 µm; and medical handles held to burr-free, biocompatible specs.
Protecting Your Design When You Source Custom Cnc Parts
For Medical buyers - especially brand owners and R&D teams - the bigger risk than a bad part is a leaked design. A drawing sent to three shops is a design in three places. When you send LusterControl your end-effector parts, protection is part of the service, not an extra.
- We work under customer NDA: your drawings and specs stay confidential to the program.
- CAD files are handled on controlled access - no open forwarding, no re-use for other customers.
- Prototype parts are packed and shipped discretely for international delivery.
- Your IP stays yours: we manufacture to your print; we do not own or resell your design.
Medical CNC precision component
More Stainless Steel Mirror Finishing Reading for Medical Buyers
If you are scoping end-effector parts for Medical, these pages help you go further — from a free DFM review to the team behind the parts.
- Request a free DFM review — marked-up drawing, recommended process and price range.
- Meet the LusterControl engineering team and our certifications.
- Read more buyer guides on tolerances, materials and supplier checks.
- LusterControl homepage — capacities, processes and industries served.
Medical CNC precision component
Medical CNC precision component
FAQ: end-effector parts & Medical Buyer Questions
A: We hold ±0.005 mm on stainless mirror-finished parts, with CMM first-article data and lot traceability for every batch. For a Medical buyer that means the fit and scrap risk are designed out before cutting.
A: 304 for general use, 316/316L for chloride or medical/marine exposure, 440C when you need hardenable wear resistance. We machine 304, 316, 303, 440C and 630 (17-4PH), each with a material cert.
A: Yes. LusterControl is a Dongguan source factory: turning, milling, 5-axis, mirror/electropolishing, anodize and assembly are all in-house across 4,000 m² plant with 60 CNC machines — one PO, one quality record.
A: ISO 9001 certified, ISO 13485 completed, IATF 16949 applying. If your part is a regulated medical device, ISO 13485 is the baseline buyers must see, and we can show the certificate plus the audit trail.
A: We target a 7-day first article from drawing to sample for many programs and accept low-MOQ or single-piece prototypes, scaling to 500,000 parts/month in volume. Book a free DFM review before PO to shorten it.
Ready to move your program forward? Send us your drawing and we will return a free DFM review with the real achievable tolerance, lead time and unit-price curve for your part — no commitment required.
Request a Free CNC Quote