Choosing a CNC Shop for Surgical Instruments & Tweezers: 2026 Buyer's Guide
If you are sourcing surgical tweezers or forceps, the features that decide whether a lot passes are almost always the ones you cannot see. A tying forceps whose tips close with a 0.03 mm gap will drop a suture under tension. A pivot bore that is 0.01 mm off-center makes the jaw bind. A surface that looks clean but was never passivated will pit after one autoclave cycle. The shop you pick is the difference between a quiet production line and a recall.
This guide is written for the procurement engineer, the contract manufacturer, and the medtech founder who needs stainless steel instrument bodies machined to spec and documented to death. We walk through the tolerances that actually matter on tweezers and forceps, why mirror finishing is a hygiene requirement and not a cosmetic upgrade, what ISO 13485 machining discipline should look like on your supplier's floor, and the exact documents you should demand before you release a purchase order.
For context, we are LusterControl - the manufacturing brand of Dongguan Licun Technology Co., Ltd., a Dongguan source factory running 60+ CNC machines on a 4,000 sqm floor since 2015. We machine precision stainless components as a contract partner under an ISO 13485 quality system; we are not a finished-device brand, and this guide is about how to vet a shop like ours, not about selling you one.
Table of Contents
- 1. Why Surgical Instruments Demand Tight Tolerance CNC Work
- 2. Stainless Steel Mirror Finishing on Tweezers and Forceps
- 3. What ISO 13485 Machining Means for Your Tweezers
- 4. A Buyer's Checklist for CNC Precision Machining Suppliers
- 5. How Medical Device Components Are Held to Micron Tolerances
- 6. Surgical Instruments: Common Sourcing Mistakes to Avoid
- 7. CNC Precision Machining vs Swiss Turning for Forceps
- 8. Tight Tolerance CNC Inspection for Surgical Instruments
- 9. Medical Device Components Need Full Material Traceability
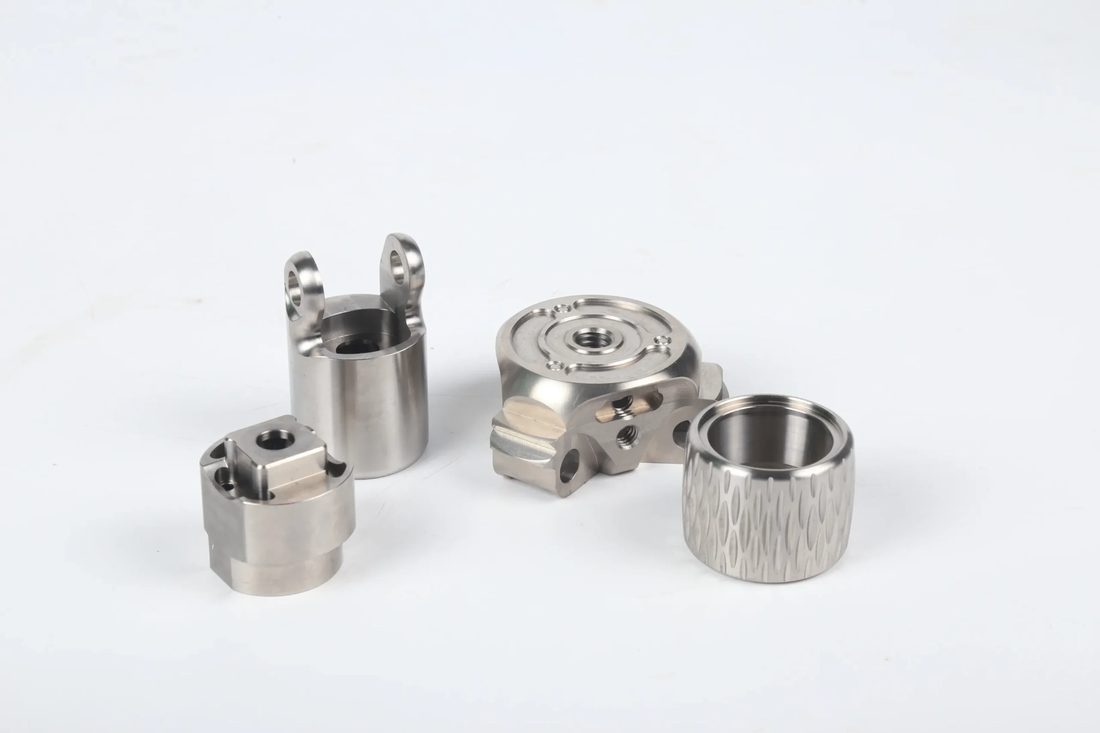
Medical CNC precision component
Why Surgical Instruments Demand Tight Tolerance CNC Work
Tweezers and forceps live or die by the features you cannot see.
A surgical instrument is a precision mechanism squeezed into a few grams of stainless steel. The working tips, the pivot, and the jaw faces are all loaded features, and each one has a tolerance that, if missed, turns a reliable tool into a liability. When you source these parts, 'close enough' is not a category that exists.
On a stainless part with a 2-4 mm cross-section, a competent shop holds +/-0.005 mm on the features that matter and +/-0.01 to 0.02 mm on the ones that don't. The discipline is knowing which is which - and proving it with measurement data, not a promise. That is the heart of what tight tolerance CNC brings to instrument manufacturing.
What 'tight tolerance' actually means for tweezers
- True position
- How far a feature's actual location sits from its designed location, measured as a diameter. On forceps pivot bores we hold this to 0.01 mm.
- Concentricity
- How well two cylindrical features share a common axis. A tying forceps jaw must stay concentric to its pivot or it binds.
- Mirror finish (Ra)
- Average surface roughness in micrometers. Standard mirror is Ra 0.6 um; our top 8K mirror reaches Ra 0.2 um.
Three features that decide whether a forceps works
- Tip closing gap - the two jaws must meet with no daylight when closed; a 0.02 mm gap is already a functional failure.
- Pivot bore concentricity - the hinge must run true or the jaw drags and wears unevenly.
- Jaw face flatness - gripping surfaces need consistent contact, not a rocking edge.
| Feature | Typical spec | Why it matters | Our capability |
|---|---|---|---|
| Tip closing gap | <= 0.02 mm | Drops or fails to hold suture | Held via single-setup turn-mill |
| Pivot bore position | 0.01 mm TIR | Jaw drag and uneven wear | +/-0.005 mm on 60+ CNC |
| Jaw face flatness | 0.01 mm | Consistent grip, no rocking | Lapped + verified on CMM |
| Overall length | +/-0.05 mm | Fit with handle and packaging | Routine on 5-axis centers |
If you want to see how we handle micron-level work across other programs, our write-ups on medical device components cover the process chain in detail. The same discipline that lands a pivot bore on-center is what protects your lot yield.
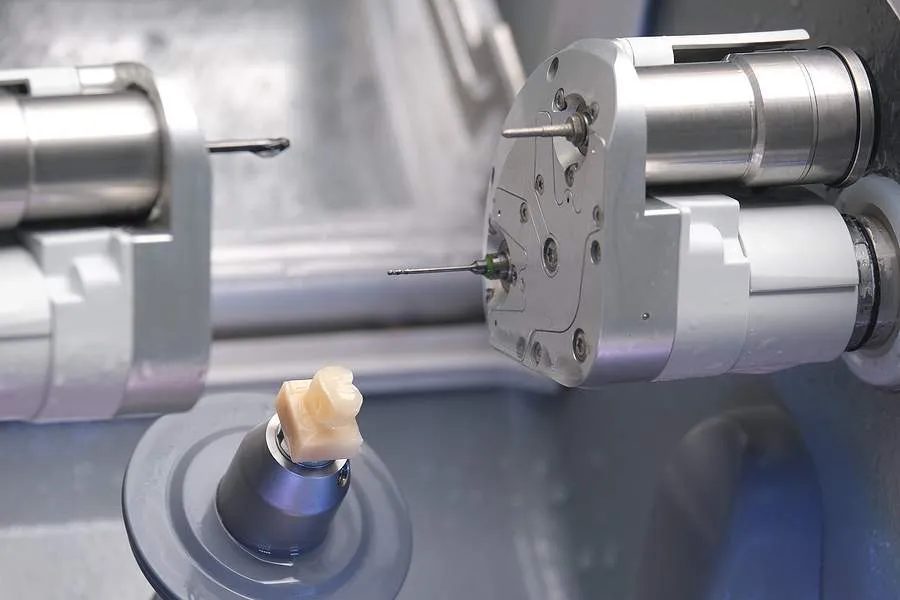
Medical CNC precision component
Stainless Steel Mirror Finishing on Tweezers and Forceps
Finish is not cosmetics - on a surgical tool it is hygiene and feel.
A rough surface on a surgical instrument does three bad things at once. It traps biofilm that survives sterilization, it corrodes faster at the peaks and valleys, and it feels wrong in a surgeon's hand. Mirror finishing removes that roughness, and on instruments it is a functional specification, not a polish you add for looks.
Stainless steel mirror finishing at LusterControl runs from a standard Ra 0.6 um mirror up to an 8K mirror at Ra 0.2 um. The 8K level is what premium instrument brands ask for on visible and contact surfaces, because it leaves almost no micro-crevice for contamination.
| Finish tier | Roughness (Ra) | Typical use | Cost factor |
|---|---|---|---|
| As-machined | 1.6 um | Internal non-contact | Baseline |
| Standard mirror | 0.6 um | Jaw, body surfaces | 1.3x |
| 8K mirror | 0.2 um | Tips, contact faces | 1.8x |
How we reach Ra 0.2 um on stainless
- Precision machine the geometry so the stock left for finishing is minimal and uniform.
- Mechanical polish in graduated steps to remove tool marks.
- Electropolish and passivate per ASTM A967 to close the grain and restore corrosion resistance.
- Verify with a surface profilometer and record the Ra value on the inspection report.
We publish our process and facility facts on our about page so buyers can verify the floor, the machine count, and the quality system before they send a drawing.
What ISO 13485 Machining Means for Your Tweezers
A certificate is a promise; the system behind it is what protects your lot.
ISO 13485 is the quality management system standard written specifically for medical device manufacturing. When a machine shop says it runs ISO 13485 machining, what you are really buying is documented control: traceable material, validated processes, calibrated measurement, and records that survive an audit years later. That is what lets your own regulatory file stand up.
LusterControl has completed ISO 13485 and holds ISO 9001; IATF 16949 is in application. We are a contract precision-machining source, not a finished-device maker, so our role is to deliver documented, traceable instrument components - the brand owner owns the final device clearance. Being honest about that line is part of the trust.
| Standard | Our status | What it controls for your parts |
|---|---|---|
| ISO 9001 | Certified | General quality system, non-conformance handling |
| ISO 13485 | Completed | Medical-device QMS: traceability, risk control, records |
| IATF 16949 | In application | Automotive-grade process discipline (being adopted) |
| ASTM A967 | Applied | Passivation of stainless corrosion-resistant parts |
What you should ask for at audit
- Lot-level material traceability from mill cert to finished part
- First-article inspection (FAI) report with CMM data for the first lot
- In-process SPC or CPK evidence on critical features
- Calibrated measurement equipment with current certificates
- A documented corrective-action path when a dimension drifts
Medical CNC precision component
A Buyer's Checklist for CNC Precision Machining Suppliers
Before you release a PO, your supplier should hand you these.
The fastest way to separate a serious CNC precision machining partner from a job shop that happens to own a lathe is the document package. A shop that can produce the list below without hesitation is one you can put on a qualified-vendor list. One that stalls is one you qualify at your own risk.
The seven documents to demand
- Valid ISO 13485 and ISO 9001 certificates whose scope covers machined parts
- Material mill certificate (EN 10204 3.1) showing heat and lot number
- First-article inspection report with CMM measurements for the first lot
- Documented passivation per ASTM A967 on all 300-series stainless
- Lot traceability linking raw bar to finished part and inspection record
- DFM feedback on your drawing before quote - not a silent yes to every tolerance
- A realistic lead-time curve based on real loaded capacity, not a flat promise
Red flags that mean walk away
- Refuses or 'lost' the mill cert - you have no idea what steel you received
- No measurement room or outsourced-only inspection with no data returned
- Won't produce a first-article report and expects you to find issues in production
- Vague or missing lot traceability in the purchase order terms
- Agrees to every tolerance without a DFM note - they are not engineering your part
If your current supplier cannot clear this list, start a parallel qualification. You can open a conversation and send a drawing through our inquiry page for a free DFM review before you commit volume.
How Medical Device Components Are Held to Micron Tolerances
Micron control is a process chain, not a single machine.
Buyers often ask 'what machine holds the tightest tolerance?' The honest answer is that tolerance is held by a chain, and the weakest link sets the result. A perfect 5-axis center cannot save a part if the bar stock was never verified or the final inspection was skipped.
The chain from bar stock to finished part
- Incoming inspection - verify the mill cert and check the bar for straightness and hardness
- Probing setup - touch-off and in-machine probing so the datum is the machine, not a hand gauge
- In-process control - SPC on critical features, with tool-wear compensation between parts
- Final verification - CMM for position and form, profilometer for Ra on finished surfaces
- Clean, documented pack - lot-labeled, kept separate from mixed inventory
| Process | Best tolerance | When to choose it | Relative cost |
|---|---|---|---|
| Turn-mill compound | +/-0.005 mm | Complex instrument bodies, one setup | Mid |
| 5-axis CNC | +/-0.005 mm | Multi-angle features, stiff thin walls | Mid-high |
| Swiss-type turning | +/-0.008 mm | Long slender shafts, high volume | Mid |
| Centerless grind | +/-0.002 mm | Cylindrical diameters only | High |
Medical CNC precision component
Surgical Instruments: Common Sourcing Mistakes to Avoid
Most rejected lots trace back to one of these five errors.
- Over-specifying a mirror finish where a brushed Ra 0.4 um would do - you pay for polish you cannot use
- Forgetting passivation - stainless still rusts in autoclave cycles without ASTM A967 treatment
- Leaving lot traceability out of the purchase order - then a heat-lot problem becomes a full recall
- Choosing a supplier on price alone and ignoring first-article evidence
- Ignoring DFM - shipping a drawing that fights the machining process instead of fitting it
Mistake number one in detail: over-specifying finish
A visible body surface reads fine at Ra 0.6 um. Specifying Ra 0.2 um 8K mirror on the entire part doubles finishing cost for zero functional gain on non-contact areas. The right move is to call out 8K only on tips and grip faces and standard mirror elsewhere - a disciplined shop will tell you this on the DFM review.
A related trap is assuming any stainless is interchangeable. Grade choice drives both machinability and corrosion behavior, which is the next thing a good buyer checks before release.
CNC Precision Machining vs Swiss Turning for Forceps
Same steel, two very different shops - pick on geometry, not habit.
Forceps and tweezers split neatly between two process families. Parts that are mostly turned shafts with a few milled features favor Swiss-type turning. Parts with complex milled jaws, thin walls, or multi-angle features favor CNC precision machining. Knowing which your design needs keeps cost and lead time honest.
| Factor | CNC precision machining | Swiss-type turning |
|---|---|---|
| Best geometry | Milled jaws, thin walls, angled features | Long slender shafts, diameters < 20 mm |
| Typical tolerance | +/-0.005 mm | +/-0.008 mm |
| Volume sweet spot | Low-to-mid, high mix | Mid-to-high, repeat runs |
| Setup style | Turn-mill or 5-axis, single clamp | Sliding headstock, bar fed |
| Our floor | Mixed 3/5-axis + turn-mill | Swiss-type and fixed-head lathes |
Choose CNC precision machining if
- Your forceps body has milled jaw profiles or thin-walled cradles
- You need 5-axis access to angled features in one setup
- Your run is low volume with several variants sharing a fixture family
Choose Swiss turning if
- The part is a long, slender shaft or pin under 20 mm diameter
- You need thousands of identical pieces with tight diameter control
- Diameter concentricity matters more than milled complexity
Medical CNC precision component
Tight Tolerance CNC Inspection for Surgical Instruments
You cannot ship what you cannot measure - and auditors will ask for the data.
On surgical instruments, inspection is not a gate at the end; it is woven through the run. Tight tolerance CNC only means something if the numbers are captured and retrievable. A shop that 'eyeballs it on a gauge' cannot defend your lot in an audit, and you inherit that gap.
What good inspection looks like
- Coordinate measuring machine (CMM) for position, form, and true position
- Optical comparator for profile and tip geometry
- Surface profilometer for Ra on mirror-finished faces
- Calibrated hand tools, all with current calibration certificates
- Recorded data tied to the lot and retrievable years later
| Feature | Instrument | Acceptance we hold |
|---|---|---|
| Pivot bore position | CMM | 0.01 mm TIR |
| Tip closing gap | Optical comparator | <= 0.02 mm |
| Jaw face flatness | CMM + surface plate | 0.01 mm |
| Mirror Ra | Profilometer | 0.2-0.6 um per tier |
You can read more about our floor and quality setup on the about page before you schedule a supplier audit.
Medical Device Components Need Full Material Traceability
In medtech, 'where did this bar come from?' is never optional.
Traceability is the quiet requirement that separates a medical supply chain from a hobby shop. When a heat lot of stainless shows a metallurgical defect, you need to know exactly which finished parts came from it - fast. That means the mill cert, the incoming log, the job, the operator, and the inspection record all link to one lot number.
The traceability chain we maintain
- Mill certificate captured at goods-in, with heat and lot number logged
- Incoming inspection tied to that lot before any cutting starts
- Machine and job ID recorded for every production run
- Operator and inspection record attached to the lot file
- Pack label carrying the lot number so it follows the part to your dock
When you are ready to qualify a partner, send a drawing and we will return a DFM note plus the document package above. Our inquiry page is the fastest way to start.
Medical CNC precision component
Medical CNC precision component
Medical CNC precision component
Medical CNC precision component
FAQ: medical device components & Medical Buyer Questions
A: A competent shop holds +/-0.005 mm on critical stainless features such as pivot bores and +/-0.01 to 0.02 mm on non-critical ones. Tip closing gap should be 0.02 mm or better, verified on an optical comparator.
A: ISO 13485 governs the quality system - traceability, risk control, and records - not the finished device. A machine shop running ISO 13485 (like LusterControl, which has completed it and holds ISO 9001) delivers documented, traceable components; final device regulatory clearance remains the brand owner's responsibility.
A: 316L is the default for surgical instruments because of its corrosion resistance and weldability. 304 is acceptable for lower-risk tools. 17-4PH is chosen when higher strength or hardness is needed but it is less corrosion-resistant and harder to machine; let DFM decide rather than defaulting.
A: Require an EN 10204 3.1 mill certificate with heat and lot number, an incoming inspection log that captures it, and a pack label carrying the same lot number. Ask to see a sample lot file before release; if the supplier cannot produce one, do not qualify them.
A: Choose Swiss-type turning for long slender shafts under 20 mm diameter and high volumes. Choose CNC precision machining or turn-mill compound for instrument bodies with milled jaws, thin walls, or multi-angle features. Many forceps are best on turn-mill because the shaft and jaw are made in one setup.
A: Contact and tip surfaces typically need an 8K mirror at Ra 0.2 um; visible body surfaces are fine at standard mirror Ra 0.6 um. Specifying 8K across the whole part adds cost with no functional gain on non-contact areas, so call it out only where it matters.
Ready to qualify a machining partner for your surgical tweezers or forceps? Send us your drawing for a free DFM review and we will return tolerances, finish tiers, and the full document package - mill cert, FAI, passivation, and lot traceability - before you commit a single unit.
Request a Free CNC Quote