EV Battery Liquid-Cooling Connectors: Seal Face Ra & Torque Spec (2026 Guide)
A single weeping fitting inside an EV battery pack is not a cosmetic defect. It is a slow loss of coolant, a rising cell temperature, a derate, and eventually a warranty conversation nobody in your engineering chain wants to have. You can specification-sheet a battery liquid-cooling connector to death and still miss the two things that actually decide whether it stays dry: the roughness and geometry of the seal face, and the torque that preloads it. Get either one wrong and the joint passes a bench check and fails after a thermal cycle.
This guide is written for the engineers and buyers who have to sign off that joint before a purchase order goes out — not for a catalogue. We walk through how a battery liquid-cooling connector actually seals, how the seal face is generated at the machine, why a torque spec is meaningless without a controlled surface under it, and how pressure-test traceability turns a one-time pass into a defensible production record. We also give you a buyer's checklist and the common drawing mistakes we see before a chip is cut.
We are LusterControl, the brand of Dongguan Licun Technology Co., Ltd. Since 2015 we have spent fifteen years on CNC stainless-steel mirror turning: 60 CNC machines, a 4,000 m² plant after the 2026 expansion, and a general monthly output around 500,000 parts. Every number in this guide comes off our own floor. Read it as a shop-floor conversation about battery liquid-cooling connectors, with the trade-offs left in.
Table of Contents
- 1. What Battery Liquid-Cooling Connectors Actually Decide in a Pack
- 2. How a Battery Liquid-Cooling Connector Seals: The Core Mechanism
- 3. Liquid-Cooling Coupler Machining: Building the Seal Face
- 4. Turn-Mill Composite: One Clamping from Bar to Seal Face
- 5. Tight Tolerance CNC: Holding the Mating Interface
- 6. CNC Precision Machining and the Torque Spec You Can Trust
- 7. CNC Precision Machining: Pressure-Test Traceability
- 8. Battery Liquid-Cooling Connector Seal Face vs Torque: Hard-Number Comparison
- 9. Which Battery Liquid-Cooling Connectors Fit Your Pack?
- 10. Buyer's Checklist for Liquid-Cooling Coupler Machining
- 11. Common Mistakes in Tight Tolerance CNC of Battery Couplers
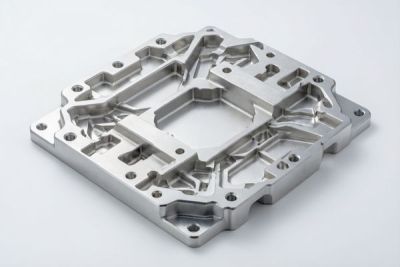
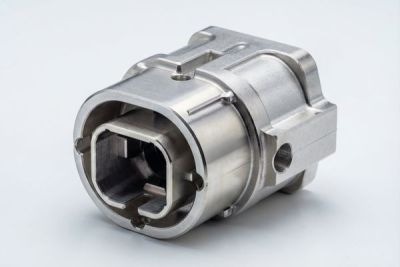
New Energy Vehicles (Battery Thermal Management) CNC precision component
What Battery Liquid-Cooling Connectors Actually Decide in a Pack
Before you compare fittings, be clear on what the joint is being asked to do.
- Battery liquid-cooling connector
- The threaded or quick-connect interface that joins a pack's cooling plate, manifold, or coolant line to the vehicle loop. Its job is to pass coolant and hold pressure for the life of the pack, through thermal cycling, vibration, and service events.
- Seal face
- The machined surface — a cone, flat, or O-ring seat — against which the sealing element compresses. On a coupler this surface, not the outside diameter, sets leak performance.
- Torque spec
- The tightening torque specified for the joint. Torque is a proxy for clamp load: it is what turns a handled wrench into a repeatable preload on the seal. A torque value only means something if the surface under it is controlled.
A battery liquid-cooling connector is a small part carrying an outsized consequence. It sits at the boundary between a pumped coolant loop and a sealed pack. It sees pressure cycling, the expansion and contraction of a heating pack, road vibration, and — at service — a technician tightening it in a confined space with limited feel. A poor joint rarely fails dramatically. It weeps, loses coolant slowly, and becomes an intermittent thermal fault that looks like a sensor problem until somebody finds the damp fitting.
Three jobs one fitting must perform at once
- Seal. Hold coolant at working pressure across temperature swings and vibration without depending on thread sealant or assembly luck.
- Align. Guide the mating half into the seat so an O-ring is not cut on the thread entry and a sealing cone is not scored on the way in.
- Survive. Resist the coolant chemistry, tolerate repeated service mating cycles, and stay dimensionally stable after cleaning and passivation.
Why the seal face, not the threads, decides the leak result
Buyers routinely specify the thread class and overall length down to the last decimal and leave the seal face under a general tolerance. That is backwards. A body dimension can be a few tenths off and still assemble. The seal face cannot. If it is out of flatness, if the bore carries a directional tool mark that wicks coolant, or if the cone and the thread were cut in two separate setups, you get a part that passes a visual check and fails a pressure-decay test.
We keep returning to this point in our technical guides on liquid-cooling and fluid-control parts: the functional surface is usually the last thing a general job shop protects, and the first thing you should specify.
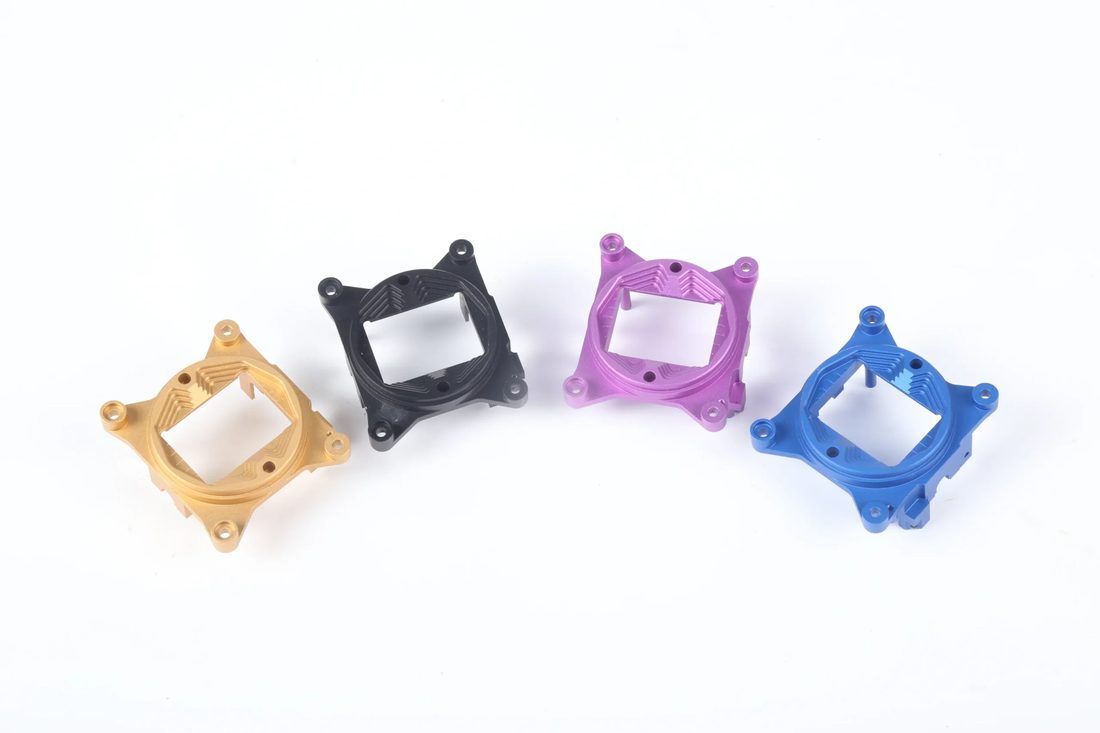
New Energy Vehicles (Battery Thermal Management) CNC precision component
How a Battery Liquid-Cooling Connector Seals: The Core Mechanism
Two mechanisms do almost all the work in pack cooling joints, and each demands a different surface.
If you understand only one thing about a battery liquid-cooling connector, make it this: an elastomer seal works by deformation, a metal-face seal works by contact geometry. One flows into imperfection; the other must be the barrier itself. Torque preloads both. Everything else — surface finish, machining difficulty, service life — follows from that distinction.
Elastomer seal: deformation as the barrier
Energy source: the interference built into an O-ring cross-section when the two halves are mated, driven by the clamp load your torque spec creates. Medium: a soft ring that flows into microscopic valleys on the seat. Result: a joint that tolerates modest scratches and flatness error because the rubber conforms. The price is an elastomer that can age, swell, or harden depending on coolant chemistry and temperature, and a groove that must be machined consistently or the ring will roll or cut on assembly.
Metal-face seal: geometry as the barrier
Energy source: preload from the coupling pushing two hard surfaces together. Medium: a finely machined cone or flat — often stainless steel finished to a mirror so asperities cannot form leak paths. Result: a joint with no elastomer to age, suited to higher temperature and aggressive coolants. The price is that the surface must genuinely be flat and smooth; there is nothing soft to bail you out if it is not.
Where each mechanism fails in a pack
Elastomer joints fail on chemistry and assembly: a compound incompatible with the coolant, a nick from a sharp thread entry, or compression set after years at temperature. Metal-face joints fail on surface and handling: a scored cone from a careless mate, embedded debris, or a finish that looked bright but held a directional grind pattern. Neither is universally better. The right answer depends on your coolant, temperature, service cycle count, and how clean your assembly process really is.
Liquid-Cooling Coupler Machining: Building the Seal Face
Seal performance is created at the machine, not at the test bench.
The route chosen on day one decides how much inspection you need on day thirty. A seal cone or O-ring seat has to be generated, finished, and protected through the whole process. Here is the three-step route we use on coupler work, and what each step buys you.
Step 1: traceable bar and a stress-relieving rough
We start from traceable stainless bar, carry the heat lot with the job, and remove bulk material while leaving stock on the functional surfaces. Coupler bodies are often lightened for dense pack packaging, which leaves thin sections that deflect under a standard chuck. Taking heavy cuts early means the finishing pass removes very little material and introduces very little new stress.
Step 2: finish the sealing geometry in one clamping
The seal face is finished in the same setup as the datum it relates to. With turn-mill composite equipment, the turned cone and any ports or flats are produced without moving the part to a second fixture, so the positional relationship is built in rather than re-established at transfer. Cross-hole deburring is a defined operation with its own inspection step, because a loose burr here travels downstream into a cooling channel.
Step 3: gauge before the part leaves the spindle
In-process gauging catches a drift while there is still time to correct an offset. Waiting until final inspection means you have already made a batch of parts that agree with each other and disagree with the drawing. On mating features held to ±0.005 mm, that distinction decides whether a production ramp stays stable.
This is the work our Dongguan plant was built around: 60 CNC machines including turn-mill centres, 5-axis equipment, and Swiss sliding-head lathes, on 4,000 m² of floor after the 2026 expansion. The older 2,000 m² figure still circulating is no longer current.
| Feature | Working target on this class of part | Why it matters to you | How we verify it |
|---|---|---|---|
| Seal-face finish | Ra ≤ 0.6 µm standard; 8K Ra 0.2 µm for metal-face cones | Controls weep and leak repeatability | Profilometer record and surface comparator |
| Mating diameter | ±0.005 mm capability window | Sets interference and preload consistency | In-process gauge plus final CMM report |
| Flatness / cone angle | Called out on the functional face only | A metal face seals on geometry, not gloss | CMM on the same datum as the seat |
| Port intersection | Defined deburr, no loose burr | Keeps debris out of cooling channels | Borescope check on the sample plan |
| Material identity | Heat lot carried with the batch | Lets you answer an audit months later | Incoming batch traceability and certificate |

New Energy Vehicles (Battery Thermal Management) CNC precision component
Turn-Mill Composite: One Clamping from Bar to Seal Face
The number of times a part is re-clamped is the number of relationships you have to inspect.
Turn-mill composite machining is the single most useful process decision on a battery liquid-cooling connector. In a conventional route, you turn the body on a lathe, move it to a mill for flats or ports, then re-fixture it to finish the cone. Each transfer re-establishes the datum, and each re-establishment is a chance for the seal face to drift out of relationship with the thread. A turn-mill centre finishes the turned and milled features in one clamping, so the geometry is built in.
What one clamping actually protects
Concentricity between the seal cone and the thread axis, the position of side ports relative to the seat, and the perpendicularity of the mating face. These are the features that decide whether the torque you apply produces even preload around the seal. If the cone is off-axis, one side compresses more than the other and the joint weeps at the low side no matter how high the wrench reads.
Turn-mill composite vs transferred operations
| Factor | Turn-mill composite | Turn then re-fixture |
|---|---|---|
| Setups for body + seal face | One clamping | Two or three fixtures |
| Datum relationship | Built in by the machine | Re-established at each transfer |
| Concentricity of cone to thread | Held by the spindle axis | Depends on re-clamping accuracy |
| Mating-feature capability | ±0.005 mm window held in process | Shop-dependent; often verified only at final |
| Inspection burden | Fewer relationships to measure | More CMM setups, more drift risk |
| Best fit | High-volume pack connectors | Low-volume or simple geometry |
Tight Tolerance CNC: Holding the Mating Interface
A tolerance is only real if it survives the whole batch, the coolant, and the cleaning line.
Specifying ±0.005 mm is easy. Holding it across a shift is a process question. On a battery liquid-cooling connector the risk is rarely one bad part; it is a slow drift through a batch so the last hundred pieces sit at the edge of the window. We treat tolerance as an in-process control, not a final-inspection filter.
Tool life and heat are part of the tolerance
A fresh insert and one near end of life leave different surfaces at the same offset, so we set tool life against finish and dimensional trend rather than a fixed piece count. Stainless holds heat at the cutting zone: a part measured hot is not the part measured at room temperature. We sequence roughing and finishing so measured features are produced when the part is stable, and we check at a controlled temperature.
Where ±0.005 mm is worth paying for
| Feature | Hold ±0.005 mm? | Reason |
|---|---|---|
| Seal mating diameter / groove | Yes | Sets interference and preload consistency |
| Cone angle and flatness | Yes, plus geometric callout | A metal face seals on geometry |
| Thread class | Per standard gauge | A thread gauge, not a CMM, is the right tool |
| Non-functional body OD | No — use a general tolerance | Tightening it adds cost, not sealing |
| Overall length | Only if it sets stack-up | Otherwise a general tolerance is enough |

New Energy Vehicles (Battery Thermal Management) CNC precision component
CNC Precision Machining and the Torque Spec You Can Trust
Torque is only a proxy for preload. The surface under it decides whether that preload seals.
Torque is the most misunderstood number on a battery liquid-cooling connector drawing. A technician applies a wrench value, but what the joint experiences is clamp load squeezing the seal. The relationship between torque and clamp load is affected by thread friction, lubricant, surface finish under the head or nut, and the geometry of the seat. Two joints torqued to the same value can carry very different preload if one seat is smooth and flat and the other is rough or off-angle.
Why a torque value needs a controlled surface
If the sealing face finish varies from batch to batch, friction varies, and the same torque produces a different clamp load — sometimes too little to seal, sometimes enough to crush an elastomer or distort a thin-walled body. This is why the torque spec and the seal-face Ra belong on the same drawing, reviewed together. A torque number without a controlled surface is a false sense of repeatability.
How to specify torque honestly
- 1. State the torque value and the tolerance band your design actually requires — not a single idealized number.
- 2. State the condition: dry or lubricated, and with what lubricant, because friction changes the preload you get.
- 3. Call out the seal-face finish and flatness the torque assumes, so preload stays consistent.
- 4. Define the assembly tool and sequence for multi-fastener flanges, so the preload is even.
- 5. Record the achieved torque at the test station and tie it to the pressure-test record for that serial or batch.
We do not invent a universal torque value for your connector — it depends on your thread, seal, and coolant. What we do is machine the surface that makes your specified torque behave the same way on the first part and the ten-thousandth. If you want a second opinion on whether your surface and torque spec are compatible, send us your drawing for a free DFM review.
CNC Precision Machining: Pressure-Test Traceability
A leak test is only as honest as the method and the record behind it.
You will see datasheets claim 'leak-free' with no pressure, duration, method, or acceptance rate. That phrase is meaningless. A useful specification states the test fluid, pressure, hold time, acceptance rate, and whether the test applies to samples or every part. For a pack component that will sit in a vehicle for years, the record matters as much as the pass.
Pressure decay at a 10 bar hold
The part is pressurised, isolated, and monitored for a pressure drop over a set interval. A frequently seen design target on this class of part is a hold around 10 bar with an equivalent leak rate below 0.01 mL/min. Pressure decay is production-friendly — fast and non-destructive — but temperature drift and trapped volume can fool a poorly designed test, so the method must be controlled.
Bubble immersion and helium tracer
Bubble immersion under water is a useful visual check for gross leaks and easy to run on samples, but it lacks sensitivity for a slow weep. Helium mass-spectrometry leak detection is far more sensitive and is the right tool when a design target is tight, at the cost of time and equipment. Ask which method sits behind any number a supplier quotes.
What a traceable record contains
A record that says 'pass' without the measured value, gauge ID, torque applied, and acceptance rate cannot help you diagnose a field problem. We tie the functional dimensions and the test conditions together so a trend is visible before it becomes a failure, and we carry the heat lot with the batch. Where documented material identity is required, we can supply EN 10204 3.1 certificates with the batch.
| Method | What it detects | Sensitivity | Fit for production |
|---|---|---|---|
| Pressure decay | Overall pressure loss at a stated hold, e.g. 10 bar | Moderate; sensitive to temperature and volume | High — fast and repeatable when controlled |
| Bubble immersion | Visible gross leaks | Low; slow weeps are missed | Sample checks and gross-leak screening |
| Helium tracer | Very small leak paths | High | Qualification and tight design targets |
| Visual / borescope | Burrs, scores, contamination on the seat | Not a leak test | Complements pressure testing on the sample plan |

New Energy Vehicles (Battery Thermal Management) CNC precision component
Battery Liquid-Cooling Connector Seal Face vs Torque: Hard-Number Comparison
Two quotes can look identical on a spreadsheet and behave completely differently at incoming inspection.
Here is the comparison we use when a buyer asks why two connector quotes differ. The figures are the ones that matter on this class of part, drawn from our process capability and from the targets that appear on pack drawings. Treat the target column as what your drawing may ask for, not as a universal guarantee.
| Factor | Elastomer (O-ring) seat | Metal-face cone |
|---|---|---|
| Seal mechanism | Elastomer deformation into the seat | Hard-on-hard contact geometry |
| Seal-face roughness target | Often Ra ≤ 0.6 µm standard mirror | Ra 0.2 µm / 8K mirror commonly specified |
| Dimensional control | ±0.005 mm on mating diameters and groove | ±0.005 mm plus flatness/cone-angle control |
| Typical leak-rate target | Below 0.01 mL/min at a stated hold | Below 0.01 mL/min; more sensitive to surface |
| Torque sensitivity | Moderate; ring conforms but can cut or roll | Higher; preload must be even across the face |
| Temperature / chemistry | Limited by elastomer compound | No elastomer to age; coolant must stay clean |
| Assembly sensitivity | Forgiving of minor scratches | Sensitive to handling and contamination |
| Relative machining cost | Lower; groove finish dominates | Higher; cone finishing and inspection dominate |
Six factors, one at a time
- 1. Coolant chemistry. Match the seal to what is actually in the loop — water-glycol, dielectric fluid, or something else. The wrong elastomer fails sooner than any machining error.
- 2. Temperature and life. If the joint sees sustained heat, ask what ages first: the ring or the surface. That decides which architecture to buy.
- 3. Surface specification. Decide which face seals and specify that face alone. A blanket mirror note is expensive and vague.
- 4. Torque and datum chain. Count how many times the part is re-clamped between the datum and the seal face, and how evenly the specified preload lands.
- 5. Test evidence. Ask for the measured value, the method, the torque applied, and the acceptance rate — not a pass stamp.
- 6. Capacity proof. Ask what the supplier actually runs per month and what share your program would consume.
Do not buy a glossy finish or a big torque number. Buy evidence that the joint still holds on the thousandth part.
Which Battery Liquid-Cooling Connectors Fit Your Pack?
A decision table beats a parameter dump when you need to choose this week.
Use the table below as a starting point, then pressure-test it against your own coolant, temperature, and assembly reality. If you want the second opinion of a shop that machines both styles, send us your drawing — you will get a short, specific answer on which surface features drive cost.
| Your requirement | Recommended direction | Why it wins |
|---|---|---|
| Water-glycol loop, normal line assembly, occasional service | Elastomer seal on a controlled Ra ≤ 0.6 µm seat | Forgiving of minor damage and technician handling |
| Hot dielectric fluid, long service interval | Metal-face seal on an 8K Ra 0.2 µm cone | No elastomer to age or swell |
| Very tight leak-rate target | Metal-face seal with helium-qualified surfaces | Surface can be verified to a high sensitivity |
| Prototype or low volume, forgiving geometry | Elastomer seal with a careful drawing | Avoid paying for cone finishing you do not yet need |
| High-volume pack ramp with audited traceability | Either style, tight tolerance CNC with batch records | Consistency and evidence matter more than the first article |
| Torque-critical flange with several fasteners | Either style, defined torque sequence and controlled face | Even preload prevents low-side weep |
Pros
- Choose an elastomer-seat connector if your coolant chemistry is well understood and you want a forgiving joint that survives field handling.
- Choose an elastomer-seat connector if your budget favours lower machining cost and your leak-rate target is moderate.
- Choose a metal-face connector if you need to remove elastomer aging in a hot or aggressive coolant.
- Choose a metal-face connector if you control cleanliness and want a surface whose leak performance can be verified precisely.
Cons
- Reconsider a metal-face connector if assembly happens in a dirty environment; a single scored cone undoes the finish.
- Reconsider an elastomer seal if the compound is incompatible with the coolant or the joint sees sustained high temperature.
- Do not choose either on gloss or torque alone; the surface you cannot see — flatness, lay, edge break — decides the leak result.

New Energy Vehicles (Battery Thermal Management) CNC precision component
Buyer's Checklist for Liquid-Cooling Coupler Machining
The things to put in writing before a purchase order, not after a problem.
Supplier selection is less about adjectives and more about what a factory will put in writing. Whatever sealing architecture you choose, these are the items we would request in your position — and the ones we keep ready because our customers ask for them.
- A DFM response that names your functional surfaces and tells you which tolerances and finishes drive cost. A supplier who says yes to every callout without comment has not read the drawing.
- A material certificate and heat-lot identification tied to the specific batch you receive.
- An initial dimensional report on the seal face, mating diameters, and groove or cone geometry — measured after the final machining operation.
- A defined pressure-test method with pressure, hold time, measured values, acceptance rate, and the torque applied — plus a stated burr-control process.
- A capacity and ramp statement: monthly output, the machines behind it, and how your volume fits into the plan.
Red flags in a low quote
- The quote is instant and unconditional, with no question about coolant chemistry, service cycles, the seal face, or the torque spec.
- The supplier offers a mirror finish on every surface, which usually means nobody has identified the surface that matters.
- Traceability is 'available' but not included in the batch documentation.
- The sample is beautiful and the production control plan is vague. One good part is not a process.
- The address is an office and a visit to the machining floor is politely avoided.
If you want to see how we handle the first item, look at how our liquid-cooling technical guides break down seal faces and tolerances, then send us your drawing. A DFM review is useful information whether or not you place an order.
Common Mistakes in Tight Tolerance CNC of Battery Couplers
Most coupler failures are process failures already visible at the drawing stage.
| Mistake | Symptom you will see | What we do instead |
|---|---|---|
| Finishing the seal face before all heavy cuts | Passes inspection, leaks after assembly | Rough first, then finish the face in a stable condition |
| Re-clamping between thread and seal face | Scored face on assembly, inconsistent leak results | Turn-mill composite in one clamping with a common datum |
| Torque spec with no surface spec | Preload varies, weep appears at the low side | Specify face finish and flatness alongside the torque |
| Treating deburr as a manual afterthought | Debris in cooling channels, intermittent blockage | Defined deburr operation with a borescope sample check |
| Cannot read a first-article report | Drift accepted as normal variation | Review functional dimensions before releasing volume |
Mistake 1: polishing instead of controlling geometry
A bright surface looks convincing. It does not guarantee a flat one. When a buyer asks for the highest gloss available, we ask what the gloss is meant to achieve. If the answer is sealing, we talk about flatness, lay direction, and edge condition. If the answer is appearance, we tell them they are paying for something the coolant will never notice.
Mistake 2: confusing a sample with a process
Any supplier can make one excellent connector on a quiet afternoon. The question is what the five-hundredth looks like at the end of a shift. Ask for the control plan: how offsets are checked, when tools are changed, and what happens when a dimension starts to walk. If there is no answer, the sample was luck.
Mistake 3: ignoring the coolant and the assembly environment
Water-glycol and dielectric fluids do not treat every stainless surface or elastomer the same way. Chloride content, temperature, stagnation, and how cleanly the joint is mated all matter. We ask what is actually in the loop and who will assemble it before finalising finish and passivation.
After machining, stainless couplers need a cleaning and passivation step that restores corrosion resistance without attacking the finish. ASTM A967 is the standard reference for chemical passivation of stainless steel; we use it as the framework for treatment and the acceptance discussion with the buyer.

New Energy Vehicles (Battery Thermal Management) CNC precision component

New Energy Vehicles (Battery Thermal Management) CNC precision component

New Energy Vehicles (Battery Thermal Management) CNC precision component
FAQ: battery liquid-cooling connectors & New Energy Vehicles (Battery Thermal Management) Buyer Questions
A: For a metal-face cone, a target around Ra 0.2 µm (8K mirror) is commonly specified; our standard mirror is Ra ≤ 0.6 µm, which is usually adequate for O-ring seats. Roughness average alone is not enough — also call out flatness, lay direction, and edge break on the actual sealing face, and ask for the measurement after final machining. Treat Ra ≤ 0.4 µm as a drawing target to confirm against your geometry, not a universal promise.
A: They are inseparable. Torque is a proxy for clamp load, but the preload you actually get depends on thread friction and the finish and flatness of the seat. If the face finish varies, the same torque produces a different preload. Specify the torque value and condition (dry or lubricated) together with the seal-face finish and flatness, and record the achieved torque against the pressure-test result.
A: Those are typical design targets on this class of part, and your geometry decides whether they are realistic. We review the seal face, coolant, and test method before committing to a number. Ask any supplier for the measured value, the method (pressure decay, bubble, or helium tracer), the hold time, and the acceptance rate — not just a pass stamp.
A: Turn-mill composite finishes the turned seal face and any ports or flats in one clamping, so the cone-to-thread relationship is built in instead of re-established at transfer. Tight tolerance CNC holds mating features to a ±0.005 mm capability window and catches drift in process rather than at final inspection. Fewer setups mean fewer sources of variation and a shorter inspection report.
A: Yes. Confidentiality is our normal operating procedure. We run NDA and controlled drawing access for programs including De'Longhi, Donlim, and Breville, and apply the same discipline to anonymous EV projects. We discuss process and capability, never a customer's identity or design details.
A: We use ASTM A967 as the reference framework for chemical passivation of stainless steel and can provide EN 10204 3.1 material certificates with the batch when required. LusterControl is ISO 9001 certified (certificate 25025Q13824R0S, valid through 2028-12-02); the ISO 13485 quality system is established with certification in progress, and IATF 16949 is at the application stage.
Send us your battery liquid-cooling connector drawing for a free DFM review. Tell us the coolant, working pressure and test method, the torque spec and assembly condition, and your target monthly volume — and we will tell you which seal face and surface targets are worth paying for before you commit a purchase order.
Request a Free CNC Quote