LusterControl News: Scaling to 60+ CNC Machines for Global OEM Demand (2026)
If you buy precision machined parts for an OEM program, capacity is a quiet kind of risk. A shop that quotes beautifully on a 200-piece pilot can fall apart at 20,000 pieces when a machine goes down or a fixture wears out - and you find out only when your line stops. That is the exact gap we have spent 2026 closing, and this LusterControl news update is written for buyers, not for our own press release.
Our Dongguan factory now runs 60+ CNC machines across a 4,000 sqm floor, with monthly output around 500,000 finished parts. But the number that matters to you is not the machine count - it is what that capacity lets us guarantee: parallel new-product-introduction and volume production, redundant cells so one fault never stops your order, and the same +/-0.005 mm accuracy whether we cut one part or fifty thousand.
Below we walk through how the floor is built, which processes earned the investment, how our quality system scales with it, and a verification checklist you can hand to any supplier before you commit. We have been a South China source factory since 2015 - 15 years deep in stainless mirror CNC machining - so this is the shop-floor view, not a brochure.
Table of Contents
- 1. LusterControl News: Scaling Capacity to Meet Global OEM Demand
- 2. How CNC Precision Machining Capacity Grew to 60+ Machines
- 3. Turn-Mill Compound Machining: Why One Setup Serves Global OEMs
- 4. Stainless Steel Mirror Finishing at Volume: From Ra 0.6 to 8K
- 5. Inside the Dongguan Factory: 4,000 sqm of Precision Capacity
- 6. How a Dongguan Factory Serves Global OEM Supply Chains
- 7. CNC Precision Machining Quality System Behind the Scale-Up
- 8. What the Capacity Expansion Means for Global OEM Buyers
- 9. LusterControl News: What Comes Next After 60+ CNC Machines
Company AI part image
LusterControl News: Scaling Capacity to Meet Global OEM Demand
More machines only help if the discipline scales with them.
The headline LusterControl news for 2026 is simple: our floor now operates 60+ CNC machines and spans 4,000 sqm of production space, supporting roughly 500,000 machined parts every month. The reason we expanded is equally simple - the programs we run for global OEMs kept growing, and adding capacity was the only honest way to protect their lead times without cutting corners on tolerance.
Since 2015 we have focused on CNC precision machining of stainless steel with mirror-class surface finish. That reputation brought us into appliance programs for brands such as De'Longhi, Donlim, and Breville, a drone customer whose first production order with us reached 1.2 million RMB, and an annual output now above 20 million RMB. Those relationships are exactly why we reinvested in more turn-mill and 5-axis equipment rather than cheaper, looser-tolerance capacity.
Company AI part image
How CNC Precision Machining Capacity Grew to 60+ Machines
Growth by machine type, not just by machine count.
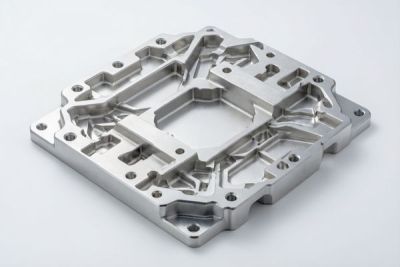
A '60+ machines' headline means little unless you know what those machines do. Our CNC precision machining floor is a deliberate mix: 3-axis and 3+1 centers for high-volume plates and brackets, turn-mill compound lathes for shafted and contoured parts, 5-axis simultaneous centers for multi-face work, and Swiss-type sliding-headstock machines (走心机) for long, slender, tight-tolerance turned parts. Each class earns its place by the part profile it serves best.
We did not buy 60 identical machines. We bought the mix that lets a single purchase order - say, a stainless valve body plus its turned stem plus a 5-axis bracket - flow through the right process for each feature instead of being forced into one compromised process. That is what 'capacity' should mean to a buyer: the right machine is free when your job needs it.
| Machine class | Share of floor | Best for | Typical accuracy |
|---|---|---|---|
| 3-axis / 3+1 centers | Largest | Plates, brackets, spacers | +/-0.01 mm |
| Turn-mill compound lathes | Growing fast | Shafted + contoured parts | +/-0.005 mm single setup |
| 5-axis simultaneous | Strategic | Multi-face, cradles, arms | +/-0.005 mm |
| Swiss sliding-headstock | Specialist | Long slender turned parts | +/-0.005 mm |
What 60+ machines actually buy you as a buyer
- Parallel NPI and volume: prototype the next revision while this month's production runs
- Redundant cells: one machine down does not stop your order
- Mixed lot sizes: small custom batches and 500k/month volume on one floor
- Faster quotes: we pick the cheapest process that still meets your true-position callout
- Buffer for demand spikes without outsourcing to an unknown sub-shop
Turn-Mill Compound Machining: Why One Setup Serves Global OEMs
One chucking, turned and milled features, one datum.
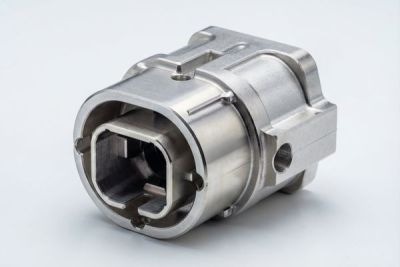
Turn-mill compound machining is the workhorse behind most of our stainless parts, and it is the reason a global OEM can trust volume consistency. The part is clamped once on the spindle, turned to diameter, then milled, drilled, and threaded in the same chucking before a sub-spindle hands it off for backwork. Because the coordinate system never releases, we hold positional accuracy to +/-0.005 mm across both turned and milled features.
For a buyer, the payoff is fewer fixtures, less handling, and no datum shift between operations. A valve stem with a milled flat and cross-drilled hole that would need two or three setups on separate machines gets done in one. That removes the 0.02-0.05 mm re-clamp error you never see on a first article but live with across a lot.
The three-step flow we run on every turn-mill part
- Bar feed and clamp on the main spindle; turn the primary diameter and form
- Live tooling mills flats, drills cross-holes, and threads - still in the first chucking
- Sub-spindle captures the part and completes backwork, then parts are separated and deburred
| Factor | Lathe + separate mill | Turn-mill compound |
|---|---|---|
| Setups | 2-3 re-clamps | 1 chucking |
| Datum shift | 0.02-0.05 mm per re-clamp | None after first clamp |
| Handling / touching | High | Low |
| Consistency at volume | Lot-to-lot drift risk | Tight, single-datum |
| Our accuracy | +/-0.01 mm | +/-0.005 mm |
Company AI part image
Stainless Steel Mirror Finishing at Volume: From Ra 0.6 to 8K
Mirror finish is a function, not a cosmetic extra.
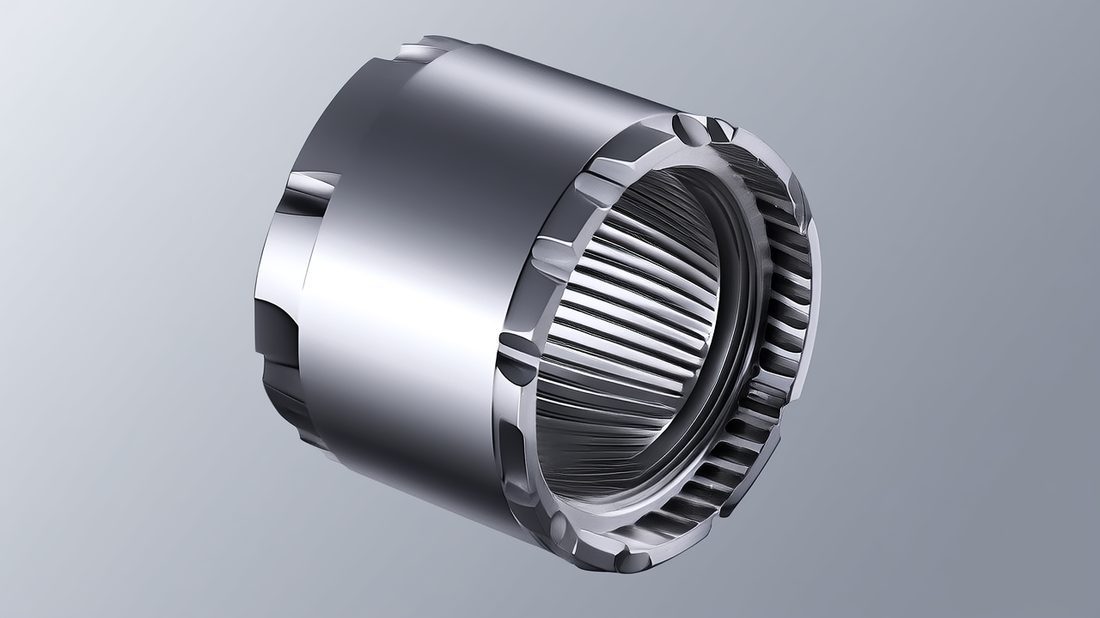
Stainless steel mirror finishing is where our 15 years show. Our standard mirror line reaches Ra 0.6 micro m; the top 8K finish reaches Ra 0.2 micro m. At volume this is not a hand-polish lottery - it is a controlled process of progressive grits, electrochemical polishing where the geometry allows, and verified surface measurement on every critical lot.
- Mirror finishing
- A controlled process that takes a machined stainless surface to a reflective, low-Ra state that resists particle adhesion and cleans easily
- 8K finish
- The top tier of stainless mirror, reaching roughly Ra 0.2 micro m - used where flow, seal, or hygiene demand the smoothest face
- Ra (roughness average)
- The arithmetic mean of surface peaks and valleys in micro meters; lower Ra means smoother, more sealing-friendly surface
Why it matters to a buyer: a mirror face on a fluid or food-contact part means fewer trapped particles, better seal contact, and easier cleaning validation. On a medical or semiconductor part it shortens the path to a clean, low-particle surface. We hold the finish on the features that need it and leave costlier rough faces alone - tolerance and finish are both budgets you should spend where the function lives.
| Finish tier | Typical Ra | Typical use | Standard discipline |
|---|---|---|---|
| Standard mirror | <= 0.6 micro m | Handles, housings, general | In-process gauging |
| High mirror | ~ 0.3 micro m | Food / fluid contact | Surface measurement per lot |
| 8K mirror | ~ 0.2 micro m | Seals, medical, semiconductor | Full trace + measurement |
| Passivation | n/a (surface treat) | All stainless | ASTM A967 |
Inside the Dongguan Factory: 4,000 sqm of Precision Capacity
Layout is a quality tool, not just real estate.
Our Dongguan factory is a South China source factory built for both small-batch custom work and large-volume runs. The 4,000 sqm floor is laid out as a flow, not a warehouse: incoming material and inspection at one end, machining cells in the middle, finishing and metrology toward the out-feed, and packing under controlled conditions. The point is to never let a finished, measured part cross paths with raw stock or shop-floor grit.
How the layout protects your tolerance
- Incoming inspection and material cert check before any bar is loaded
- Segregated cells so stainless medical work never shares a bench with mixed jobs
- Climate-stable metrology room so CMM numbers are not skewed by afternoon heat
- Lot traceability from raw bar through machining to finished pack
- First-article CMM report before a new revision goes to volume
Company AI part image
How a Dongguan Factory Serves Global OEM Supply Chains
Capacity is only useful if it ships and documents correctly.
A Dongguan factory sits inside one of the densest manufacturing ecosystems on earth, with component supply, surface treatment, and export logistics all within reach. For a global OEM that means shorter physical lead times and a real path to dual-sourcing risk reduction - you can qualify a second line on the same floor without crossing a border. But location is not the whole story; documentation and communication carry the order.
We treat the paperwork as part of the part. Material certs traceable to the heat lot, first-article measurement reports, in-process gauging records, and lot-level traceability are prepared as the job runs, not scrambled together the night before ship. For buyers managing PPAP-style requirements, that discipline is what lets your quality team sign off without a site visit every time.
| Buyer concern | How we address it |
|---|---|
| Lead time | 60+ machines + redundant cells absorb spikes |
| Traceability | Bar-to-part lot trace, certs on file |
| Quality evidence | CMM first article + in-process gauging |
| Logistics | Dongguan export hub, flexible pack/outbound |
| Risk | Second line qualified on same floor (dual-source) |
CNC Precision Machining Quality System Behind the Scale-Up
The certs scale; the paperwork does not get skipped.
Scaling CNC precision machining to 500,000 parts a month only works if the quality system scales with it. Ours is anchored on ISO 9001 (certified), extended into the medical device scope through ISO 13485 (completed), and aligned toward automotive through IATF 16949 (in application). Stainless parts are passivated per ASTM A967 so handling and service environments do not introduce corrosion you will find only after field returns.
The practical promise to a buyer: a part made on day one of a lot and a part made on day thirty are held to the same datum, the same gauging, and the same traceability. We do not relax inspection as volume rises - we automate it. That is the difference between a floor that is merely big and one you can actually depend on.
| Standard | Scope | Our status | What it proves to you |
|---|---|---|---|
| ISO 9001 | General QMS | Certified | Documented, audited process control |
| ISO 13485 | Medical devices | Completed | Device-grade traceability & hygiene |
| IATF 16949 | Automotive | In application | PPAP-style discipline coming online |
| ASTM A967 | Stainless passivation | In routine use | Corrosion-resistant finish |
Documents to request before you commit
- ISO 9001 (or better) certificate, current and in-scope
- Material certs traceable to the heat lot
- CMM first-article report with full datum references
- In-process gauging and lot traceability records
- Passivation / finish spec (ASTM A967 where stainless)
- A written rework and containment path for non-conforming lots
Company AI part image
What the Capacity Expansion Means for Global OEM Buyers
Shorter lead times, lower risk, same accuracy.
For a global OEM, the capacity expansion translates into three concrete benefits. First, lead time: with redundant cells and 60+ machines, your order no longer waits behind someone else's. Second, risk: we can qualify a second line on the same floor, so a single machine or shift problem does not become your line-down event. Third, concurrent engineering: we run your next revision's prototype while this month's volume ships, so NPI and production stop fighting for the same capacity.
None of this changes the numbers that matter most - we still hold +/-0.005 mm positioning and mirror finishes down to Ra 0.2 micro m, and we still trace every bar to the finished part. Capacity without that discipline would just be more scrap, faster. If you are weighing a move to UAV structural components or medical device components on our floor, the scale-up is what makes a pilot-to-volume jump safe.
Pros
- Shorter, more predictable lead times
- Redundant cells cut line-down risk
- Pilot and volume run in parallel
- Second qualified line enables dual-sourcing
- Same +/-0.005 mm accuracy at any volume
Cons
- Bigger floor means tighter scheduling discipline required
- You must still verify certs and traceability up front
LusterControl News: What Comes Next After 60+ CNC Machines
The next investment is automation and medical clean capability.
This LusterControl news update is not the end of the roadmap. With the 60+ machine floor in place, the next investments are targeted: more 5-axis simultaneous capacity for complex multi-face parts, robotic loading to stabilize unattended night runs, and a cleaner, more controlled cell for medical and semiconductor work where particle control is part of the spec, not an afterthought.
For buyers, the practical meaning is continuity. The floor you qualify today will keep getting more capable without re-qualifying the fundamentals - the certs, the traceability, and the +/-0.005 mm accuracy stay. If you have a program that is outgrowing its current supplier, that is exactly the moment to talk. Send us your drawing and we will return a free DFM review that flags where single-setup turn-mill or 5-axis saves you money and risk.
Capacity is only worth having if the part that comes off machine 60 is identical to the part that came off machine 1 - that is the promise we built the floor to keep.
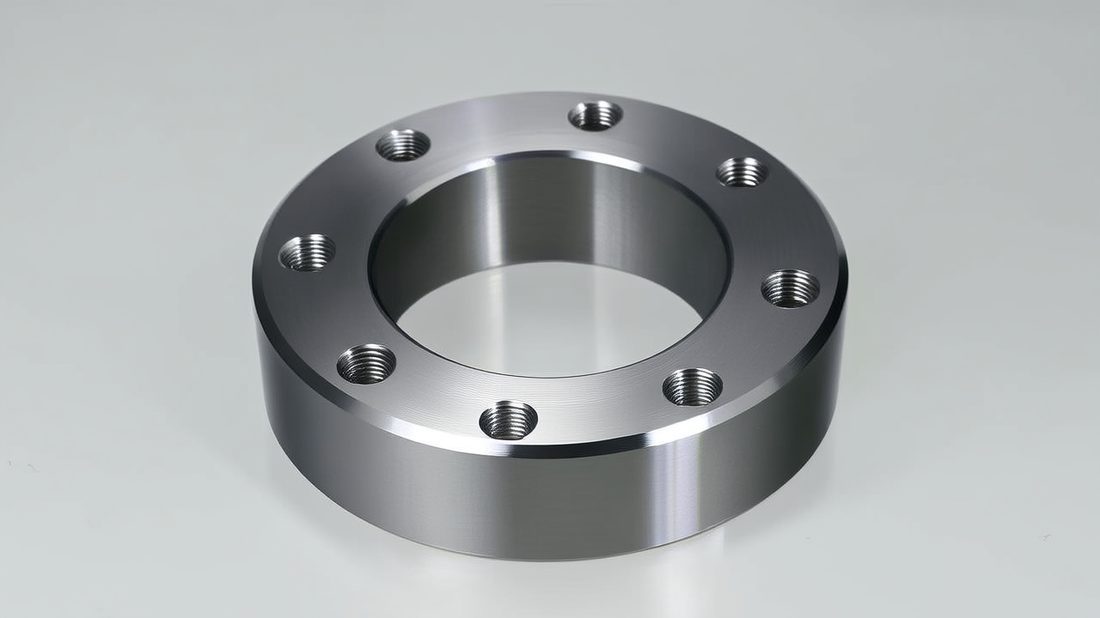
Company AI part image
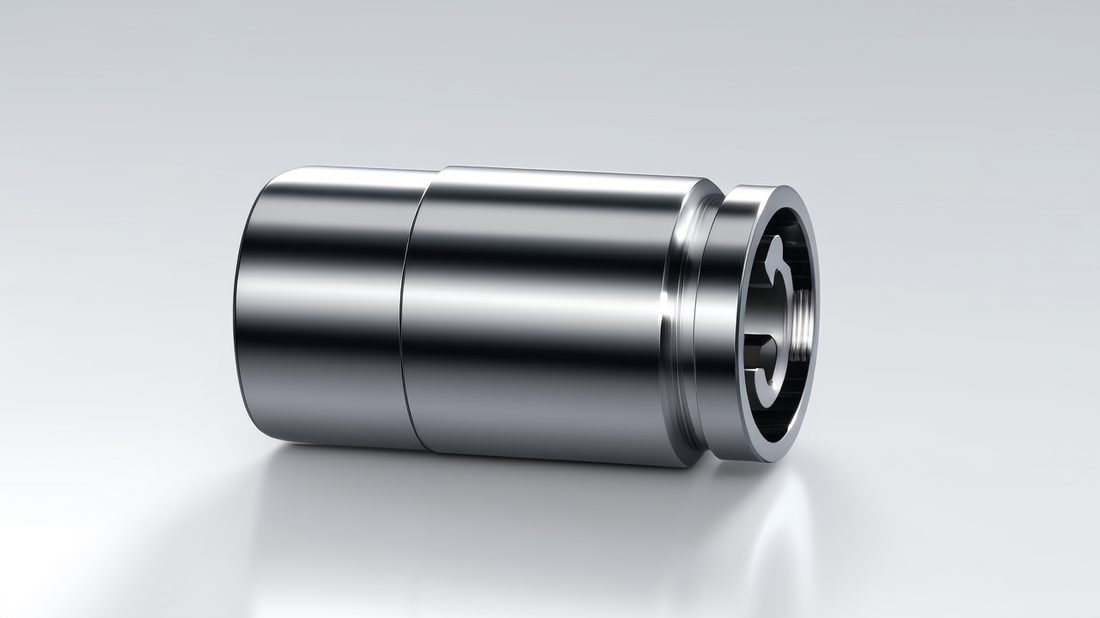
Company AI part image
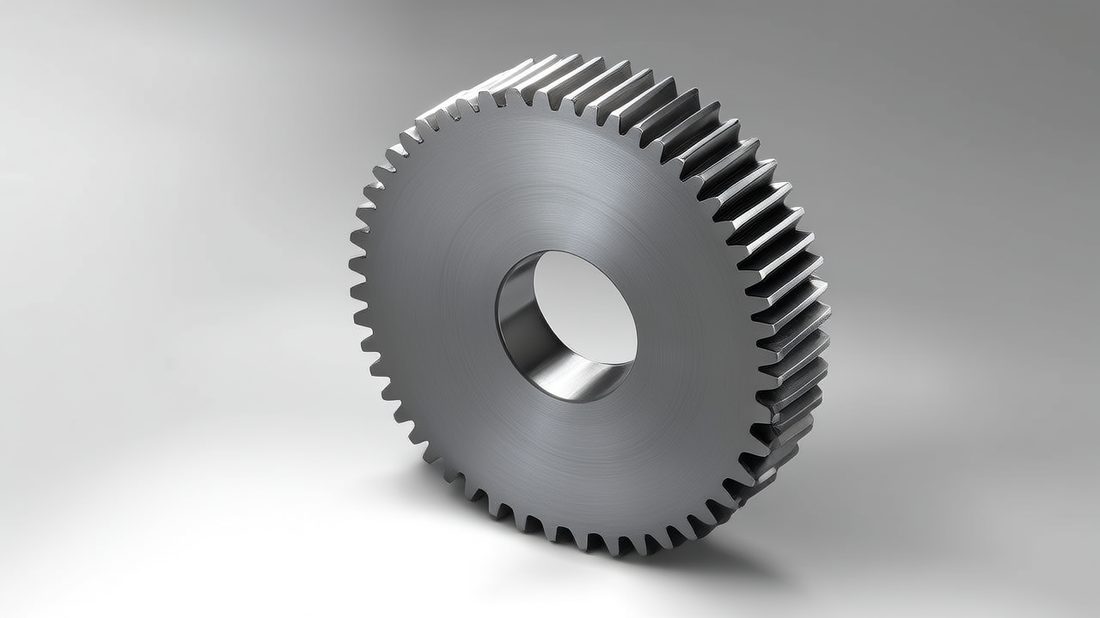
Company AI part image
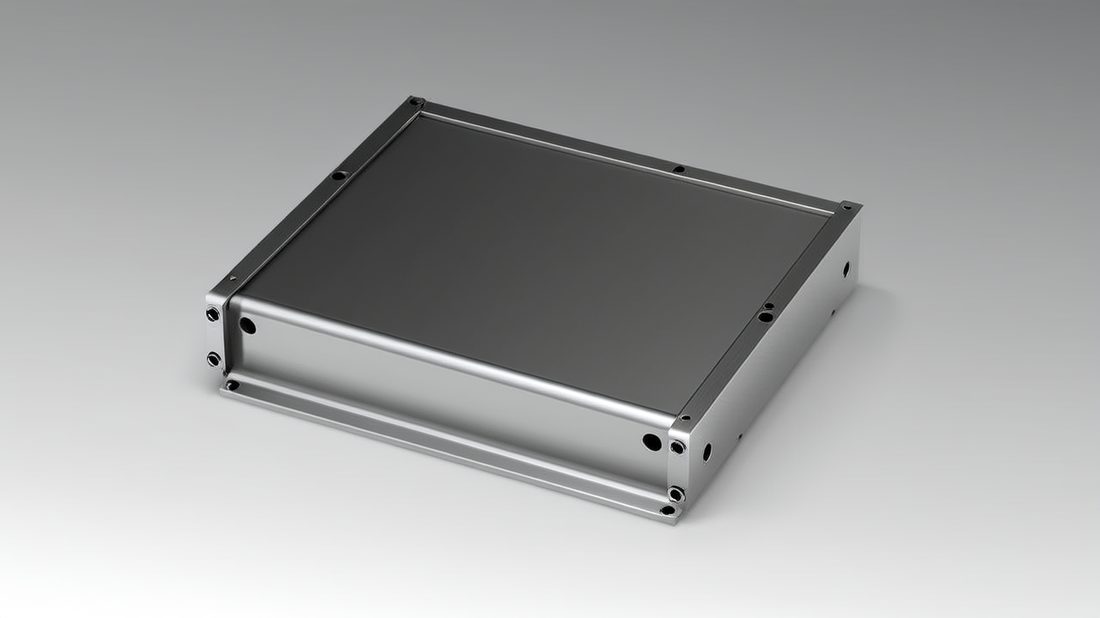
Company AI part image
FAQ: LusterControl news & Company Buyer Questions
A: Our Dongguan factory now operates 60+ CNC machines across a 4,000 sqm floor, with monthly output around 500,000 finished parts. The mix spans 3-axis centers, turn-mill compound lathes, 5-axis simultaneous machines, and Swiss sliding-headstock machines so each part profile runs on the right process.
A: We are ISO 9001 certified, have completed ISO 13485 for the medical device scope, and have IATF 16949 in application for automotive. Stainless parts are passivated per ASTM A967. Customers can request material certs, CMM first-article reports, and lot-level traceability from raw bar to finished part.
A: Yes. Beyond location, reliability comes from the documentation and redundant capacity: 60+ machines with duplicate cells, bar-to-part traceability, first-article CMM reports, and in-process gauging. A second line can be qualified on the same floor, which gives global OEM buyers a built-in dual-source path without crossing a border.
A: Because the part is clamped once and turned, milled, and drilled in the same chucking, we hold positional accuracy to +/-0.005 mm with no datum shift between operations. Mirror finishing reaches Ra 0.6 micro m standard and Ra 0.2 micro m at the 8K tier, verified per lot on critical faces.
A: The same floor runs small custom batches and 500k/month volume, so a small buyer gets the cert stack, traceability, and CMM evidence of a large program without paying for dedicated capacity. Redundant cells also mean your prototype is never bumped by a bigger order.
A: Request the cert stack (ISO 9001 minimum), material certs traceable to the heat lot, a CMM first-article report, in-process gauging and traceability records, the passivation/finish spec, and a written rework path. A cheap quote with no traceability is the most expensive part you will buy - verify the documents before you commit.
Sending us your drawing gets you a free DFM review - we will flag the features that should move to single-setup turn-mill or 5-axis, the tolerances that are costing you money, and the finish tier your application actually needs. Reach out and let's cut the first article on our 60+ machine floor.
Request a Free CNC Quote