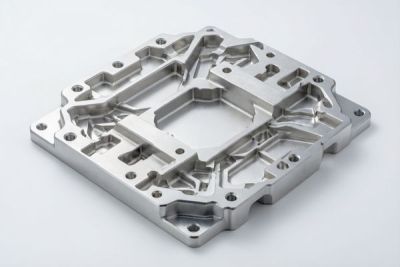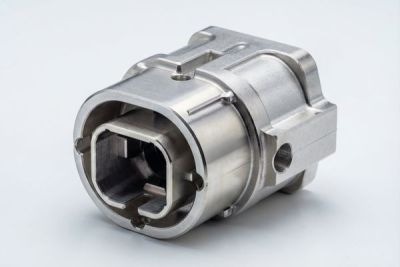
Machining Invar Mirror Bases for Thermal Stability
If you are buying optical components for Optical applications, the part that looks fine on a drawing can still fail in the field — at the worst moment. specifying optical components that must hold tight tolerances and survive real operating loads is exactly where most sourcing mistakes happen, and where a disciplined supplier earns its fee.
At LusterControl we have spent 15 years machining stainless and alloy precision parts on 60 CNC machines across a 4,000 m² plant. This guide walks through what a Optical buyer should actually check before releasing a PO — written the way an engineer talks to another engineer, with numbers you can verify.
Table of Contents
- 1. Why Optical Components Matter for Optical Buyers
- 2. How Invar Machining Is Machined at LusterControl
- 3. Tolerances and Inspection on Sub-Micron Stability
- 4. Material and Surface Finish for Lens Barrel Machining
- 5. Comparing Suppliers for Cnc Instrumentation
- 6. Buyer's Checklist for Precision Base
- 7. Cost and Lead Time for Optical Components
Optical AI part image
Why Optical Components Matter for Optical Buyers
A mirror bases is rarely the hero of your assembly, but it is usually the part that determines whether the whole product passes qualification. For Optical programs, optical components sit at the intersection of fit, function and cost.
The buyer's real risk
Miss the tolerance and you get scrap, rework loops and a delayed launch. Pick the wrong process and you pay for capability you do not need — or worse, you under-buy and the part cannot hold up. That is why Optical Components deserve a second look before PO.
Optical AI part image
How Invar Machining Is Machined at LusterControl
Most optical components are produced on a combination of turning and milling. LusterControl runs 60 CNC machines covering turn-mill composite, 5-axis, mirror/electropolishing, Swiss-type turning, lot traceability — so a part that needs multi-side features is done in fewer setups, which means less stack-up error.
Choosing the right process
- 3-axis milling for simple profiles — cheapest, fast.
- Turn-mill composite for round parts with milled features — one chucking, better concentricity.
- 5-axis when you need deep cavities or tight angular features without re-fixturing.
- Swiss-type turning for long, slender, high-volume shafts where runout matters.
Tolerances and Inspection on Sub-Micron Stability
LusterControl holds ±0.005 mm on stainless mirror-finished parts. But a number on a drawing means nothing without proof, so every high-precision item ships with CMM first-article data and ISO 9001 certified, ISO 13485 completed, IATF 16949 applying controls behind it.
| What you should request | Why it matters |
|---|---|
| First-article CMM report | Measured data, not a promise — your baseline for incoming inspection. |
| Lot traceability | Every batch ties back to material and machine for field failures. |
| 100% final inspection plan | Incoming, in-process and final checks before shipment. |
| Material cert (MTR) | Confirms the alloy is what the print calls for. |
Optical AI part image
Material and Surface Finish for Lens Barrel Machining
For optical components the alloy decides corrosion resistance, hardness and cleanability. LusterControl machines 304, 316/316L, 303, 440C and 630 (17-4PH) stainless.
- 304 — general corrosion resistance, the default workhorse.
- 316 / 316L — chloride, marine and medical exposure.
- 440C — hardenable, wear-resistant moving parts.
- 630 (17-4PH) — high strength with good corrosion resistance.
Surface matters too. LusterControl reaches Ra 0.6 μm (standard), up to 8K mirror Ra 0.2 μm — the difference between a seal that holds and one that weeps, or a part that sterilizes clean versus one that traps residue. We do electropolishing in-house, so lead time stays short.
Comparing Suppliers for Cnc Instrumentation
Not all shops that quote optical components are equal. The table below is the quick lens a Optical buyer should use when the prices look similar.
| Supplier model | Best for | Watch-out |
|---|---|---|
| Trading company | White-label, re-export convenience | You pay a margin and lose traceability to the source. |
| Job shop (no finishing) | Simple one-off parts | You manage plating/polish handoffs and lead time. |
| One-stop source factory (LusterControl) | Turn-mill-finish-assembly in one PO | Confirm certs match your industry upfront. |
Optical AI part image
Buyer's Checklist for Precision Base
Before you release a PO for optical components, run this list. It takes five minutes and removes most of the risk on a Optical program.
- Drawing is 2D + 3D and the real annual volume is stated.
- Tolerance is called out (not just 'as per drawing').
- Material grade and finish (Ra) are specified.
- Inspection plan and AQL are agreed up front.
- Material cert + lot traceability are in the contract.
- Free DFM review is done before PO to avoid rework loops.
Cost and Lead Time for Optical Components
Unit price on optical components is material + machine time + finishing + inspection + packaging. LusterControl prices transparently so you can trade off tolerance, finish and volume instead of guessing.
- Send a clean drawing and the real annual volume.
- Confirm material early so we reserve stock.
- Book a free DFM review before PO to relax non-critical tolerances.
- Bundle volume for a sharper unit rate.
Optical AI part image
Optical AI part image
Optical AI part image
Optical AI part image
Optical AI part image
FAQ: optical components & Optical Buyer Questions
A: We hold ±0.005 mm on stainless mirror-finished parts, with CMM first-article data and lot traceability for every batch. For a Optical buyer that means the fit and scrap risk are designed out before cutting.
A: 304 for general use, 316/316L for chloride or medical/marine exposure, 440C when you need hardenable wear resistance. We machine 304, 316, 303, 440C and 630 (17-4PH), each with a material cert.
A: Yes. LusterControl is a Dongguan source factory: turning, milling, 5-axis, mirror/electropolishing, anodize and assembly are all in-house across 4,000 m² plant with 60 CNC machines — one PO, one quality record.
A: ISO 9001 certified, ISO 13485 completed, IATF 16949 applying. If your part is a regulated medical device, ISO 13485 is the baseline buyers must see, and we can show the certificate plus the audit trail.
A: We target a 7-day first article from drawing to sample for many programs and accept low-MOQ or single-piece prototypes, scaling to 500,000 parts/month in volume. Book a free DFM review before PO to shorten it.
Ready to move your program forward? Send us your drawing and we will return a free DFM review with the real achievable tolerance, lead time and unit-price curve for your part — no commitment required.
Request a Free CNC Quote