Quick-Swap CNC Fixtures: Why Gripper Jaws Win for Industrial Automation Parts (2026)
If your robot cell loses three minutes every time you swap a part family, you are not buying downtime - you are buying a tax on every batch you ever run. Across a two-shift line that changeover tax quietly eats 8 to 12 percent of available capacity before a single defective part appears. The buyers we talk to have started treating the fixture, not the spindle, as the real bottleneck.
In this guide we walk through why quick-swap CNC fixtures and properly machined gripper jaws have become the default answer for industrial automation parts lines, what the trade-offs actually are between hardened and soft jaws, and how tolerance stack-up is controlled so the tenth part is as true as the first. We also give you a buyer's checklist you can hand to any shop tomorrow.
We have been a Dongguan source factory for precision CNC work since 2015, running 60 machines on a 4,000 sqm floor with monthly output around 500k parts. This is written from the bench - the numbers below are the ones we argue about with customers before a single chip is cut, not catalog copy.
Table of Contents
- 1. Why Quick-Swap CNC Fixtures Save Industrial Automation Parts Lines
- 2. How Gripper Jaws Work: A Fixture Machining Walkthrough
- 3. Hardened vs Soft Quick-Change Jaws: A Precision Brackets Comparison
- 4. Aluminum 6061 Machining for Lightweight Gripper Bodies
- 5. Tolerance Stack-Up in CNC Fixtures and How We Control It
- 6. Custom CNC Parts vs Standard Jaws: Which Should You Specify?
- 7. Fixture Machining Process: 3 Steps from Drawing to Swap-Ready Jaw
- 8. Buyer's Checklist: What to Demand from Precision Brackets and Fixtures
- 9. Industrial Automation Parts Sourcing: Choose Standard If / Choose Custom If
Industrial Automation AI part image
Why Quick-Swap CNC Fixtures Save Industrial Automation Parts Lines
The fixture is the bottleneck you forgot you had.
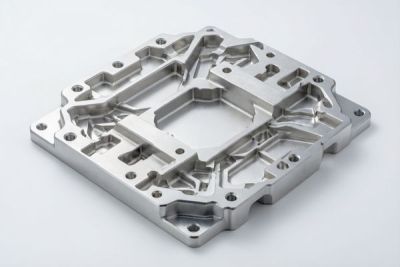
A traditional changeover means unbolting a fixture, re-indicating it to the machine datum, proving repeatability with a first-article check, and only then running. On a manual setup that is 20 to 45 minutes of lost spindle time per family. A quick-swap CNC fixture replaces that with a base plate that stays indicated and a jaw or sub-plate that drops into a known location within 0.005 mm. The robot keeps running while the operator swaps the part-specific element.
- Quick-swap fixture
- A permanent base (sub-plate or riser) that stays clamped and indicated on the machine, plus interchangeable jaw/insert elements that locate to the base through hardened pins or a zero-point clamp system.
- Re-indication
- The act of re-proving a fixture's position relative to the machine coordinate system after it has been removed and refitted - the step quick-swap is designed to eliminate.
What quick-swap actually buys you
Three things, in order of value: (1) recovered spindle hours, (2) removed re-indication error, and (3) a repeatable datum the quality team can trust across shifts. For a cell running six part families a day, recovering even 15 minutes per swap is a full extra shift per week of capacity.
| Step | Manual fixture | Quick-swap CNC fixture |
|---|---|---|
| Swap time | 20-45 min | 1-3 min |
| Re-indication needed | Yes, every swap | No - base stays indicated |
| Datum reset error | 0.01-0.03 mm risk | Below 0.005 mm by design |
| First-article re-prove | Every family | Only on new jaw element |
| Capacity recovered | None | 8-12% of line time |
Industrial Automation AI part image
How Gripper Jaws Work: A Fixture Machining Walkthrough
A jaw is a fixture you hold in your hand - treat it like one.
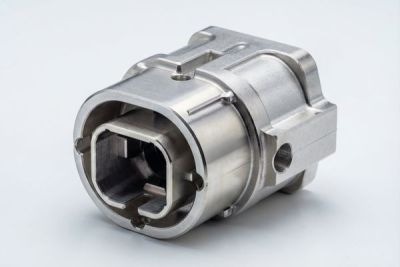
A gripper jaw looks simple: a block with a serrated or contoured face that the robot finger squeezes. But the moment it touches a part it becomes part of your fixture chain, and every micron of jaw error becomes part of the part's position error. That is why fixture machining of jaws is worth the same rigor as the fixture itself.
- Fixture machining
- The discipline of cutting fixture elements - jaws, bushes, nests, locators - to controlled datums so they repeatably position the workpiece, not just hold it.
The three-stage path from drawing to swap-ready jaw
- Design the datum: decide which feature of the jaw locates to the base and which face contacts the part. Get this wrong and the jaw is 'tight' but never repeatable.
- Machine the jaw: cut the locators first on the known datum, then the contact contour, holding the contact face to the tolerance the gripper needs - we hold +/-0.005 mm on the locate features.
- Balance and prove: lighten the jaw so it does not throw the robot wrist off-balance, then prove repeatability on a CMM or a pin-gauge stack before it ever reaches the cell.
We machine jaws on the same turn-mill and 5-axis centers we use for flight-critical work, because a jaw that drifts 0.02 mm turns into a dropped part on cycle 50,000. The grip face is often taken to Ra 0.8 micro m so it bites without marking a finished surface, and where the part is delicate we add a relief pocket so only the intended lands touch.
Hardened vs Soft Quick-Change Jaws: A Precision Brackets Comparison
The material choice decides who pays for wear - you or the jaw.
Quick-change jaws come in three practical flavors, and they are not interchangeable. Hardened steel jaws are permanent and precise but cannot be contoured to a soft part without marking it. Aluminum soft jaws are machined to the part every time the family changes, so they are gentle but consumable. PEEK or acetal jaws are for fragile or scratch-sensitive parts and give up almost all grip pressure.
| Property | Hardened steel jaw | Aluminum 6061 soft jaw | PEEK / acetal jaw |
|---|---|---|---|
| Grip pressure | High | Medium | Low |
| Part marking risk | High on soft parts | Low | None |
| Re-machine per family | No | Yes (mill to part) | Sometimes |
| Wear life | Years | Hundreds of cycles | Dozens of cycles |
| Best for | Rigid steel parts | Most automation lines | Glass, anodized, medical |
Pros
- Hardened jaws hold datum for years with no re-cut
- Soft aluminum jaws contour to any part in minutes
- PEEK protects scratch-sensitive surfaces
Cons
- Hardened jaws mark soft parts
- Soft jaws are a consumable you must re-machine
- PEEK gives up grip and costs more per jaw
Industrial Automation AI part image
Aluminum 6061 Machining for Lightweight Gripper Bodies
A heavy jaw is a robot you are paying to lift nothing.
Every gram on the gripper finger is mass the robot wrist must accelerate and decelerate thousands of times a shift. Aluminum 6061 machining is the default for gripper bodies and soft jaws because it is light, stable, and easy to hold to tight tolerances. We run 6061-T6 for the bulk of bodies and step to 7075-T6 only where yield strength at the finger root matters.
| Alloy | Use it for | Watch out for |
|---|---|---|
| 6061-T6 | Gripper bodies, soft jaws, brackets | Lower strength vs 7075 |
| 7075-T6 | High-stress finger roots, arms | Corrosion; anodize advised |
| 2024-T3 | Fatigue-critical (rare in jaws) | Poor corrosion resistance |
We anodize most gripper bodies - Type II for a durable matte finish that hides handling marks, Type III hard coat where the finger sees abrasion. Anodize adds a few microns and can close a 0.005 mm slot, so we machine bores undersize and let the coating bring them to nominal. Miss that and the finger pivot binds on assembly.
Tolerance Stack-Up in CNC Fixtures and How We Control It
Tolerance is a budget - and the fixture spends most of it.
Position error on a gripped part is the sum of base-locate error, jaw-locate error, jaw-contact error, and part-feature error. Each link adds. A fixture that is +/-0.01 mm at the base and a jaw that is +/-0.01 mm at the contact can hand the robot a part that is +/-0.02 mm off true - before the machining tolerance is even considered. The fix is to spend the budget where it matters and relax it where it does not.
| Link in the chain | Our target | Why it matters |
|---|---|---|
| Base-to-machine locate | +/-0.005 mm | Stays fixed for every family |
| Jaw-to-base locate | +/-0.005 mm | Repeatable across swaps |
| Jaw contact face | Ra 0.8 um, +/-0.01 mm | Grip, not position, here |
| Part feature (machined) | per your drawing | Only this is 'the part' |
We prove the chain with a CMM first-article on the jaw element and a pin-gauge stack on the assembled base, then audit in process so a worn locator shows up before a bad lot ships. Lot traceability runs from the raw bar to the finished jaw.
- Spend the tight tolerance on base and jaw locate features
- Relax the contact face to grip-spec, not position-spec
- CMM first-article on the jaw, not just a photo
- Lot traceability from raw bar to finished jaw
- Re-audit after any locator repair
Industrial Automation AI part image
Custom CNC Parts vs Standard Jaws: Which Should You Specify?
Buy standard until a standard jaw costs you more than a custom one.
Off-the-shelf gripper jaws are cheap and fast, and for round or rectangular parts they are the right call. The moment your part is thin-walled, oddly shaped, or scratch-sensitive, a standard jaw starts costing you in scrap and re-work. That is the line where custom CNC parts - a jaw machined to your exact part - pay for themselves.
| If your part is... | Specify | Why it wins |
|---|---|---|
| Round or rectangular, rigid | Standard jaw | Cheapest, fastest |
| Thin-walled or delicate | Custom soft jaw | Relief lands stop distortion |
| Scratch-sensitive (anodized, glass) | Custom PEEK jaw | Zero marking |
| High mix, low volume | Standard + quick base | Swap families in minutes |
| One shape, 100k+ / yr | Custom hardened jaw | Datum lasts for years |
Fixture Machining Process: 3 Steps from Drawing to Swap-Ready Jaw
A jaw is only swap-ready if its datum is proven, not assumed.
- Release the drawing on the jaw's own datum: locate features, contact lands, and the finger interface all called out so the jaw is swappable independent of finger wear.
- Machine on a known datum: cut locators first, then contact contour, holding +/-0.005 mm on locate features; take the grip face to Ra 0.8 micro m and passivate per ASTM A967 if the jaw is stainless.
- Prove and register: CMM the locate features, balance the mass, and register the jaw to its base with a pin-gauge stack so the next operator just drops it in.
Where fixture machining meets the robot
The jaw's finger interface must match the gripper standard your cell uses - most are a simple tongue-and-slot or a dowel pattern. We machine that interface to the robot maker's print so the jaw seats the same way every time, which is the whole point of quick-swap. A jaw that needs 'persuasion' to seat is not swap-ready.
Industrial Automation AI part image
Buyer's Checklist: What to Demand from Precision Brackets and Fixtures
Hand this to a supplier and the tire-kickers disappear.
Sourcing precision brackets and quick-swap fixtures is less about finding a cheap machine and more about finding a shop that understands repeatability, not just shape. The list below is what we are happy to answer with data, and it is what separates a real precision source from a broker with a logo.
- Cert stack: ISO 9001 minimum; ISO 13485 or IATF 16949 a plus for medical or auto-adjacent lines
- Jaw drawn on its own datum, not just 'make it fit the finger'
- Locate features held to +/-0.005 mm, with CMM proof
- Material cert traceable to the heat lot (6061-T6 / 7075-T6 / 17-4PH)
- Coated vs bare tolerances agreed before quoting (anodize grows bores)
- Lot traceability from raw bar to finished jaw
- A re-work path when a locator wears, not a 'buy a new one' shrug
The cheapest jaw is the one that passes qualification the first time - because the second time costs you a launch date.
Industrial Automation Parts Sourcing: Choose Standard If / Choose Custom If
The decision is a line on a scrap report, not a philosophy.
When you source industrial automation parts like gripper jaws and precision brackets, the standard-versus-custom call comes down to one question: is a standard jaw already costing you money? If the answer is no, do not over-engineer. If yes, a custom CNC jaw is the cheaper part by the time you count re-work.
- Choose a STANDARD jaw if: your part is rigid and round/rectangular, volume is steady, and scrap from grip marks is near zero.
- Choose a CUSTOM soft jaw if: you re-machine standard jaws to fit, or you reject parts on distortion and marking.
- Choose a CUSTOM hardened jaw if: one shape runs 100k+/year and you want a datum that lasts for years.
- Choose a CUSTOM PEEK jaw if: the part is glass, anodized, or medical and cannot take a mark.
- Choose a QUICK-SWAP BASE if: you run more than three families a day and changeover is stealing capacity.
For Dongguan Licun Technology, the pattern is consistent: most lines start on standard jaws plus a quick-swap base, then move the problem families to custom jaws as volume and scrap teach them where the money is. You do not have to decide everything on day one.
Industrial Automation AI part image
Industrial Automation AI part image
Industrial Automation AI part image
Industrial Automation AI part image
FAQ: industrial automation parts & Industrial Automation Buyer Questions
A: It is a permanent base plate that stays clamped and indicated on the machine, plus interchangeable jaw or sub-plate elements that locate to the base within 0.005 mm through hardened pins or a zero-point clamp. It matters because it removes the 20-45 minute re-indication step on every changeover, recovering 8-12 percent of line capacity.
A: Use hardened steel jaws for rigid parts where grip pressure is high and marking is not a concern - they hold datum for years. Use aluminum 6061 soft jaws for most automation lines because they contour to the part in minutes and protect finished surfaces; they are consumable but cheap to re-machine. Use PEEK only for fragile or scratch-sensitive parts.
A: Hold the jaw-to-base locate features to +/-0.005 mm and prove them on a CMM; relax the contact face to a grip spec like Ra 0.8 micro m and +/-0.01 mm. Over-tolerancing the contact face just wastes budget you need at the locate face, which is what actually controls part position.
A: Yes. Type II adds a few microns and Type III hard coat adds more; either can close a 0.005 mm slot or bind a press-fit pivot. Always machine bores undersize by the coating thickness so the finished, coated dimension lands at nominal. Designing to the bare condition is the classic mistake that causes binding on assembly.
A: When you are already re-machining a standard jaw to fit your part, or rejecting parts on distortion or grip marks. Standard jaws win for rigid round or rectangular parts at steady volume; custom jaws win the moment scrap or re-work from a poor grip starts costing more than the jaw itself.
A: Yes. We provide material certs traceable to the heat lot (6061-T6, 7075-T6, 17-4PH), a CMM first-article report on the jaw's locate features, lot-level traceability from raw bar to finished part, and a re-work path when a locator wears. Our floor runs ISO 9001 certified with ISO 13485 completed and IATF 16949 in application.
Send us your gripper jaw or fixture drawing for a free DFM review - we will flag whether a standard jaw plus a quick-swap base is enough, which families should move to custom CNC jaws, and the tolerances that are quietly costing you capacity. Reach out and let's cut the first article.
Request a Free CNC Quote