LusterControl Expands Threaded Inserts Capacity for Automotive & EV (2026)
LusterControl has expanded its precision threaded insert capability for automotive and EV clients, adding capacity and process depth at its Dongguan source factory. The move targets rising demand for durable, repeatable threads in aluminum battery-pack enclosures, sensor housings, charging-connector bodies and busbar mounts, where a stripped or loosening insert does not just mean a rattling cover, it can open a coolant path, break a service seam or fail a torque-to-yield check at the worst moment on the line.
For buyers, the practical upside is direct: one accountable partner that takes your threaded insert from raw bar or blank to finished, inspected, lot-traceable part, without the handoffs between turning, finishing and inspection that quietly add cost, lead time and fit risk on a component most engineers treat as a commodity until it strips.
This piece is written from the buyer's seat. We explain why the threaded insert, not the big casting, often decides whether an EV assembly stays sealed and serviceable across its life, what real specifications to demand, and how to avoid the sourcing mistakes that turn a strong-looking insert into a field failure nobody expected.
Table of Contents
- 1. Why Threaded Inserts Decide Assembly Strength in Automotive & EV
- 2. Automotive and EV CNC Parts: Capacity Expansion in 2026
- 3. How Threaded Inserts Lock Components: A Buyer's View
- 4. CNC Precision Machining Behind Precision Threaded Inserts
- 5. Tight Tolerance CNC: How We Hold +/-0.005 mm on Threaded Inserts
- 6. Custom CNC Parts: Choosing the Right Threaded Insert Build
- 7. Buyer's Checklist for Automotive and EV CNC Parts and Threaded Inserts
- 8. Common Mistakes When Sourcing Threaded Inserts
- 9. Quality Framework Behind Automotive and EV CNC Parts
- 10. Real Custom CNC Parts We Have Shipped
- 11. Protecting Your Design: NDA for Automotive and EV CNC Parts
Automotive&EV CNC precision component
Why Threaded Inserts Decide Assembly Strength in Automotive & EV
The smallest fastening detail often holds the whole stack together.
An automotive or EV assembly is only as serviceable as the threads it relies on. The seat that holds a coolant-cover collar, the insert that anchors a sensor bracket to a cast-aluminum housing, the bushing that lets a charging-plug body be torqued and re-torqued, and the heat-set insert that locks a plastic module to a metal frame all pass through a precision threaded insert. If the insert's internal thread form, outer grip geometry and the host bore or molding are not held to a tight, repeatable budget, the joint loosens between units and your part either rattles after vibration testing or fails the torque audit at the line.
- Threaded inserts
- Bushings or sleeves that create durable, repeatable internal threads in a softer host material or reinforce threads in metal. In automotive and EV they provide torque-resistant fastening into aluminum castings, plastic housings and composites, but only if the insert geometry, grip feature and host bore are held to spec together.
- Automotive and EV CNC parts
- Precision machined components built into battery packs, sensor housings, charging hardware, busbars and structural mounts. These parts are made to vibration, thermal-cycle and torque-retention standards with little tolerance for fit, finish or batch drift across a vehicle program.
For a program buyer the lesson is direct: the threaded insert specification, not the colorful housing, often decides whether a bracket stays torqued across a production lot or whether a sensor seat holds on unit 1 and strips on unit 5,000 after a summer of thermal cycling. An insert held to +/-0.01 mm on its grip diameter instead of +/-0.03 mm resists pull-out; a poorly formed internal thread strips under a rated fastener. Insert discipline is the cheapest insurance you can spec up front.
Automotive&EV CNC precision component
Automotive and EV CNC Parts: Capacity Expansion in 2026
One plant, one quality record, one accountable partner.
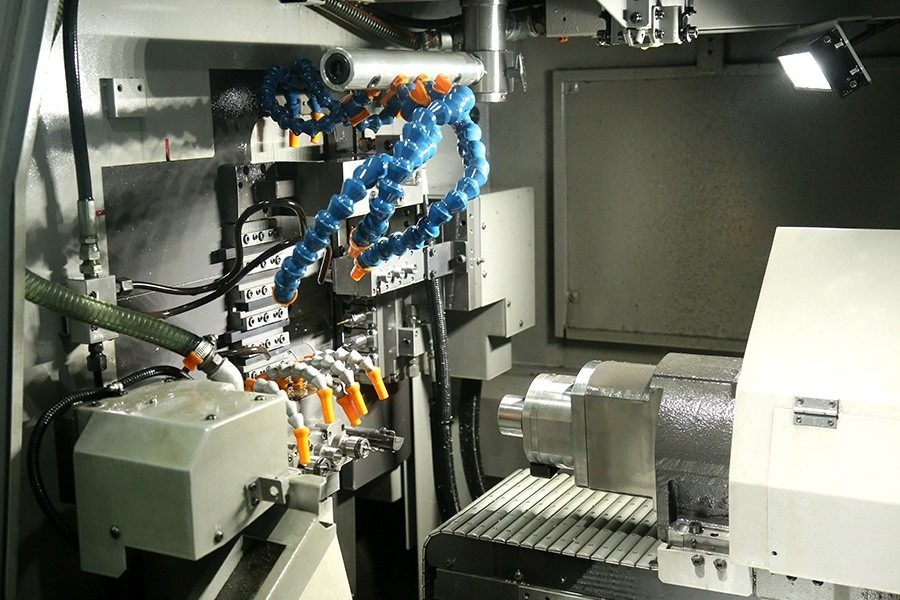
LusterControl's Dongguan plant spans 4,000 m2, expanded in 2026, with the old 2,000 m2 footprint retired, and ships 500,000 parts per month. The automotive and EV threaded insert line runs on Swiss-type turning, turn-mill composite and 5-axis cells that cut setups and stack-up error, plus in-house mirror and electropolishing so the part leaves finished, not half-done. For background on the factory and certifications, see our company profile.
- In-house turning, milling, 5-axis, mirror and electropolishing, no outsourced plating or polish handoffs.
- CMM first-article data on every new print, not a verbal promise.
- Lot traceability back to material batch and machine for fast root cause.
- Low-MOQ prototypes to de-risk a new threaded insert before volume.
How Threaded Inserts Lock Components: A Buyer's View
An insert is only as good as the host it lives in.
A threaded insert works by gripping a host bore or molded pocket and presenting a clean, repeatable internal thread to the fastener. The buyer's job is to specify the whole system, not just the insert. A brass heat-set insert is useless if the molded hole is oversized, and a press-in steel insert strips the host if the bore is undersized or out of round. Below is how the parts interact, and what each dimension does for your assembly.
| Feature | What it controls | Why it protects the assembly |
|---|---|---|
| Internal thread form | Fastener engagement and stripping torque | Stops the screw pulling the thread under rated load. |
| Outer grip geometry | Resistance to pull-out and rotation | Prevents the insert backing out under vibration. |
| Host bore / molded pocket | Seat squareness and concentricity | Keeps the insert straight and seated after thermal cycles. |
| Insert length and wall | Load spread into the host | Lets the joint survive repeated torquing and service. |
Step 1, Specify the host geometry, not just the insert
We verify the host bore or molded pocket against the insert standard and run a CMM first article on both the insert and a sample host before any volume runs. For stainless 304, 316L, 17-4PH and brass inserts this also sets the baseline for surface finish and passivation later in the chain, so the grip and thread faces are measured against a known reference, not a hope.
Step 2, Cut the insert and seat in one setup where possible
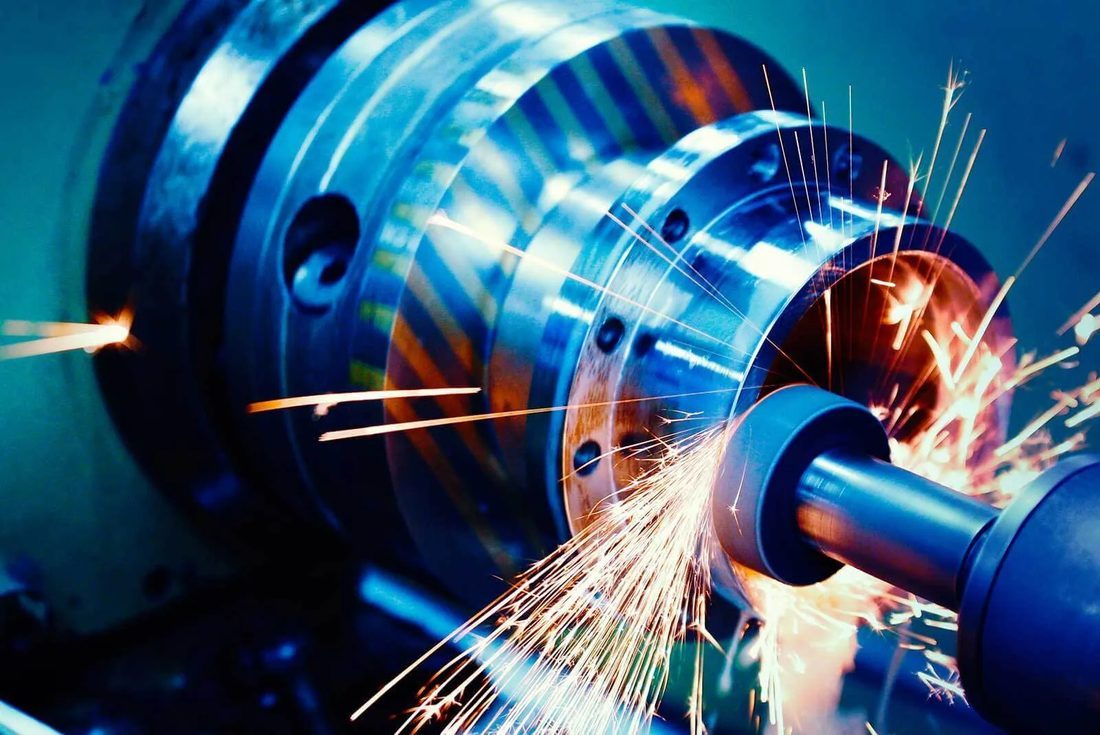
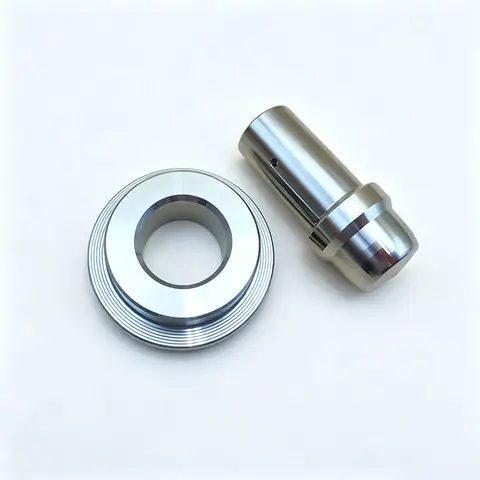
Holding the insert OD, the thread form and the seating datum in one setup is what lets us hold +/-0.005 mm and keep faces parallel within microns. Swiss-type turning is the workhorse for small cylindrical inserts; turn-mill composite is used for inserts with integrated flanges; 5-axis lets contoured or slotted inserts be cut without re-clamping, which is exactly where stack-up error usually sneaks into a precision threaded insert.
Step 3, Finish, deburr and passivate
Standard mirror finishing reaches Ra 0.6 micrometer; the top end reaches 8K mirror at Ra 0.2 micrometer. We follow ASTM A967 for electropolish and passivation so the insert stays burr-free and corrosion-resistant in a part that may live under hood heat, road salt and battery-pack humidity. You can read more on our process approach at the LusterControl blog.
Automotive&EV CNC precision component
CNC Precision Machining Behind Precision Threaded Inserts
An insert is only as good as the chain that made it.
CNC precision machining for a precision threaded insert is less about one magic cut and more about a disciplined chain: incoming material verification, DFM-driven fixturing, single-setup Swiss-type turning or turn-mill to protect the thread form and grip, 5-axis for slotted or contoured inserts, then mirror or electropolishing for a clean, burr-free surface that will not gall a fastener. Each step exists to protect the next.
- Verify the bar, blank or screw stock cert, grade and heat lot before cutting.
- Run a CMM first article on the insert and a sample host seat.
- Cut in a single setup to remove re-clamp error on the thread form.
- Mirror finish to Ra 0.6 micrometer, top end 8K at Ra 0.2 micrometer.
- Passivate to ASTM A967 and package for clean transfer to assembly.
Tight Tolerance CNC: How We Hold +/-0.005 mm on Threaded Inserts
Tolerance is a process decision, not a number on a drawing.
A tight tolerance CNC threaded insert lives or dies on how the tolerance is distributed. An internal thread at +/-0.01 mm only helps if the outer grip diameter it presses into is held to the same budget and the seating face is cut in the same setup. Below is how we map tolerance to the features that actually protect joint retention in an automotive or EV assembly.
| Feature | Held tolerance | Why it protects the assembly |
|---|---|---|
| Internal thread form | +/-0.01 mm | Repeatable fastener engagement, no stripping. |
| Outer grip diameter | +/-0.005 mm | Predictable press-in and pull-out resistance. |
| Seating face flatness | +/-0.01 mm | Square seat, no tilt under torque. |
| Insert length | +/-0.02 mm | Repeatable load spread into the host. |
| Surface finish on grip | Ra 0.4 micrometer | Clean contact, no galling, no particle traps. |
- Fix the thread form, grip diameter and seat in one setup to remove re-clamp error.
- Run SPC/CPK on grip diameter and thread form, not just spot checks.
- Verify every batch on CMM against the first-article baseline.
- Passivate to ASTM A967 so the insert survives hood and pack environments.
Automotive&EV CNC precision component
Custom CNC Parts: Choosing the Right Threaded Insert Build
Match the build to volume, material and risk, not to habit.
Most custom CNC parts decisions for precision threaded inserts come down to three build paths: Swiss-type turning for small cylindrical inserts, turn-mill composite for flanged or integrated inserts, and 5-axis milling for slotted or contoured inserts. The table below turns that into a buyer decision rather than a spec sheet.
| Your program need | Recommended build | Why it wins |
|---|---|---|
| Small cylindrical insert, high volume | Swiss-type turning | Best diameter control, lowest per-part cost at scale. |
| Flanged one-piece insert, tight faces | Turn-mill composite | Both faces and thread in one setup, no flatness handoff. |
| Slotted or contoured insert | 5-axis milling | Cuts complex features without re-clamping and stack-up error. |
| Low-MOQ prototype before volume | Swiss-type or turn-mill | Fast first article, then scale on the same process. |
- Choose Swiss-type turning if your insert is small, round and you need volume cost down.
- Choose turn-mill composite if a flat, seated face and a tight thread are the whole point of the part.
- Choose 5-axis if the insert is slotted, contoured or angled and re-clamping would add error.
Buyer's Checklist for Automotive and EV CNC Parts and Threaded Inserts
Five things to demand before you release the drawing.
For automotive and EV CNC parts the gap between a good threaded insert and a joint that strips is usually paperwork you never asked for. Use the checklist below as your release gate.
- Material certificate with grade and heat lot, not just 'stainless' or 'brass'.
- CMM first-article report tied to your drawing revision, insert and host seat.
- Grip diameter AND host bore spec, not just the internal thread.
- Lot traceability back to material batch and machine.
- Passivation to ASTM A967 for corrosion resistance under hood and pack.
- Red flag: certs sent later, certs travel with the batch, not after.
- Red flag: thread quoted with no host bore callout.
- Red flag: finish quoted as a word, not a measured Ra number.
Automotive&EV CNC precision component
Common Mistakes When Sourcing Threaded Inserts
The failures are predictable, and avoidable.
- Specifying finish as 'polished' instead of a measured Ra, you get whatever the shop feels like.
- Splitting turning and finishing across two vendors to save a few cents, then owning the fit path.
- Skipping lot traceability to move faster, then having no root cause when an insert pulls out.
- Quoting thread form on one feature but ignoring how it stacks against the host bore.
- Choosing the cheapest passivation that is not ASTM A967 compliant in the service environment.
None of these are exotic. They are the routine shortcuts that turn a precision threaded insert into a rework line item on a vehicle program. Ask the five questions in the checklist above and most of them disappear.
Quality Framework Behind Automotive and EV CNC Parts
Proof beats promises, here is the chain.
For program buyers, the discipline behind +/-0.005 mm matters more than the number itself. LusterControl runs a staged chain: DFM review, incoming material check, first-article CMM, in-process SPC/CPK, final FQC/OQC and lot traceability. That is what lets us stand behind ISO 9001 certified, ISO 13485 completed and IATF 16949 applying controls on every threaded insert.
- First-article CMM data on every new print before volume.
- SPC / CPK on special characteristics, not spot checks.
- Lot traceability back to material and machine for fast root cause.
- Material certs and passivation records on every batch.
Automotive&EV CNC precision component
Real Custom CNC Parts We Have Shipped
Same model, applied to your threaded insert.
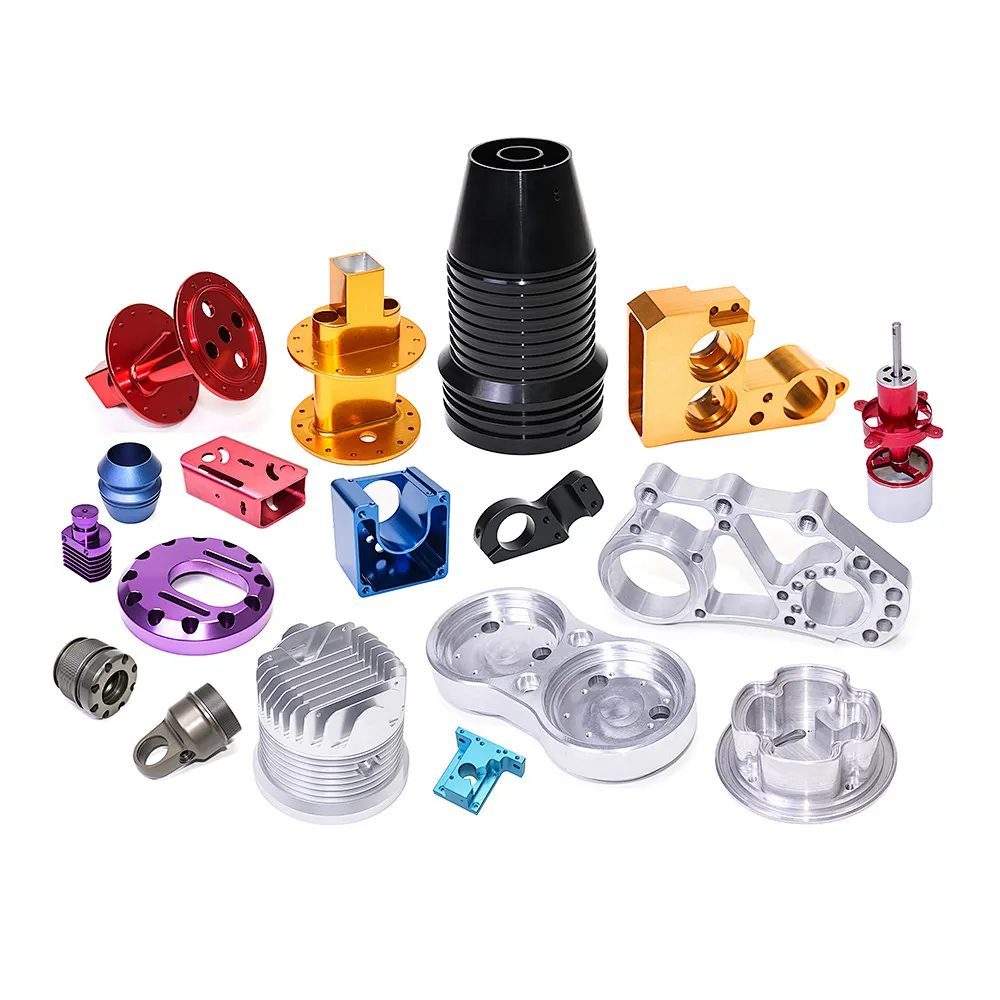
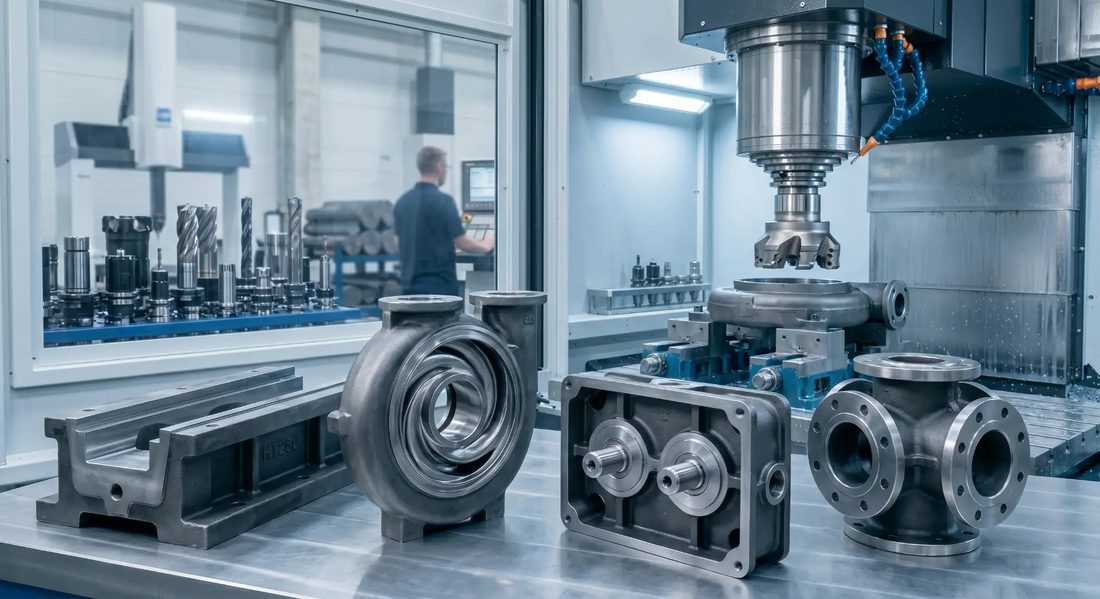
For your precision threaded inserts, the same model applies: turning, milling, 5-axis, mirror/electropolishing and inspection in-house, one quality record. Request a free DFM review and we will show it on your drawing.
Protecting Your Design: NDA for Automotive and EV CNC Parts
A leaked drawing travels faster than a purchase order.
For EV platform teams, Tier suppliers and R&D groups especially, releasing a threaded insert or housing drawing to three shops triples the exposure of your design. LusterControl runs customer-NDA programs and handles CAD files on controlled access, so your insert and bracket designs stay yours.
- NDA-backed programs for De'Longhi, Donlim and Breville-grade work.
- Controlled CAD access, no re-use or re-sale of your design.
- Discreet international packaging for prototype shipments.
Automotive&EV CNC precision component
Automotive&EV CNC precision component
Automotive&EV CNC precision component
FAQ: threaded inserts & Automotive&EV Buyer Questions
A: Yes. Turning, milling, 5-axis, mirror/electropolishing and inspection are all in-house across our 4,000 m2 Dongguan plant with 60 CNC machines.
A: We hold +/-0.005 mm on outer grip diameter and +/-0.01 mm on internal thread form and seating face, cut in a single setup to control stack-up.
A: ISO 9001 certified, ISO 13485 completed and IATF 16949 applying. We provide material certs, CMM first-article data and lot traceability on every batch.
A: Standard mirror finishing reaches Ra 0.6 micrometer and the top end reaches 8K mirror at Ra 0.2 micrometer, followed by electropolish and passivation per ASTM A967 to resist corrosion under hood and pack environments.
A: Yes. NDA-backed programs are routine for us, including De'Longhi, Donlim and Breville-grade work, with controlled CAD access and discreet prototype packaging.
A: We target a fast first article from drawing to sample for many programs and accept low-MOQ prototypes, then scale to 500,000 parts per month in volume.
Want the same precision on your next threaded insert? Send LusterControl your drawing and our engineering team will return a free DFM review with achievable tolerance and lead time.
Request a Free CNC Quote