Trade Show Recap: What Precision Buyers Asked LusterControl in 2026
You walk a trade-show aisle with a drawing in your hand and a launch date behind you. At every booth the same pitch lands: 'tight tolerance, fast lead time, great price.' By booth nine the words blur. What actually separates a shop that will protect your program from one that will quietly cost you a quarter? The buyers who stopped at our booth in 2026 asked sharper questions than that — and the pattern of those buyer questions tells you exactly what a serious sourcing engineer checks before the PO goes out.
This is a recap, but it is written from your side of the table. We have taken the most common CNC precision machining and stainless steel mirror finishing questions global OEM buyers asked LusterControl (Dongguan Licun Technology Co., Ltd.) this year and turned them into a reference you can keep open during your own supplier evaluations. No brochure language — just the questions that matter and the honest answers behind them.
Use it as a checklist for your next audit. Every number below is a real LusterControl fact: 15 years of CNC lathe work since 2015, 60+ machines, 4,000 m² of floor, 500K parts a month, ISO 9001 held, ISO 13485 completed, IATF 16949 in progress, and Ra 0.2 µm 8K mirror finishing on stainless. The goal is to help you ask better buyer questions of every supplier you meet — including us.
Table of Contents
- 1. The Buyer Questions LusterControl Heard Most at 2026 Trade Shows
- 2. CNC Precision Machining Tolerances Buyers Probe at the Booth
- 3. Stainless Steel Mirror Finishing: The Specs Buyers Asked About
- 4. How Global OEM Buyers Evaluate a Dongguan Source Factory
- 5. LusterControl News From the 2026 Floor: 15 Years of CNC Lathe Work
- 6. Buyer Questions on Quality Certification: ISO 9001, ISO 13485, IATF 16949
- 7. CNC Precision Machining Capacity: 60+ Machines, 500K Parts a Month
- 8. Stainless Steel Mirror Finishing Specs Global OEM Buyers Should Request
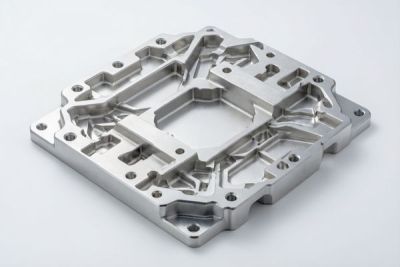
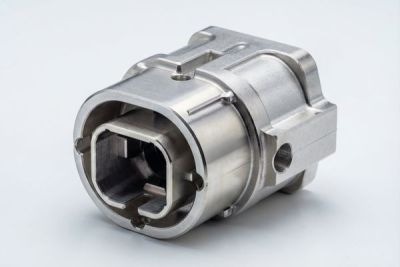
Company AI part image
The Buyer Questions LusterControl Heard Most at 2026 Trade Shows
A booth is the fastest supplier audit you will ever run.
A trade-show booth compresses a supplier audit into ninety seconds. You cannot see the floor, but you can hear how a shop answers. The buyer questions we heard most in 2026 were not 'what is your price' — they were 'how do you prove it.' That shift alone separates a mature sourcing engineer from a reactive one. The questions below recurred across every industry we serve: medical, automotive, aerospace, robotics, semiconductor, and coffee-machine OEMs.
Why the booth question pattern predicts the audit result
Engineers who ask 'show me the calibration log' at the booth are the same engineers who demand a First Article Inspection report before volume. The question pattern is a proxy for procurement discipline. If a supplier fumbles the easy booth question, the hard floor audit will not go better. We started logging these buyer questions because the same five themes showed up in Dongguan, in Stuttgart, and online — a global OEM buyer asks the same things whether the part is a titanium bracket or a brass brew chamber.
The recurring buyer questions clustered into four themes: tolerance proof, surface-finish specs, global OEM evaluation, and quality certification. The next sections answer each one the way we answered it at the booth — with the document or the number, not the adjective.
Company AI part image
CNC Precision Machining Tolerances Buyers Probe at the Booth
Tolerance is the first word out of a serious buyer's mouth.
- Tolerance
- The permitted deviation from a drawing dimension. On a precision part, ±0.005 mm means the feature may sit five thousandths of a millimetre either side of nominal — about one-tenth the width of a human hair.
- Geometric tolerance
- Tolerance on shape and relationship (flatness, concentricity, position), not just size. This is what holds a stack of features aligned across a multi-face part.
The single most-asked CNC precision machining question in 2026 was a version of: 'You say ±0.005 mm — how do you hold it on the 5,000th part at 2 a.m.?' The honest answer is process discipline, not operator skill. Turn-mill compound, 5-axis, and Swiss-type turning each control a different source of error, and the booth buyer who understood that was the one who left with a qualified vendor.
The ±0.005 mm question, answered with process
Turn-mill compound holds tolerance by eliminating re-fixturing — the biggest source of stack-up on stepped shafts and housings. 5-axis holds inter-feature relationships by cutting multi-face geometry in fewer setups. Swiss-type turning supports slender, small-diameter parts right at the cut so diameter and length stay stable at volume. A supplier who cannot name which process your part runs on is a supplier who cannot trace the tolerance they promised.
| Process | Best for | Tolerance strength |
|---|---|---|
| Turn-mill compound | Stepped shafts, housings | Minimal re-fixturing stack-up |
| 5-axis CNC | Contoured, multi-face parts | Tight inter-feature relationships |
| Swiss-type turning | Slender small parts, high volume | Stable diameter/length at scale |
| Mirror / electrolytic polish | Ra ≤0.6 µm, up to 8K Ra 0.2 µm | Surface, not geometry tolerance |
What 'tight tolerance' really costs you if unproven
An unproven tolerance claim costs more than scrap. You absorb incoming inspection, expedited rework, line-down penalties, and field failures that trace back to your supply chain. For medical, automotive, or aerospace programs the compliance exposure can end a contract. The booth question that screens this out is simple: 'show me the First Article Inspection report, not the certificate of conformance.'
For a deeper look at how process choice drives tolerance, see our ±0.005 mm tolerance deep-dive and the 5-axis and turn-mill capability map. Both show the documentation a mature shop keeps ready.
Stainless Steel Mirror Finishing: The Specs Buyers Asked About
Finish is where coffee-machine and medical buyers live or die.
- Mirror finishing
- A surface process that removes micro-scratches to a reflective, low-roughness state measured in Ra (roughness average, micrometres). Lower Ra means smoother.
- 8K mirror
- The highest common polish grade, reaching Ra 0.2 µm on stainless — a near-optical, fingerprint-resistant surface used where cleanability and sealing matter.
Stainless steel mirror finishing was the second theme in our 2026 buyer questions, and it splits cleanly by industry. Coffee-machine and medical buyers cared about cleanability and seal performance; decorative buyers cared about looks. The booth buyers who knew the difference asked for the Ra number, not the word 'mirror.'
| Finish grade | Roughness (Ra) | Where it earns its cost |
|---|---|---|
| Standard machined | Ra ~1.6 µm | Internal, non-contact features |
| Standard mirror | Ra ≤0.6 µm | Food / medical contact, seals |
| 8K mirror | Ra 0.2 µm | Premium appliances, optical-adjacent, cleanability-critical |
| As-machined vs polished | Depends on process | Polish adds cost only where spec demands |
When you actually need 8K, and when you do not
You need 8K when the surface is in contact with fluid, food, or a sealing face, or when cleanability is a compliance requirement. You do not need 8K on a hidden bracket — and paying for it there is the classic overspec that a good supplier will flag for you. A booth buyer who asks 'do I need 8K here?' is signaling they trust their supplier to save them money, not inflate the quote.
Electrolytic polishing vs mechanical mirror
Electrolytic (electropolishing) levels the surface chemically and improves corrosion resistance on stainless; mechanical mirror polishing hits the low Ra but can leave directional grain. For medical and fluid-control parts, electropolishing plus ASTM A967 passivation is the combination buyers asked about most. LusterControl runs both under one ISO 13485 system, so the finish and the corrosion-control cert come from the same quality record.
| Method | Best result | Buyer caveat |
|---|---|---|
| Mechanical mirror polish | Low Ra, bright look | Directional grain; verify Ra on the print |
| Electropolishing | Smooth + corrosion-resistant | Pair with ASTM A967 passivation cert |
| Combined process | Ra 0.2 µm + passivated | One quality record, one cert stack |
See our 8K mirror finishing guide for the full comparison. The booth takeaway: ask for the Ra number and the passivation cert, not the adjective.
Company AI part image
How Global OEM Buyers Evaluate a Dongguan Source Factory
A Dongguan source factory is judged by documents, not distance.
Global OEM buyers do not evaluate a Dongguan source factory differently because of where it sits — they evaluate it by the same document discipline they demand at home. The 2026 buyer questions on this theme were about traceability, cert scope, and volume proof. A mature South China source factory answers all three with paperwork, not promises.
The three documents global OEMs ask for first
- Valid ISO 9001 certificate with scope statement and expiry — proves a documented, repeatable system, not a lucky operator.
- Program-matched certificates: ISO 13485 for medical, IATF 16949 roadmap for automotive, ASTM A967 passivation per lot for stainless.
- Incoming-material batch traceability ID linking every part to its raw-material mill test report and inspection record.
| Evaluation item | What a global OEM checks | Red flag |
|---|---|---|
| Cert scope | Does machining fall inside the certified scope? | Cert excludes machining or expired |
| Volume proof | 500K/month under one QMS? | No single-system capacity evidence |
| Traceability | Lot ID on part and record? | Manual, easily lost paper trail |
| OEM reference | Named global customers? | Only vague 'we supply many brands' |
LusterControl is a verifiable Dongguan source factory: founded 2015, 60+ CNC machines across 4,000 m², 500K parts a month, and proven OEM supply to De'Longhi, Donlim, and Breville, plus a UAV customer's first order of ¥1.2M and annual output above ¥20M. Those are the facts a global OEM buyer weighs against the brochure.
Our company overview and supplier-audit guide lay out the exact document set a global OEM evaluation expects. Bring them to your next booth conversation.
LusterControl News From the 2026 Floor: 15 Years of CNC Lathe Work
The booth facts that anchored every answer we gave.
Behind every answer at the booth was a concrete fact about the shop. This LusterControl news recap would be hollow without them, so here is the reference sheet we handed buyers — use it as the benchmark when you audit any supplier.
| Capability | LusterControl fact | Why it matters to your audit |
|---|---|---|
| Founded | 2015 — 15 years CNC lathe work | Documented, matured processes |
| Scale | 60+ CNC machines, 4,000 m² floor | One QMS across volume |
| Capacity | 500K parts / month | Repeatability at scale |
| Tolerance | ±0.005 mm geometric | Tight tolerance CNC proven |
| Finish | Ra ≤0.6 µm, 8K Ra 0.2 µm | Mirror finishing controlled |
| Certs | ISO 9001 + ISO 13485, IATF 16949 in progress | Stack matches your program |
| Clients | De'Longhi, Donlim, Breville; UAV first order ¥1.2M | Proven global OEM supply |
| Annual output | ¥20M+ | Stable source factory |
We supply precision parts to brands including De'Longhi, Donlim, and Breville, and a UAV customer's first order reached ¥1.2M — proof that a Dongguan source factory can meet global OEM discipline. Our incoming-material batch traceability and ASTM A967 passivation on stainless are available on request during your audit.
These are the same facts we ask you to demand from every supplier. For more, read the technical blog or the ±0.005 mm tolerance deep-dive.
Company AI part image
Buyer Questions on Quality Certification: ISO 9001, ISO 13485, IATF 16949
Certificates are the most cited and most misunderstood booth topic.
No 2026 booth conversation ended without a certification question. Buyers wanted to know what each certificate actually proves and — more importantly — what it does not. The honest framing we gave: ISO 9001 is the floor, ISO 13485 is the medical ceiling, IATF 16949 is the automotive gate, and ASTM A967 is the stainless corrosion-control proof.
| Certification | What it adds beyond ISO 9001 | Verify by |
|---|---|---|
| ISO 13485 | QMS specific to medical devices — traceability, risk files, controlled environment | Valid cert + scope covers your device class |
| IATF 16949 | Automotive QMS — PPAP, layered audit, supplier escalation (LusterControl: in progress) | Current cert or signed roadmap letter |
| ASTM A967 | Spec for passivation of stainless — proves corrosion-resistant finish control | Passivation cert per lot on stainless parts |
| ISO 9001 | Baseline QMS — documented, repeatable process | Valid scope + audit date |
- Ask for the certificate number and issue/expiry date; cross-check the issuer is accredited.
- Ask which of your part numbers actually falls inside the certified scope.
- For stainless, request ASTM A967 passivation cert per incoming lot, not per year.
- If IATF 16949 is 'in progress,' get the project timeline and interim PPAP capability in writing.
ASTM A967 passivation for stainless — the question buyers forget
Passivation is the step that removes free iron from the stainless surface so the part resists rust in the field. Buyers specify the alloy but forget to ask for the ASTM A967 cert per lot. On a coffee-machine brew chamber or a medical instrument that cert is the difference between a part that lasts and a warranty claim. LusterControl issues it per lot, on the same quality record as the dimensional FAI.
The rule we gave at the booth: a certificate that expired last month or excludes machining is worthless to you. Check the scope statement, not the logo.
CNC Precision Machining Capacity: 60+ Machines, 500K Parts a Month
Volume questions decide whether a pilot becomes a program.
The capacity buyer questions in 2026 were about one thing: 'can you scale from my prototype to my production without a second supplier?' A source factory running 60+ CNC machines and 500K parts a month under one QMS answers that with a single quality record — the prototype and the millionth part share the same process control.
| Your program | What to verify | Why it protects you |
|---|---|---|
| Prototype only | FAI on pilot lot, program control | Confirms the process before you commit |
| Small-batch custom | Swiss-type + turn-mill flexibility | Mixed parts without re-quoting chaos |
| Mass production | 500K/month under one QMS | Repeatability at scale, one cert stack |
| Mixed volume | Single system, both modes | No second supplier, no second audit |
Small-batch custom vs mass production — you should not choose
A mature CNC precision machining shop runs both from the same floor. You should not have to pick a prototype shop and a production shop and then manage two quality systems. LusterControl's 60+ machines cover turn-mill, 5-axis, and Swiss-type, so a part can start as a custom batch and scale to volume without leaving the system that qualified it.
Pros
- One QMS across prototype and volume — single audit, single cert stack
- Flexibility to scale a custom batch into mass production without re-qualification
- Batch-level traceability follows the part from first article to millionth
Cons
- Very low annual volumes may not justify a full PPAP package — discuss interim controls
- Extreme exotic alloys may need confirmed heat-treat/grind sub-suppliers — verify scope
For the capability map behind this capacity, see the 5-axis and turn-mill guide. The volume proof is the part of the audit that turns a pilot into a program.
Company AI part image
Stainless Steel Mirror Finishing Specs Global OEM Buyers Should Request
Close the loop: the spec sheet that protects your program.
The final theme in our 2026 buyer questions was practical: 'what exactly should I write on the drawing so I get the finish I need and the cert to prove it?' This is the close of the booth conversation and the open of your incoming inspection. Get the spec right and the audit writes itself.
- Ra value on every contact surface (Ra ≤0.6 µm standard, Ra 0.2 µm 8K where cleanability matters)
- Specify electropolishing + ASTM A967 passivation for stainless fluid/food/medical parts
- Require a passivation cert per incoming lot, not per year
- Name the process (mechanical vs electrolytic) so the supplier cannot substitute silently
- Tie the finish spec to the same quality record as the dimensional FAI
- State the inspection method (profilometer vs visual) so 'mirror' is not subjective
- Confirm the cert scope covers stainless finishing before you release the PO
| If your part is… | Request | Why |
|---|---|---|
| Coffee-machine brew chamber | Ra 0.2 µm + ASTM A967 per lot | Cleanability + corrosion resistance |
| Medical instrument | ISO 13485 + electropolish + passivation | Regulatory traceability |
| Decorative trim | Ra ≤0.6 µm mechanical | Look without overspec cost |
| Fluid-control valve | Mirror seal face + passivation | Leak-tight sealing surface |
Bring this checklist to the next booth. The suppliers who answer it without friction are the ones worth the flight. LusterControl's inquiry page is where you send the drawing once you have the spec — we will return an FAI and the cert stack this guide says to demand.
Company AI part image
Company AI part image
Company AI part image
Company AI part image
FAQ: LusterControl news & Company Buyer Questions
A: Ask for proof before price: which process runs my part and can I see it on the floor, show me a First Article Inspection report (not just a certificate of conformance), what is your Ra on contact surfaces, and what is your cert scope and expiry. These buyer questions screen out shops that lead with a number and dodge the document.
A: Ask for an FAI report with measured values against your drawing on a pilot lot, and confirm the process (turn-mill, 5-axis, or Swiss-type) actually exists on the shop floor. Also check gauge and CMM calibration logs. A tolerance promised on a subcontracted process you cannot see is a tolerance you cannot trace.
A: You need 8K (Ra 0.2 µm) when the surface contacts fluid, food, or a sealing face, or where cleanability is a compliance requirement. You do not need it on a hidden bracket — paying for 8K there is overspec. For stainless fluid or medical parts, pair the finish with ASTM A967 passivation per lot.
A: Demand ISO 9001 as the baseline, ISO 13485 for medical programs, an IATF 16949 roadmap for automotive, and ASTM A967 passivation per lot for stainless. Verify each certificate's scope and expiry, plus incoming-material batch traceability. LusterControl holds ISO 9001 and ISO 13485, with IATF 16949 in progress, and supplies De'Longhi, Donlim, and Breville.
A: A mature CNC precision machining shop should. Look for one QMS across 60+ machines running turn-mill, 5-axis, and Swiss-type, shipping 500K parts a month, so your prototype and production share one quality record and one cert stack. That removes the need for a second supplier and a second audit.
A: Because 'mirror' is subjective and unenforceable at incoming inspection. Writing the Ra value (Ra ≤0.6 µm standard, Ra 0.2 µm 8K where needed) plus an ASTM A967 passivation cert per lot gives you a paper basis to accept or reject the part. Global OEM buyers specify both so the finish is measurable, not a feeling.
Send us your drawing for a free DFM review — we will return a First Article Inspection report and the cert stack this 2026 recap says every buyer should demand, from a Dongguan source factory with 15 years of CNC lathe work and ISO 9001 / ISO 13485 behind it.
Request a Free CNC Quote