LusterControl Expands Timing Pulleys for Fluid Control & Valve (2026)
If you buy timing pulleys for fluid control and valve systems, you already know the failure is rarely dramatic. A valve actuator that creeps a half degree off its set point, a flow-meter rotor that drifts after three months of duty, a proportional valve that chatters at low flow, each of these traces back to a pulley whose pitch or bore was a few microns off, and nobody noticed until the field complaint landed. In flow control, a timing pulley is not a commodity drive element, it is the gear that sets how accurately your valve opens and closes, and most buyers spec it like a catalog part anyway.
This guide is written for the valve engineer, procurement lead, or automation integrator who has to select a supplier, read a tooth-profile drawing, and defend the choice to a quality manager. We walk through what actually decides pulley performance in fluid control duty, the hard numbers that separate a passing lot from a scrap lot, and a sourcing checklist you can use the same day. LusterControl has just expanded capacity for fluid control and valve timing pulleys on our 60-machine CNC floor in Dongguan, and we are sharing the buyer-side logic we use internally.
Everything below is grounded in real, verifiable facts, our plant, our tolerances, our certifications, and the programs we have shipped. No inflated capacity numbers, no borrowed case studies, just the criteria you should apply to any shop, including ours.
Table of Contents
- 1. Why Timing Pulleys Demand Tight Tolerance CNC in 2026
- 2. How CNC Precision Machining Shapes Timing Pulleys
- 3. Timing Pulleys Specs: Tight Tolerance CNC and Mirror Finish
- 4. Fluid Control and Valve CNC Parts: Timing Pulleys vs Sprockets
- 5. Custom CNC Parts for Fluid Control Valve Actuators
- 6. Tight Tolerance CNC: +/-0.005 mm for Timing Pulleys
- 7. How to Verify a Supplier's CNC Precision Machining for Pulleys
- 8. Custom CNC Parts Sourcing Checklist for Fluid Control Buyers
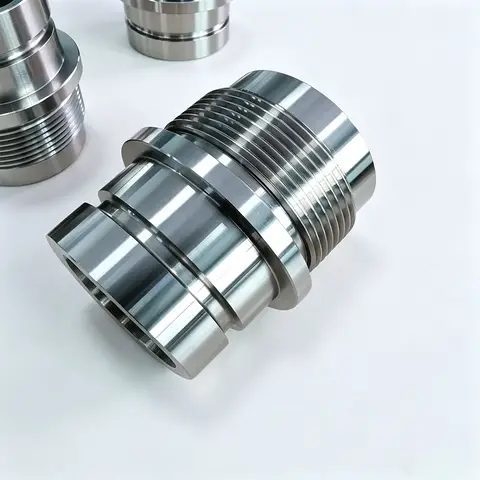
Fluid Control&Valve CNC precision component
Why Timing Pulleys Demand Tight Tolerance CNC in 2026
Bore runout and pitch accuracy, not raw hardness, decide whether a valve pulley holds its set point.
A timing pulley in a fluid control and valve assembly is a precision indexing element. It drives a valve actuator cam, a flow-meter rotor, or a proportional spool, and it must repeat its angular position within microns over hundreds of thousands of cycles. In metering, dosing, and pressure-regulation loops, a pulley that is off by 20 microns on pitch or bore is not 'close enough', it is a flow error, a leak path, or a noisy control loop that your PID tuner will fight forever. For a buyer, the lesson is simple: the pulley's bore-concentricity and pitch tolerance are process specs, not cosmetic details.
Three terms every fluid-control buyer should read first
- Timing pulleys
- Toothed drive elements that transmit motion with fixed pitch; in valve systems they set the exact angular position of an actuator or rotor.
- Bore concentricity (runout)
- How far the bore axis deviates from the pulley's rotation axis; the single number that predicts seal wear and set-point drift.
- Pitch accuracy
- The cumulative error across the toothed band; it decides whether the belt or GT2 mesh tracks without backlash or tooth jump.
At LusterControl we hold a standard mirror finish of Ra 0.6 um and can reach an 8K mirror of Ra 0.2 um on stainless pulley sealing faces. For fluid control parts where a face sits against a seal or a bearing, that 0.2 um finish is what prevents micro-leakage paths and keeps the bore-to-face relationship stable. You should ask every supplier for the actual bore runout and pitch tolerance they can lock in, not the number on their brochure.
Why 2026 is the year to re-check your pulley supply base
Smart valves, battery-energy-storage cooling loops, and semiconductor-grade fluid handling are pulling precise actuation out of the lab and onto volume lines. That shifts the buyer's problem from 'can anyone cut a pulley' to 'can a shop cut fifty thousand that all mesh the same on day 30.' In 2026, repeatability and scale matter more than a hero prototype. Our own expansion, 60 CNC machines across a 4,000 sqm Dongguan plant after our 2026 capacity build-out, is a direct response to that shift toward volume fluid control and valve cnc parts.
Fluid Control&Valve CNC precision component
How CNC Precision Machining Shapes Timing Pulleys
The path from bar stock to a clean-meshing pulley is three process steps, each guarding a different failure mode.
CNC precision machining is what lets us hold both the tooth profile and the bore-to-face relationship on the same part. A pulley may need a GT2 pitch held to a tight band and a bore runout of +/-0.005 mm, two requirements that fight each other unless the process is staged. Here is the sequence we run for fluid-control-grade work, and why each stage exists.
Step 1: 5-axis and turn-mill roughing
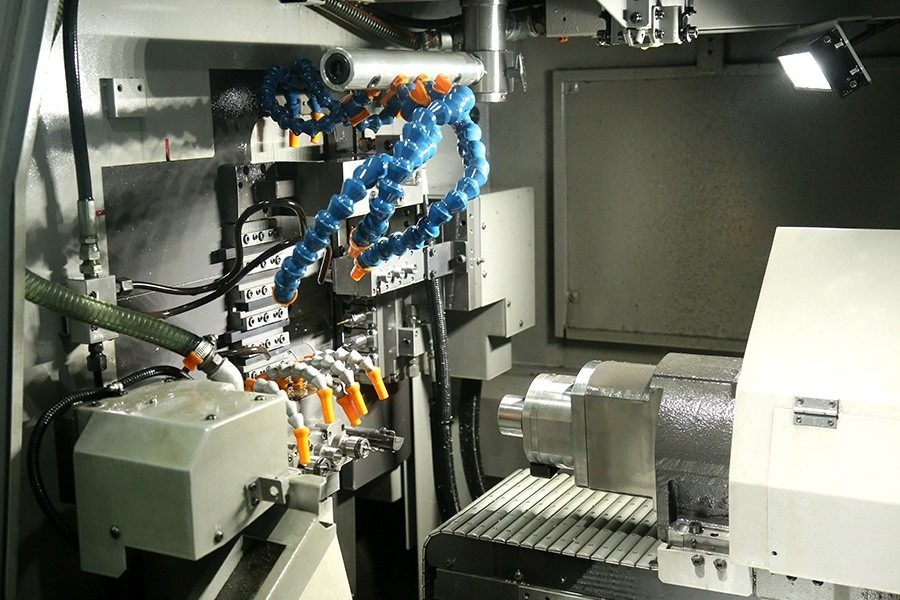
We start on 5-axis machining centers and turn-mill composite units to cut the body, hub, and bore in one setup. Single-setup machining removes the stack-up error you get from re-fixturing, the quiet enemy of tight tolerance CNC work. For thin-web pulleys, Swiss-type turning keeps deflection under control so the web does not bell and throw the teeth off pitch.
Step 2: Tooth profile and bore finishing
We then cut or hob the toothed band to print pitch and finish the bore in the same chucking. A burr on a tooth root is a guaranteed mesh-gall site in a valve drive, and untreated stress warps the web after you measure it. Our medical and semiconductor programs already run batch-level material traceability, so the same discipline carries into pulleys: you can tie a finished pulley back to its incoming lot.
Step 3: Mirror finishing and passivation
- Machine the tooth profile and bore to print tolerance, leaving a controlled stock allowance for finishing.
- Run mirror finishing or electropolishing to reach Ra 0.2 um on sealing and bearing faces.
- Verify bore runout and pitch on CMM and gear-profiling, not by eye.
- Passivate stainless per ASTM A967 so the pulley resists corrosion in valve service.
Timing Pulleys Specs: Tight Tolerance CNC and Mirror Finish
Read these five numbers before you approve any pulley drawing release.
When you compare quotes for timing pulleys, the spec sheet should read like a contract, not a wish list. Below is the real capability table we publish for fluid-control-grade work, with the 'why it matters' column a buyer actually needs. Use it as a template when you ask a supplier what they can lock in.
| Spec | LusterControl capability | Why it matters to your valve system |
|---|---|---|
| Bore runout (concentricity) | +/-0.005 mm | Keeps the pulley centered so seals and set points stay stable. |
| Sealing-face roughness | Ra 0.6 um std, Ra 0.2 um (8K) max | Lower micro-leakage risk on faces that touch seals. |
| Tooth pitch accuracy | Per GT2/HTD profile, +/-band | Prevents backlash, tooth jump, and mesh chatter. |
| Material traceability | Incoming lot tracked per batch | Lets you recall or re-verify a field failure to source stock. |
| Passivation | ASTM A967 on stainless | Protects the pulley from corrosion in fluid service. |
Notice we did not list a tolerance we cannot hold every day. Tight tolerance CNC only helps you if the shop can repeat it across the lot, not just on the first-article part. Our ISO 9001 system and completed ISO 13485 program are what let us promise repeatability, and IATF 16949 is in application to extend that discipline into automotive-grade fluid-control supply.
Fluid Control&Valve CNC precision component
Fluid Control and Valve CNC Parts: Timing Pulleys vs Sprockets
Not every valve drive needs a timing pulley; here is how to decide between the two.
Buyers often conflate two purchases: timing pulleys, a synchronous toothed element that transmits motion with fixed pitch and no slip, and roller-chain sprockets, an asynchronous element for higher torque at the cost of backlash. The table below separates them on the metrics that change your valve accuracy, life, and cost.
| Factor | Timing pulleys (synchronous) | Roller-chain sprockets |
|---|---|---|
| Motion precision | Zero backlash, fixed pitch | Chain stretch introduces drift |
| Best when | Metering, dosing, set-point control | High torque, dirty environments |
| Sealing compatibility | Closed belt, fewer leak points | Lubricated chain, more maintenance |
| Wear / drift | Bore runout if un-finished | Chain elongation over time |
| LusterControl fit | Ra 0.2 um face, +/-0.005 mm | Tolerance +/-0.005 mm bodies |
| Unit cost | Lower for precision small parts | Higher, includes chain kit |
Pros
- Choose timing pulleys if your valve needs fixed, slip-free position, such as metering or proportional control.
- Choose sprockets if torque dominates and a small position drift is acceptable in the loop.
Cons
- Do not buy timing pulleys if your drive needs high torque beyond a belt's rating.
- Do not buy sprockets if your loop demands zero-backlash set-point accuracy.
Either way, the underlying CNC precision machining is the same discipline. The question is only which drive principle fits your valve, and that should follow from your duty cycle, not from a catalog photo.
Custom CNC Parts for Fluid Control Valve Actuators
Material and process choice set the ceiling on both seal life and corrosion resistance.
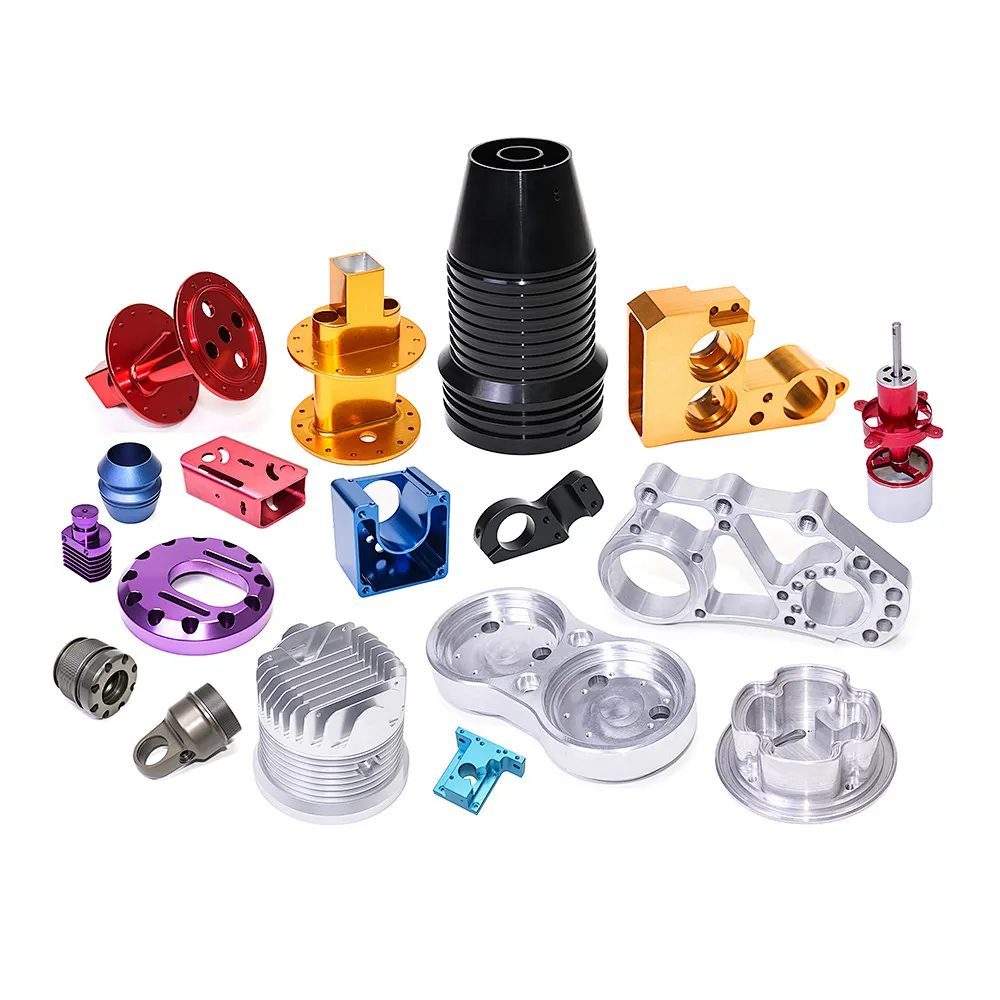
Timing pulleys for fluid control are rarely made from a single magic alloy. The right material depends on whether you need corrosion resistance, non-magnetic behavior, or clean fluid compatibility. As a source factory doing both small-batch custom CNC parts and volume runs, we see the same materials recur across valve programs.
- 303 / 304 stainless
- Easy to machine and passivate per ASTM A967; the default for corrosion-resistant pulleys.
- 316L stainless
- Higher corrosion resistance for chemical and seawater valve duty; slightly softer, plan finish carefully.
- Non-magnetic 304 / 316
- Used when the valve has magnetic position sensors a ferromagnetic pulley would disturb.
- Brass / bronze
- Used for low-friction bearing faces in potable-water and instrument valves.
- Pick stainless when the pulley sees the process fluid and you need ASTM A967 passivation.
- Pick non-magnetic grades when your valve uses magnetic position feedback.
- Pick brass or bronze only when bearing friction, not corrosion, is the limit.
- Confirm the shop can mirror-finish your specific alloy before you release the drawing.
Our 4,000 sqm Dongguan plant and 60 CNC machines let us run these materials from prototype through monthly volume of up to 500,000 pieces, so a custom CNC parts program can scale without re-qualifying a second shop. You can see the full process scope on our company page and recent programs on our blog.
Fluid Control&Valve CNC precision component
Tight Tolerance CNC: +/-0.005 mm for Timing Pulleys
Tolerance and finish are not the same decision; match each to where the part actually fails.
A common buyer mistake is demanding +/-0.005 mm everywhere and Ra 0.2 um everywhere. That doubles cost with no benefit, because only the bore, sealing face, and pitch actually decide valve accuracy. The smarter move is to tier your spec: tight tolerance CNC on the bore and pitch, mirror finish on the sealing face, and commercial tolerances on the outer web and hub.
| Feature on the pulley | Recommended spec | Reason |
|---|---|---|
| Bore and runout | +/-0.005 mm, Ra 0.4 um | Concentricity drives set-point drift; finish is secondary. |
| Sealing face | Ra 0.2 um, +/-0.02 mm | Micro-leakage dominates; position is forgiving. |
| Tooth pitch band | Per profile, +/-band | Mesh tracking prevents backlash and chatter. |
| Outer web and hub | +/-0.05 mm, Ra 1.6 um | Pure structure; no sealing role. |
Pros
- Tiering cuts cost by not over-specifying polish on structural faces.
- Targets the spec where valves actually drift, improving first-pass yield.
- Makes the drawing a clearer contract for any shop you quote.
Cons
- Requires you to decide which features are critical versus structural up front.
- A supplier without gear-profiling gear may push back on the pitch band.
If a shop cannot measure bore runout and pitch on a CMM or gear profiler, they cannot hold them. Put bore-runout and pitch data in the first-article report, not just a dimensional check. That single requirement filters out most shops that say 'we can do valve-grade' but have never proven the geometry.
How to Verify a Supplier's CNC Precision Machining for Pulleys
Five checks separate shops that can do valve-grade from shops that say they can.
- Ask for a bore-runout (concentricity) report on the actual pulley, not just an outer-diameter check.
- Confirm they run ASTM A967 passivation on stainless pulleys for valve service.
- Request incoming-lot material traceability, not just a CoC PDF.
- Verify they have 5-axis or turn-mill composite to hold tight tolerance CNC in one setup.
- Check certifications: ISO 9001 at minimum, ISO 13485 or IATF 16949 as a plus for medical or auto.
- Run a paid first-article batch and cycle-test the actuator before committing volume.
These checks sound basic, yet most valve-drift incidents we are asked to rescue trace back to one of them being skipped. A shop that publishes its Ra and runout capability and cert status up front, like we do, is simply easier to qualify. You can review our credentials and facility on the about page before sending a drawing.
Fluid Control&Valve CNC precision component
Custom CNC Parts Sourcing Checklist for Fluid Control Buyers
Use this as your RFQ attachment so every quote answers the same questions.
- State which features are critical versus structural, and tier the Ra and tolerance per feature.
- Require bore-runout and pitch data in the first-article report, not a CMM-only check.
- Specify ASTM A967 passivation for any stainless pulley touching the process fluid.
- Demand incoming-lot traceability so field failures are traceable to source stock.
- Ask for real repeatability evidence, SPC or CPK, on prior pulley lots.
- Confirm scale: can the shop go from prototype to 500,000 pieces a month without re-qualification?
LusterControl's expansion for fluid control and valve clients is built around exactly this buyer logic: one plant, one quality system, prototype-to-volume on 60 CNC machines, with mirror finishing and passivation done in house. If your drawing is ready, the fastest next step is a design-for-manufacturing review where we flag bore-runout and pitch conflicts before you cut metal. See our inquiry page to start.
Fluid Control&Valve CNC precision component
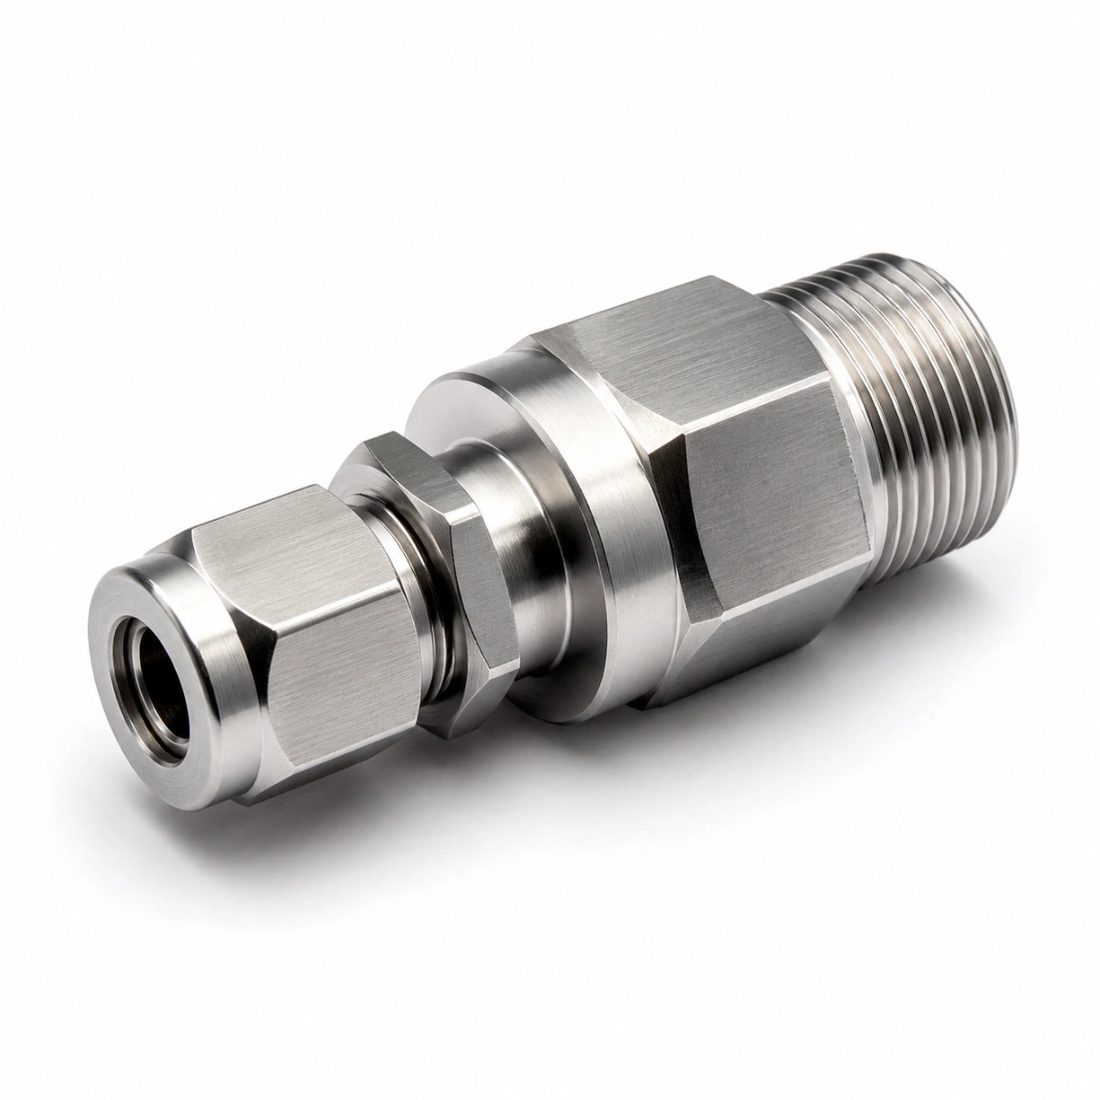
Fluid Control&Valve CNC precision component
Fluid Control&Valve CNC precision component
Fluid Control&Valve CNC precision component
FAQ: timing pulleys & Fluid Control&Valve Buyer Questions
A: Bore concentricity should target +/-0.005 mm so the pulley stays centered and the valve holds its set point without drift. LusterControl holds +/-0.005 mm bore runout using 5-axis and turn-mill composite machining in a single setup.
A: The sealing or bearing face should target Ra 0.2 um, 8K mirror, to avoid micro-leakage paths in valve service. Structural faces need only Ra 1.6 um. LusterControl holds Ra 0.6 um standard and Ra 0.2 um mirror on request.
A: Yes. Stainless timing pulleys are passivated per ASTM A967 to resist corrosion in fluid control and valve service. Passivation is specified on the drawing and verified, not assumed.
A: Yes. Our Dongguan plant runs 60 CNC machines in 4,000 sqm with monthly capacity up to 500,000 pieces, under one ISO 9001 and ISO 13485 quality system. The same line that makes your first article makes your volume.
A: Yes, confidentiality is routine, not a special request. We run NDA programs for global brands such as De'Longhi, Donlim, and Breville, with controlled CAD access and discreet packaging on prototype shipments.
A: LusterControl is ISO 9001 certified and ISO 13485 completed, with IATF 16949 in application. Founded in 2015, we bring 15 years of CNC stainless mirror machining to fluid control and valve programs.
Send us your drawing for a free DFM review, we will flag bore-runout and pitch conflicts before you cut metal, and quote prototype-to-volume on one quality system. Start at https://www.lustercontrol.com/sendinquiry.htm
Request a Free CNC Quote