O-Ring Seal vs Metal-Face Seal: Choosing Liquid-Cooling Couplers (2026)
If you specify liquid cooling for a rack, a cold plate or a coolant distribution unit, you already know the uncomfortable part: the loop rarely fails at the pump. It fails at the joint. A coupler that weeps a few microlitres after a thermal cycle, or a seal seat that scores on the tenth mate, can take an expensive assembly out of service. Yet in 2026 most sourcing teams still choose between an O-ring seal and a metal-face seal on habit rather than on the physics of their application.
This guide is written for the thermal-design engineer and the buyer who has to defend that choice. We compare the two sealing approaches on the things that actually decide field performance — achievable leak rate, required surface finish, temperature and pressure envelope, mate-unmate durability, contaminant sensitivity and cost at volume — using the hard numbers a drawing should carry: a seal seat at Ra ≤ 0.4 µm for demanding programs, an 8K mirror ceiling of Ra 0.2 µm, ±0.005 mm held tolerance, and a documented pressure-hold and leak test. Then we show what liquid-cooling coupler machining must deliver to hold those numbers, and how to vet a supplier before you release a purchase order.
The capability cited here is our own, not an industry average: LusterControl (Dongguan Licun Technology) was founded in 2015 and has spent 15 years in CNC precision machining with a focus on stainless-steel mirror finishing. We run 60 CNC machines in a 4,000 m² plant (2026 expansion; the former 2,000 m² figure is obsolete), hold ±0.005 mm in production, ship up to 500,000 parts per month, and operate under ISO 9001 certification with an ISO 13485 quality system established (certification advancing) and an IATF 16949 application in progress. We compare technologies, not competitors; every recommendation below is a sourcing decision you can verify with data.
Table of Contents
- 1. Why Liquid Cooling Couplers and Seals Decide Rack Reliability in 2026
- 2. How a Metal-Face Seal Works: The Cone, the Contact Band and the Preload
- 3. O-Ring Seal vs Metal-Face Seal: 7 Engineering Factors Compared
- 4. Liquid-Cooling Coupler Machining: What the Seal Seat Really Demands
- 5. Stainless Steel Mirror Finishing (Seal Cone) to Ra 0.2 µm and Beyond
- 6. Tight Tolerance CNC: Holding Cone Angle, Concentricity and Burr-Free Edges
- 7. Which Liquid Cooling Couplers and Seals Fit Your Loop? Decision Table
- 8. Quality Framework Behind Liquid-Cooling Coupler Machining: First Article to Lot Traceability
- 9. Common Mistakes in Liquid-Cooling Coupler Machining (and How to Avoid Them)
- 10. Buyer's Checklist: Vetting a CNC Precision Machining Partner for Seal Parts
- 11. Why LusterControl's CNC Precision Machining Fits Liquid-Cooling Seal Programs
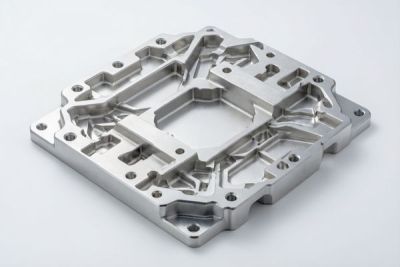
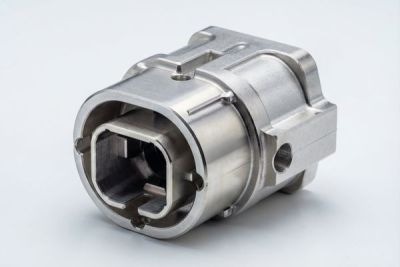
Liquid Cooling (Coupler Seal) CNC precision component
Why Liquid Cooling Couplers and Seals Decide Rack Reliability in 2026
The smallest interface in the loop is the one you will inspect first when something goes wrong.
As rack densities climb through 2026, direct-to-chip and rear-door liquid cooling have moved from pilot to default in new compute halls. Every loop needs a way to connect and disconnect without spilling fluid onto live electronics, and that job falls to liquid cooling couplers and seals. The coupler is simultaneously a fluidic joint, a mechanical locator and often an electrical or sensing interface. Its seal must survive pressure, temperature cycling, vibration and repeated mate-unmate cycles while staying dry.
The commercial risk is easy to underestimate. A coupler is a low-unit-cost item, but a leak discovered after integration can mean a drained loop, a removed board, a re-test of the whole rack and a schedule slip measured in weeks. That asymmetry — a cheap part, an expensive failure — is why the seal architecture deserves a decision of its own rather than a line in a bill of materials. When you source liquid cooling couplers and seals, you are really choosing a failure mode.
- O-ring seal
- A circular elastomer ring seated in a machined groove, compressed between two surfaces to block a leak path; the seal is the elastomer, and the machined groove and land control its compression.
- Metal-face seal
- A seal in which two lapped metal surfaces — commonly a cone and a matching seat — are pressed together to form the barrier, with no elastomer in the fluid path.
- Seal seat / seal cone
- The machined surface that a seal bears against. For a metal-face design the cone angle, contact band and surface finish are functional features, not cosmetic ones.
- Leak rate
- The quantified fluid loss across a sealed interface under a stated pressure and time, typically verified by pressure-decay or helium testing against an agreed acceptance limit.
Read our broader CNC precision machining technical guides for the process background; this article stays on the single decision in front of you — elastomer or metal face — and on what it takes to manufacture either one repeatably.
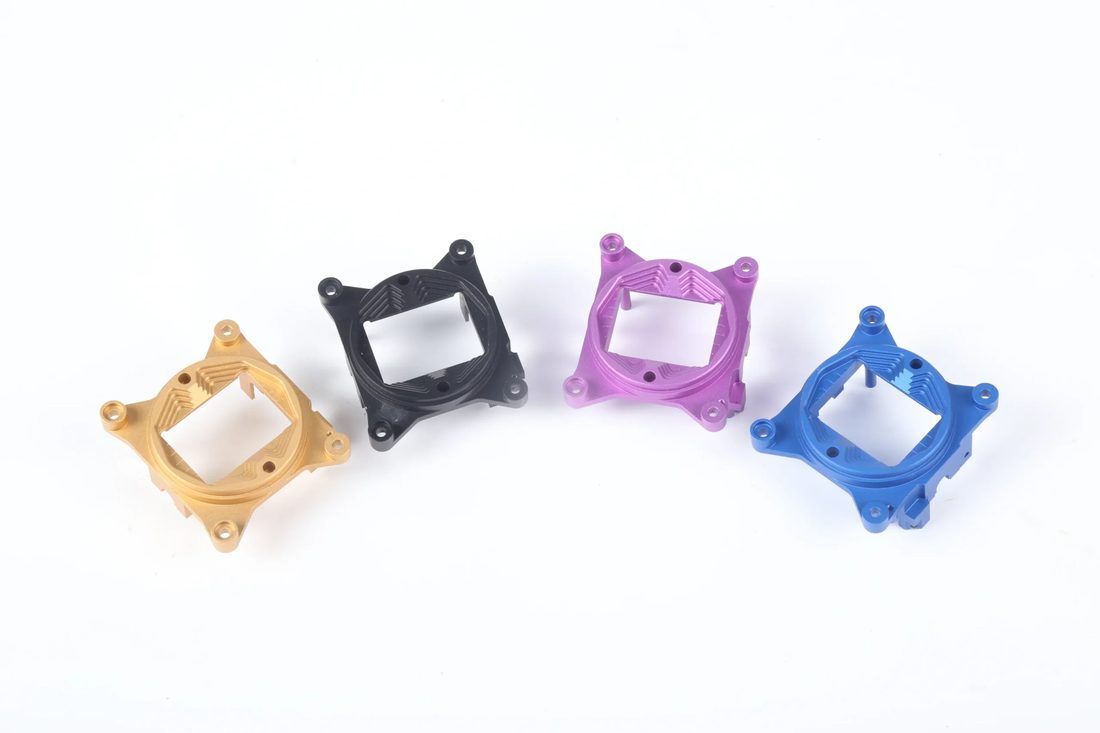
Liquid Cooling (Coupler Seal) CNC precision component
How a Metal-Face Seal Works: The Cone, the Contact Band and the Preload
In a metal-face seal the machining is the seal. There is no soft part to forgive a bad surface.
The sealing geometry
A metal-face seal works by bringing two precisely finished metal surfaces into contact under axial preload. In a typical quick-disconnect liquid coupler one half carries a male cone and the other a female seat; when the coupling is engaged, a spring or cam pushes the cone into the seat until a narrow annular contact band is established. That band — often only a fraction of a millimetre wide — is the barrier. Because no elastomer sits in the fluid path, the design tolerates higher temperature and aggressive coolants better than an O-ring, and it can be cleaned and re-mated with far less sensitivity to swelling or compression set.
Why the cone is a machining problem, not a gasket problem
The consequence is that the sealing performance is created at the machine tool, not at assembly. Three features do nearly all the work: the cone angle, which must match within a small angular tolerance or the contact band shifts off the seat; the roundness and concentricity of the cone relative to the flow bore, which determines whether contact pressure is uniform around the circumference; and the surface finish of the contact band, which controls whether the two asperity fields can actually close the leak path. A cone that looks polished to the eye can still leak if its angle is a fraction of a degree off or if the finish is measured on the wrong face.
- Geometry: matched cone and seat angles, typically specified to a tight angular tolerance with a defined contact-band location.
- Surface: a low-Ra, often mirror-grade finish on the sealing surface itself — demanding programs in liquid cooling specify Ra ≤ 0.4 µm on the seal seat, with higher mirror grades reaching 8K Ra 0.2 µm.
- Form: roundness and bore-to-seat concentricity that keep the contact band continuous; this is where setup count matters more than spindle speed.
For the buyer, the practical point is that a metal-face seal moves quality upstream. You cannot inspect leak performance into a cone after the fact; you have to machine the geometry and finish correctly the first time, then verify them. That is why the supplier's process route — not just its price — belongs in the RFQ.
O-Ring Seal vs Metal-Face Seal: 7 Engineering Factors Compared
Both designs can seal water-glycol. The difference is what each one asks you to accept elsewhere.
There is no universal winner between an O-ring seal and a metal-face seal. There is a correct choice for your temperature, pressure, coolant chemistry, mate-cycle count and cleanliness requirement. The table below gives the comparison a specifier can actually defend, using the numbers a drawing should state rather than generalities. Treat the figures as typical engineering targets to agree with your supplier, not as blanket guarantees for every application.
| Factor | O-ring seal | Metal-face seal |
|---|---|---|
| Sealing element | Elastomer ring (e.g. FKM, EPDM) in a machined groove | Two lapped metal surfaces — cone and seat — under preload |
| Typical leak target | Low, but dependent on compression and elastomer condition | Very low when cone angle, form and finish are controlled; demanding programs specify ≤0.01 mL/min at 10 bar hold |
| Seat finish demand | Groove and land finish matter; Ra around 0.8–1.6 µm often adequate | Seal cone is the critical face; Ra ≤ 0.4 µm typical for demanding service, up to 8K mirror Ra 0.2 µm |
| Temperature envelope | Limited by elastomer; swelling and compression set at high temperature | Limited mainly by metal and fluid; no elastomer in the path |
| Mate-unmate cycles | Ring can be damaged or rolled; replacement may be needed | Designed for repeated mating; wear concentrated on a hard contact band |
| Contamination sensitivity | Tolerant of some debris, but debris can cut the ring | A particle on the contact band can break the seal; cleanliness and capping matter |
| Cost at volume | Low part cost, simple seat machining | Higher machining and inspection cost, offset by durability in demanding loops |
- 1. Leak performance. If your acceptance criterion is a documented pressure-hold and leak rate rather than a visual dry check, a metal-face seal gives a more repeatable barrier — provided the cone is machined and verified to the specified finish.
- 2. Temperature and chemistry. Above the practical range of elastomers, or with coolant additives that swell rubber, the metal-face seal removes the weakest material from the equation.
- 3. Mate cycles. Quick-disconnect couplers that are connected and disconnected on the bench repeatedly favour a metal face; the elastomer in an O-ring design is the consumable.
- 4. Surface requirement. An O-ring tolerates a more modest land finish; a metal-face seal demands a controlled low-Ra cone. Be honest about whether your supplier can measure that finish on the actual sealing face.
- 5. Cleanliness. Metal faces are unforgiving of a stray particle on the contact band. Specify deburring, flushing and capped shipment for either design, and more strictly for the metal face.
- 6. Cost. At low volumes the O-ring is usually cheaper. At lifecycle level, including downtime and re-mate behaviour, the comparison can reverse.
- 7. Serviceability. If field replacement of the seal is part of the maintenance concept, an O-ring is easier to replace; a metal-face coupler is usually replaced as an assembly.

Liquid Cooling (Coupler Seal) CNC precision component
Liquid-Cooling Coupler Machining: What the Seal Seat Really Demands
Concentricity is not inspected into a part. It is set by how the part is held.
Liquid-cooling coupler machining is a setup-count problem before it is a cutting problem. A coupler body carries a sealing cone or O-ring land, a flow bore, a thread or locking feature, and datum faces — all with a positional relationship to one another. If the cone and bore are cut in different fixtures, every transfer adds a datum shift, and the contact band or O-ring compression drifts around the circumference. The result is a part that passes a dimensional check yet weeps under pressure.
One clamping, one datum frame
Turn-mill composite — turning and live-tool milling on one platform without moving the part between machines — is the most direct way to protect that relationship. The blank is clamped once; the spindle turns the cone and sealing land, live tooling cuts flats and ports, and the bore is finished in the same coordinate system. For smaller couplers and manifold inserts, Swiss-type turning adds the same discipline at a reduced diameter. On our floor these cells sit alongside 5-axis capability, so the process route can be chosen by geometry rather than by convenience.
| Factor | Turn-mill / Swiss-type in one setup | Split lathe → mill → drill routing |
|---|---|---|
| Bore-to-seat concentricity | Held by a single datum frame; ±0.005 mm capability | Limited by re-clamping and datum transfer |
| Cone angle consistency | Program-controlled, one tool reference | Depends on fixture repeatability between operations |
| Setup count | One primary clamping | Two to three handoffs |
| First-article repeatability | Program-driven and repeatable | Operator-dependent alignment |
| Best fit | Sealing couplers, manifold inserts, ported bodies | Simple fittings with loose concentricity |
Ask a supplier which single setup holds your critical relationship. If the answer involves three machines and an inspection guess, the quote is hiding a risk. More of our process-selection reasoning is covered in the technical guides section.
Stainless Steel Mirror Finishing (Seal Cone) to Ra 0.2 µm and Beyond
A mirror finish on a seal cone is a measured requirement, not a decorative choice.
Stainless steel mirror finishing (seal cone) work is where a metal-face design succeeds or fails. On a sealing cone the surface roughness determines whether two metal asperity fields can close the leak path under preload. A finish specified loosely — 'polished', 'bright', 'mirror' — is not a requirement, because it has no measurement location, method or limit. A usable specification names the Ra target, the face to be measured, and the instrument or comparison standard.
| Finish level | Ra target | Where it is used in a liquid-cooling coupler |
|---|---|---|
| Standard mirror | Ra ≤ 0.6 µm | General wetted surfaces and external appearance where sealing is not critical |
| Demanding seal seat | Ra ≤ 0.4 µm | Seal seat and cone in higher-spec liquid-cooling programs |
| 8K mirror | Ra 0.2 µm | Highest mirror grade we produce, for the most demanding sealing faces |
| Non-sealing machined land | Per drawing, often coarser | Threads, flats and datum faces where finish does not govern leakage |
Passivation and cleanliness after finishing
Mirror finishing removes material and can leave embedded media or a disturbed surface layer. For stainless wetted parts we reference ASTM A967 for chemical passivation treatments in our documentation, then clean, flush and cap parts destined for a sealed loop. Naming the standard on the purchase order replaces a vague phrase like 'stainless finish' with a verifiable criterion — a detail that matters when coolant chemistry and long service life are involved.
- Ra
- Arithmetic mean surface roughness, in micrometres (µm). A lower Ra indicates a smoother surface; on a seal cone it correlates with the ability to close a leak path.
- 8K mirror
- A high-grade mirror finish corresponding to Ra 0.2 µm, the ceiling of our mirror-finishing capability.
- Passivation (ASTM A967)
- A chemical treatment that removes free iron from a stainless surface and enhances corrosion resistance, specified by standard rather than by description.

Liquid Cooling (Coupler Seal) CNC precision component
Tight Tolerance CNC: Holding Cone Angle, Concentricity and Burr-Free Edges
A tolerance is only as credible as the inspection behind it.
Tight tolerance CNC is easy to claim and expensive to prove. On a coupler, the features that govern sealing are few but demanding: the cone angle and contact-band position, the bore diameter and its concentricity to the seat, the mating-face flatness, and the absence of burrs at any edge that touches the seal. Our production tolerance of ±0.005 mm is a shop-floor number, held on the same cells that run appliance and medical programs — not a laboratory result quoted from a brochure.
| Critical feature | Why it is critical | Verification method |
|---|---|---|
| Cone angle / seat geometry | Sets the location and width of the contact band | Profile/CMM against the agreed datum scheme |
| Seat finish (Ra) | Controls whether the leak path closes | Surface-roughness trace taken on the sealing face |
| Bore-to-seat concentricity | Uneven contact causes weeping | CMM with shared datums |
| Mating-face flatness | Preload distribution around the joint | Flatness check on the datum face |
| Edge condition | A burr can cut an O-ring or lift a metal seat | Deburr verification under magnification |
- Concentricity
- The degree to which two features share a common axis; on a coupler, bore-to-seat concentricity keeps seal compression or metal contact uniform.
- Burr
- A small raised edge left by machining; on a sealing part it can cut an elastomer or prevent full metal-to-metal contact.
- CPK
- A process-capability index used in statistical process control to show how consistently a process holds a specification.
The lesson for a buyer is to tie every tolerance to a method. A number printed on a drawing with no gauge, no datum and no measurement location is an aspiration. In a well-run program the inspection plan — including how the seal face will be measured — is agreed during DFM, before the first chip is cut.
Which Liquid Cooling Couplers and Seals Fit Your Loop? Decision Table
Use this table to decide in five minutes what your application is actually asking for.
Strip the decision down to the requirements that matter and the choice usually becomes clear. Match your project to the closest row, then use the choose-A / choose-B list to confirm with your thermal and sourcing teams.
| Your requirement | Recommended seal | Why it wins |
|---|---|---|
| High coolant temperature or aggressive additives | Metal-face seal | No elastomer to swell or take compression set |
| Frequent bench mate-unmate cycles | Metal-face seal | Wear concentrated on a hard, re-matable contact band |
| Very low unit cost, moderate duty | O-ring seal | Simple groove machining and low part cost |
| Field-replaceable seal concept | O-ring seal | Elastomer can be replaced without swapping the assembly |
| Controlled-cleanliness loop with capped shipment | Either; metal face preferred | Metal face gives the lowest leak rate when kept clean |
| Vibration plus thermal cycling, long service interval | Metal-face seal | More stable barrier over temperature and time |
Pros
- Choose a metal-face seal if your priority is a documented low leak rate, high temperature capability or repeated mating, and your supplier can machine and measure a Ra ≤ 0.4 µm cone.
- Choose an O-ring seal if you need the lowest unit cost, a field-replaceable element or tolerance of less-than-perfect cleanliness, and your duty cycle is moderate.
- Choose either only after the acceptance test — pressure, dwell time, temperature and leak limit — is written into the drawing.
Cons
- A metal-face seal asks more of machining and inspection; if your supplier cannot show a roughness trace on the cone, the advantage is theoretical.
- An O-ring in a high-temperature or aggressive-coolant loop will eventually show compression set or swelling, whatever its initial leak result.
If your requirement sits between rows, send the drawing and the operating envelope for a DFM review; the right answer depends on the seal seat as much as on the seal.

Liquid Cooling (Coupler Seal) CNC precision component
Quality Framework Behind Liquid-Cooling Coupler Machining: First Article to Lot Traceability
The ramp holds only if the evidence chain was designed before the first chip was cut.
A supplier can cut an excellent first article and still fail at the tenth lot if there is no system tying material, machine and inspection record together. Our quality chain for liquid-cooling coupler machining is the same for a ten-piece prototype and a 500,000-part month, which is what allows it to scale without a separate 'production quality' standard.
- DFM review: seal strategy, cone and datum scheme, tool reach and inspection access agreed before programming.
- Incoming material check: mill certificates verified, batch recorded and stock screened before it enters the cell.
- First-article inspection: critical angles, diameters, concentricity and seal-face geometry measured against the agreed datums.
- Surface verification: roughness trace taken on the functional sealing face, with the measurement location recorded.
- In-process SPC/CPK: special characteristics monitored statistically, not spot-checked at the end of a run.
- Pressure-hold / leak test and final release: agreed method and acceptance limit, followed by deburr, clean, flush, cap where specified, and FQC/OQC release.
For an integrator the value is practical: if a coupler is questioned in the field, a traceable batch record lets you isolate material, machine and inspection history in hours rather than weeks. That difference decides whether a quality notice is contained or becomes a program delay.
Common Mistakes in Liquid-Cooling Coupler Machining (and How to Avoid Them)
Most coupler failures are decided at the drawing stage, long before the pressure test.
- Mistake 1 — ignoring setup count. If the drawing carries a concentricity callout, ask which single setup holds it. A multi-fixture answer is a risk signal.
- Mistake 2 — a finish with no measurement location. Require a roughness trace on the sealing cone, not on an easy-to-reach outer face.
- Mistake 3 — an unqualified leak claim. Define the test method, pressure, time and acceptance limit in the drawing, and ask for the calibration record.
- Mistake 4 — skipping the pilot batch. A first article proves geometry; a pilot batch proves repeatability. Both are needed before volume.
- Mistake 5 — no cleanliness or capping plan. A perfectly machined seat contaminated with cutting debris will fail in the loop.
A supplier who welcomes these questions has usually already solved them. Put each item into the RFQ as a requirement and you remove most of the usual ramp risk before a single part is cut.

Liquid Cooling (Coupler Seal) CNC precision component
Buyer's Checklist: Vetting a CNC Precision Machining Partner for Seal Parts
Five documents tell you more than a polished sample.
Whether you are sourcing liquid cooling couplers and seals or any other sealing component, the supplier's documentation is the honest signal. Use this buyer's checklist as a gate before you award a program. These are the same documents we expect you to ask of us.
- A first-article report with the datum scheme and measured cone or land geometry — not a pass/fail stamp alone.
- A surface-roughness trace taken on the actual sealing face, with the measurement location stated.
- A documented leak-test method, calibration record and acceptance limit for the sealed interface.
- Material certificates and lot-level traceability that can be tied to your specific batch.
- A written process plan naming the route (turn-mill composite, Swiss-type or 5-axis), critical steps and inspection holds.
Red flags worth walking away from
- A quote that ignores the concentricity callout or proposes multiple setups without explaining datum control.
- Finish claims with no trace, or traces taken on a face that does not seal.
- A leak claim with no stated test method, pressure or acceptance limit.
- A process route that changes between sample and production without re-qualification.
- Unwillingness to sign an NDA or to control access to your CAD files.
None of these are exotic demands — they are the minimum file a serious CNC precision machining partner already keeps. Review more of our Dongguan plant and team information before you write the RFQ.
Why LusterControl's CNC Precision Machining Fits Liquid-Cooling Seal Programs
A source factory built for the transition from a difficult sample to a stable, documented volume.
LusterControl (Dongguan Licun Technology) was founded in 2015 and has spent 15 years in CNC precision machining with a focus on stainless-steel mirror finishing. The same plant that reaches 8K mirror Ra 0.2 µm for appliance clients runs the tight tolerance cells that hold a coupler's sealing geometry. Critical operations — turning, milling, finishing and inspection — stay under one quality record rather than being subcontracted away.
| Capability | LusterControl reality | Buyer value in a coupler program |
|---|---|---|
| Equipment | 60 CNC machines (35 lathes, 20 4/5-axis, 5 turn-mill; Swiss-type available) | Parallel cells protect the sample-to-volume schedule |
| Facility | 4,000 m² (2026 expansion; former 2,000 m² obsolete) | Room for dedicated inspection and clean packaging |
| Tolerance | ±0.005 mm held in production | Concentricity and fit confidence on the seal seat |
| Surface | Standard mirror Ra ≤ 0.6 µm; up to 8K Ra 0.2 µm | Low-Ra cones and mating faces |
| Quality | ISO 9001 certified; ISO 13485 quality system established (certification advancing); IATF 16949 application in progress | Auditable system, not ad-hoc QC |
| Traceability | Incoming lot control and batch records | Fast root cause on any field issue |
We serve new-energy vehicles, medical devices, aerospace, smart home, coffee-machine parts, UAVs, semiconductor, robotics, optics, industrial automation, fluid control, energy storage, transmission and tooling programs from our Dongguan source factory. If you are choosing between an O-ring seal and a metal-face seal for a 2026 liquid-cooling design, send us your drawing for a free DFM review — we will return achievable tolerance, seal-finish and leak-test guidance, a process route and a unit-price curve before you commit.
Choose the seal by the physics of your loop, then choose the supplier by the evidence behind the finish.

Liquid Cooling (Coupler Seal) CNC precision component

Liquid Cooling (Coupler Seal) CNC precision component

Liquid Cooling (Coupler Seal) CNC precision component
FAQ: liquid cooling couplers and seals & Liquid Cooling (Coupler Seal) Buyer Questions
A: An O-ring seal uses a compressed elastomer ring in a machined groove; a metal-face seal uses two lapped metal surfaces, typically a cone and seat, pressed together under preload. The O-ring wins on unit cost and field serviceability, while the metal face wins on temperature, repeated mating and achievable leak rate.
A: The sealing face should carry a stated Ra limit and measurement location. Demanding liquid-cooling programs commonly specify Ra ≤ 0.4 µm on the seal seat; our highest mirror grade reaches 8K Ra 0.2 µm. Always require a roughness trace taken on the actual sealing face, not an accessible outer surface.
A: It depends on the seal design and the agreed test. Demanding programs specify a leak rate below 0.01 mL/min at a 10 bar pressure hold, verified by pressure-decay or helium testing. Ask for the pressure, dwell time, temperature and acceptance limit in writing — a number without a method is not a requirement.
A: It cuts the sealing cone or land, bore and milled features in one clamping, so bore-to-seat concentricity is held by a single datum frame rather than by re-fixturing. Split lathe-mill-drill routing introduces datum transfer error at every handoff, which can make a part weep under pressure.
A: Material certificates, first-article inspection data, a roughness trace on the sealing face, in-process SPC/CPK records, a documented leak test and lot-level traceability tying material, machine and inspection together. LusterControl is ISO 9001 certified, with an ISO 13485 quality system established (certification advancing) and an IATF 16949 application in progress.
A: Yes. NDA-backed programs are routine, including De'Longhi, Donlim and Breville-grade work. CAD files are held under controlled access, customer designs are not reused or offered to competing programs, and prototype shipments are packaged discreetly. Send your drawing for a free DFM review to start.
Still choosing between an O-ring seal and a metal-face seal for your 2026 liquid-cooling design? Send LusterControl your coupler drawing for a free DFM review — we will return achievable tolerance, seal-finish and leak-test guidance, a process route and a unit-price curve, backed by 15 years of CNC precision machining.
Request a Free CNC Quote